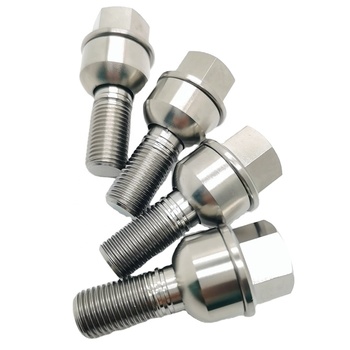
M14 x 1.25 Conical Seat Hub Bolts
Specifically engineered for modern BMW F/G series, Mini Cooper, and Rolls-Royce platforms. Features precision CNC-formed 60-degree taper cones ensuring micro-concentric contact.
Certified Grade 5 (Ti-6Al-4V) wheel hub fasteners engineered for extreme shear resistance, rotational unsprung mass reduction, and zero atmospheric corrosion. Custom CNC manufactured by Yevzo Titanium Metal Co., Ltd.
In modern high-performance automotive engineering, motorsport architectures, and luxury electric vehicle (EV) platforms, wheel hub fastening systems are subjected to severe multiaxial dynamic stress, brake rotor thermal radiation up to 400°C, and aggressive environmental salt-spray corrosion. Titanium hub bolts manufactured from Ti-6Al-4V alloy represent the premier solution to resolve the fundamental trade-off between tensile strength and rotational mass.
Standard automotive wheel assemblies typically rely on Grade 10.9 or 12.9 chromoly steel wheel studs and hub bolts. Steel carries a high density of approximately 7.85 g/cm³. Under high angular velocity, every gram of weight placed at the wheel hub perimeter acts as unsprung, rotational mass. Rotational inertia increases with the square of the radius, meaning that heavy steel hub bolts directly impair suspension response, dampening efficacy, steering crispness, and acceleration throttle dynamics.
Yevzo Titanium Metal Co., Ltd. machines titanium hub bolts exclusively from vacuum-melted, certified Grade 5 titanium (Ti-6Al-4V, Werkstoff 3.7165, UNS R56400). With a nominal density of 4.43 g/cm³, our titanium hub bolts achieve an immediate 43% to 46% mass reduction compared to equivalent carbon steel and alloy steel fasteners without compromising structural clamping integrity.
| Mechanical Metric | Gr5 (Ti-6Al-4V) Hub Bolt | Class 10.9 Steel | Class 12.9 Steel |
|---|---|---|---|
| Nominal Density | 4.43 g/cm³ (Lightweight) | 7.85 g/cm³ | 7.85 g/cm³ |
| Ultimate Tensile Strength | 950 – 1050 MPa | 1000 – 1040 MPa | 1200 – 1220 MPa |
| Yield Strength (0.2% Proof) | 880 – 920 MPa | 900 – 940 MPa | 1080 – 1100 MPa |
| Thermal Conductivity | 6.7 W/(m·K) (Thermal Barrier) | 42.6 W/(m·K) | 42.6 W/(m·K) |
| Modulus of Elasticity (E) | 114 GPa (Superior compliance) | 210 GPa | 210 GPa |
| Salt-Spray Corrosion Resistance | Infinite (Self-passivating TiO₂) | Poor (Rusts when plated layer wears) | High Risk (Hydrogen embrittlement) |
| Rotational Mass Delta | -44.2% Reduction | Baseline (0%) | Baseline (0%) |
Mechanical testing performed in accordance with ASTM E8/E8M tensile protocols and ISO 898-1 standard proof load test parameters on M14x1.5 rolled thread specimens.
Whether you require direct replacements for OEM hub assemblies (Porsche, BMW M, Mercedes-AMG, Audi RS, Ferrari, Lamborghini, Tesla) or extended shank lengths for aftermarket track wheel spacers, Yevzo provides fully customized titanium wheel hub solutions.
Specifically engineered for modern BMW F/G series, Mini Cooper, and Rolls-Royce platforms. Features precision CNC-formed 60-degree taper cones ensuring micro-concentric contact.
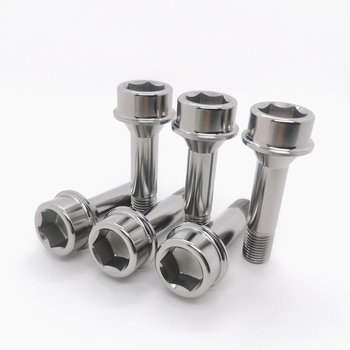
Equipped with an independent Grade 5 two-piece rotating washer seat (R13 Ball / R14 Ball or 60° Taper). Eliminates rotational galling against expensive forged alloy wheels during torque-down.
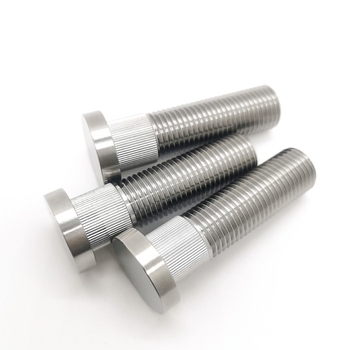
Designed for vintage European track vehicles, track day applications, and custom tuner hubs. Available with custom shank lengths from 28mm to 65mm to fit extended slip-on wheel spacers.
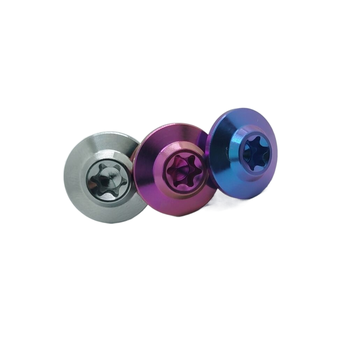
Internal multi-spline and hollow-head security drives providing maximum anti-theft deterrence, enhanced cam-out resistance at high torques, and further weight reduction in the bolt core.
Global automotive supply chains are actively shifting procurement strategies toward ultra-lightweight metals. Inquiries and RFQs across North America and Europe reveal three major procurement trends driving commercial adoption.
Electric vehicles carry heavy lithium battery packs, forcing engineers to eliminate weight from the corner chassis. Titanium hub bolts provide immediate, safe weight reduction on unsprung assemblies, improving WLTP/EPA range efficiency ratings and regenerative braking performance.
Automotive tier-1 buyers increasingly bypass third-party trading intermediaries to establish direct sourcing relationships with primary facilities located inside China’s "Titanium Valley" (Baoji), securing transparent melt lot numbers, chemical spectrograms, and ESG-compliant audit logs.
Aftermarket wheel rim damage caused by high-friction rigid taper bolts is prompting wheel manufacturers to mandate two-piece floating collar designs. This reduces clamping torque scatter, prevents aluminum galling, and maintains consistent tension through repeated wheel changes.
Standard anodized finishes are evolving toward advanced Physical Vapor Deposition (PVD) and Diamond-Like Carbon (DLC) coatings. These nanometer-thick ceramic coatings yield surface hardness exceeding 2500 HV, drastically lowering thread friction coefficients and resisting tool impact.
The fatigue lifecycle of a wheel bolt determines passenger safety. Unlike cheap budget fasteners manufactured via simple single-point lathe turning, aerospace-grade titanium hub bolts demand complex multi-stage manufacturing protocols.
| Process Parameter | Cut Thread (Budget Machining) | Rolled Thread (Yevzo Standard) |
|---|---|---|
| Grain Flow Integrity | Cuts across metal grain lines, introducing micro-notches | Continuous grain flow follows contour of the thread flanks |
| Root Tensile Stress Concentration | High localized stress notches at thread root base | Burnished, compressive residual stress layer at root |
| Surface Smoothness (Ra) | Rougher surface (Ra 1.6 - 3.2 µm) | Mirror-smooth burnished finish (Ra < 0.4 µm) |
| Cyclic Fatigue Endurance | Premature fatigue failure under lateral cornering loads | >250% higher fatigue lifecycle under track conditions |
| Thread Shear Strength | Standard shear threshold | Work-hardened flank surface increases shear resistance |
Every Yevzo titanium hub bolt is fabricated with thread rolling dies operating under high hydraulic pressures to ensure zero thread peeling and fatigue-resistant performance.
The hex or spline head of our hub bolt is forged under induction heat at exact recrystallization temperatures, ensuring homogeneous crystalline density and high ultimate shearing capability.
Tolerances on floating collars and seat radiuses (R12, R13, R14) are held within ±0.01mm via Swiss-type multi-axis CNC turn-mill stations to deliver 100% full-surface seating against wheel rims.
Vacuum annealing eliminates internal stresses post-heading and rolling. The bolts exhibit balanced ductility (elongation > 10%), ensuring ductile yield warning rather than brittle failure under catastrophic shear.
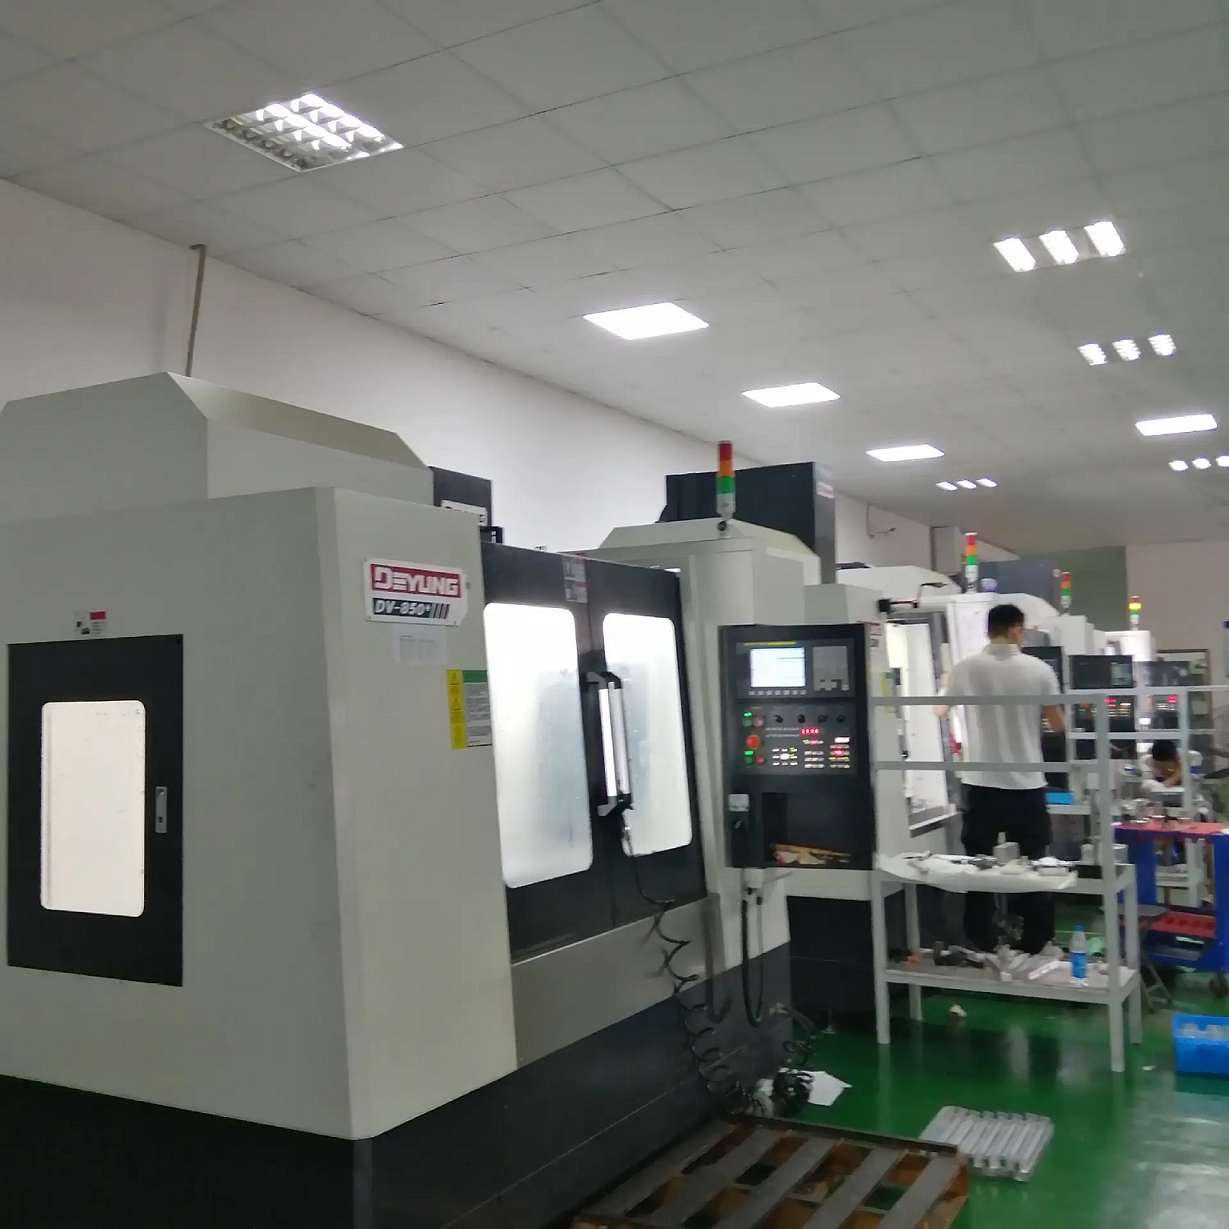
Founded in 2013 in the heart of China’s Titanium Valley, Yevzo integrates raw bar processing, metallurgical testing, CNC manufacturing, surface treatment, and ultrasonic cleaning in an end-to-end quality-controlled environment.
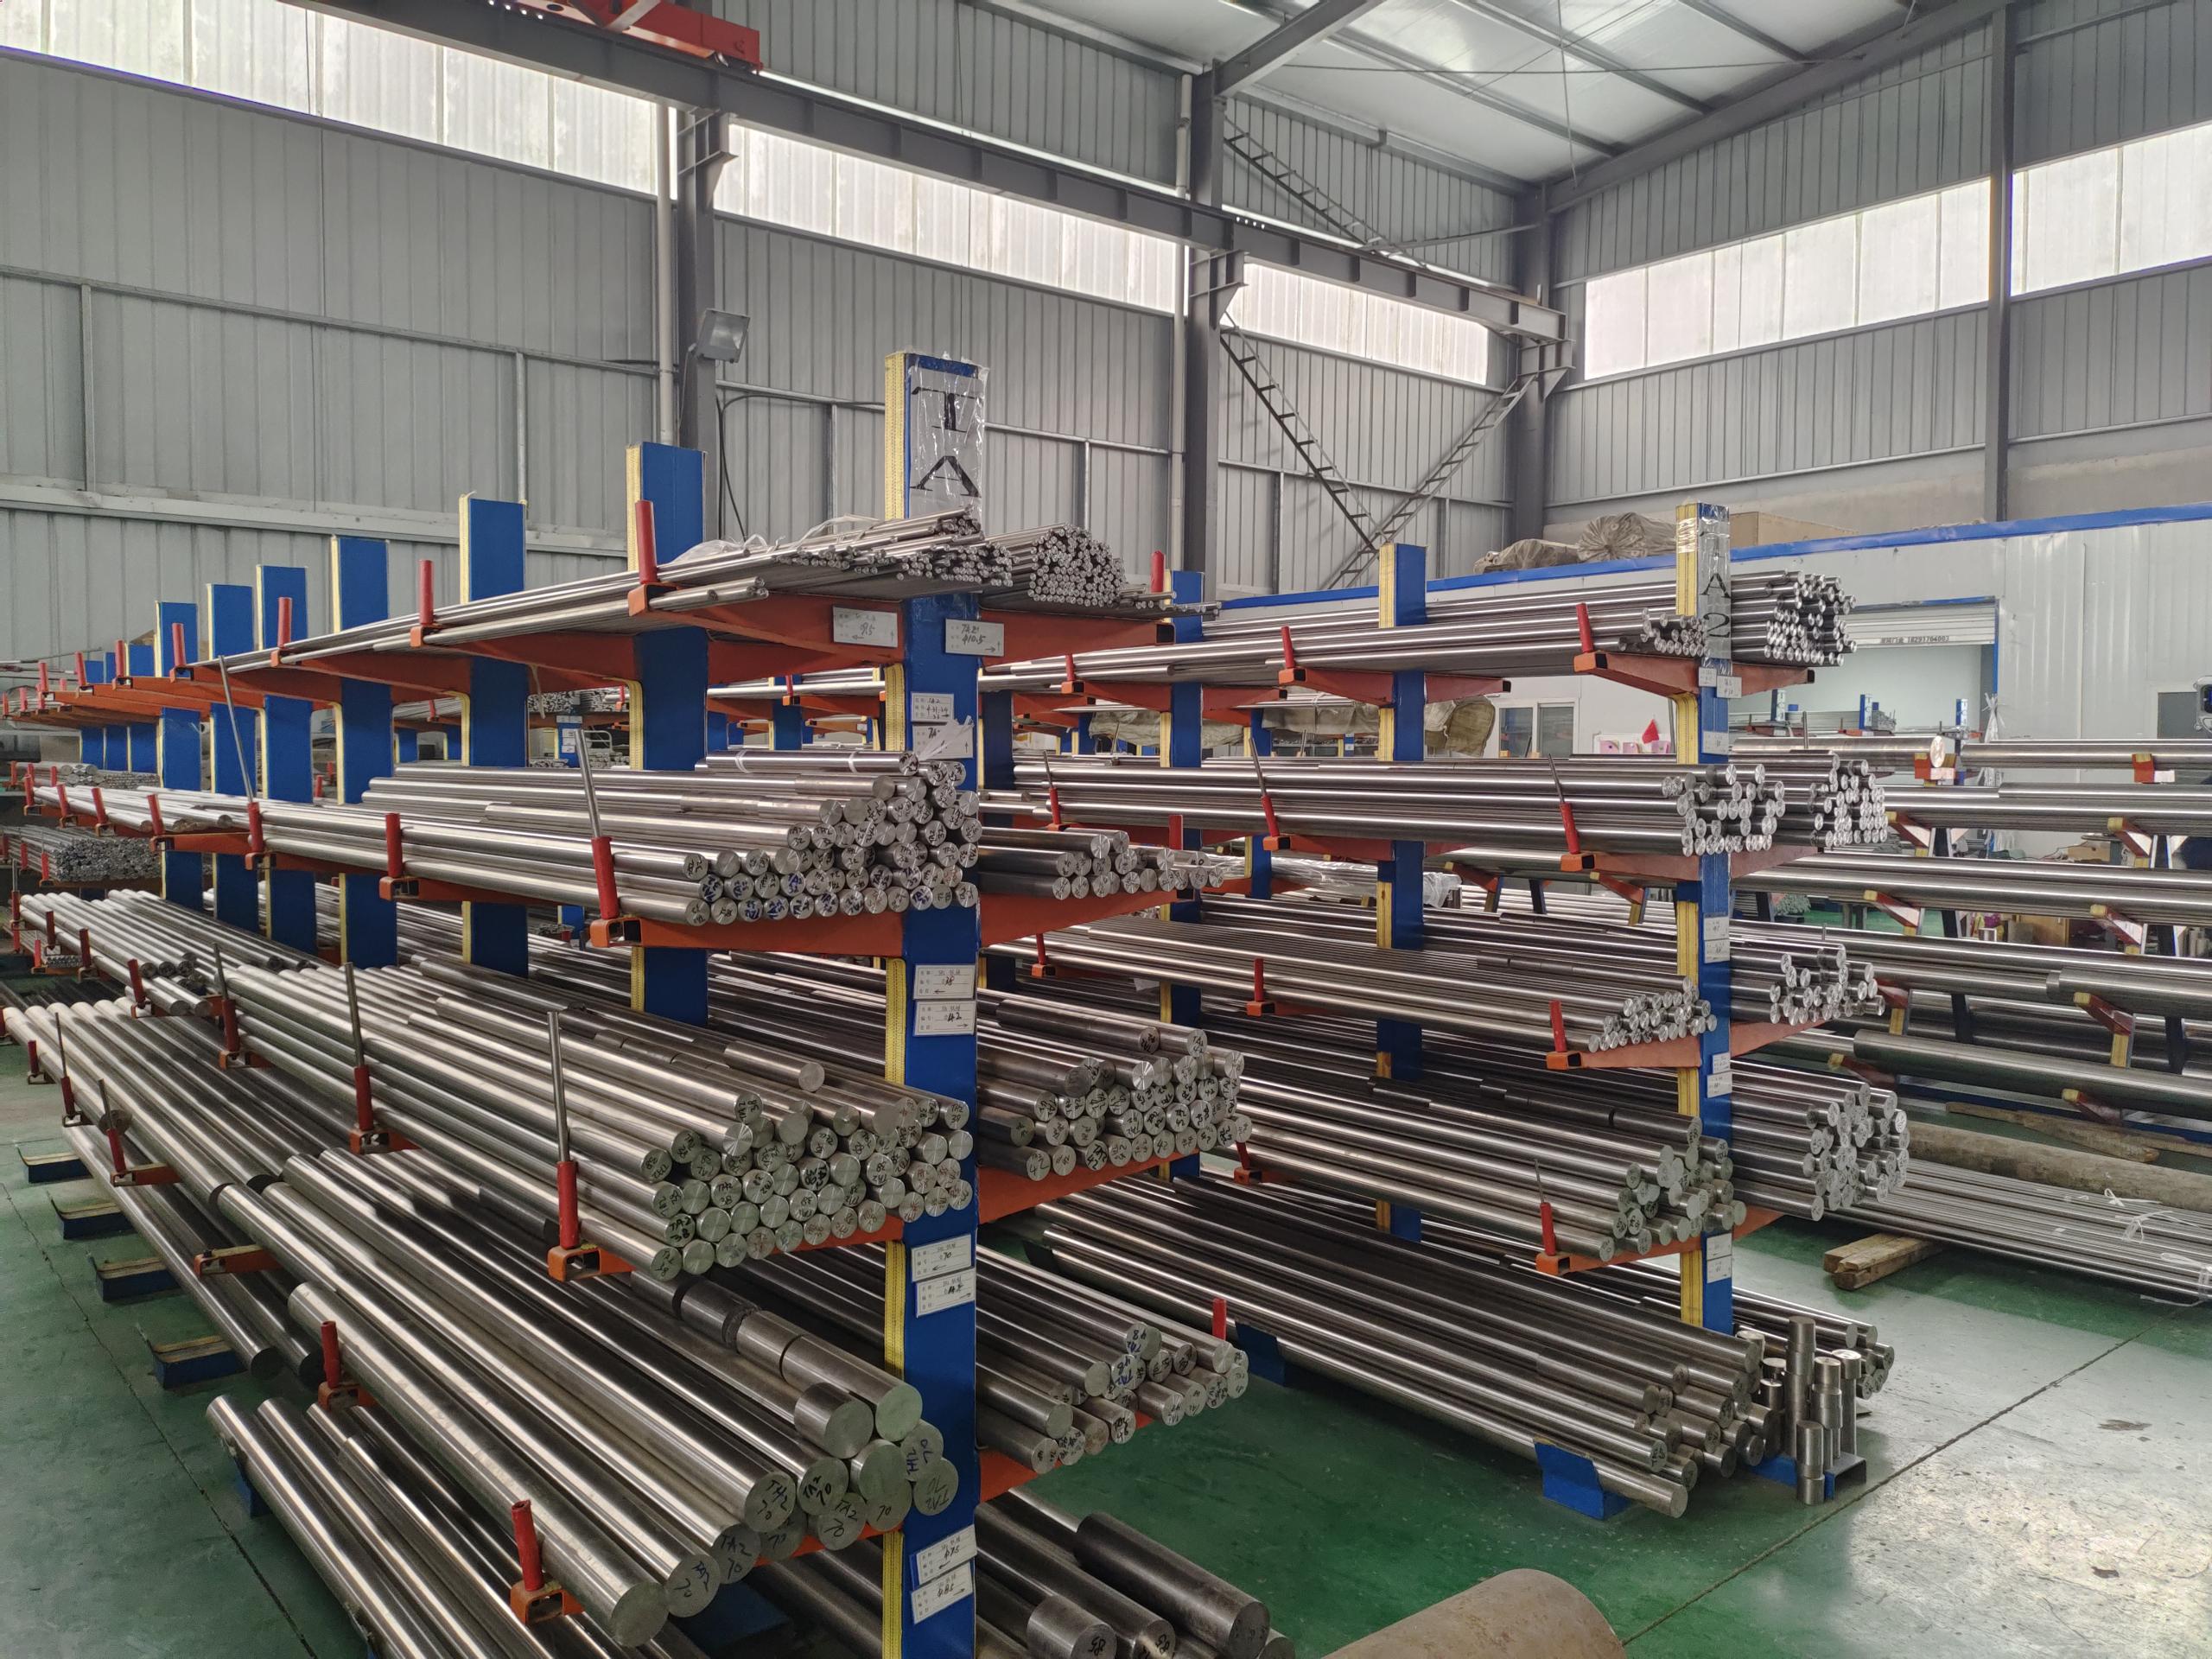
Incoming ASTM B348 Grade 5 bars undergo PMI spectrometry and ultrasonic inspection to guarantee zero microscopic porosity or interstitial defects before precision cutting.
Our heavy CNC turning and 3-axis CNC milling batteries machine bolt hex contours, floating collars, and internal security sockets to strict ISO 2768-m precision tolerances.
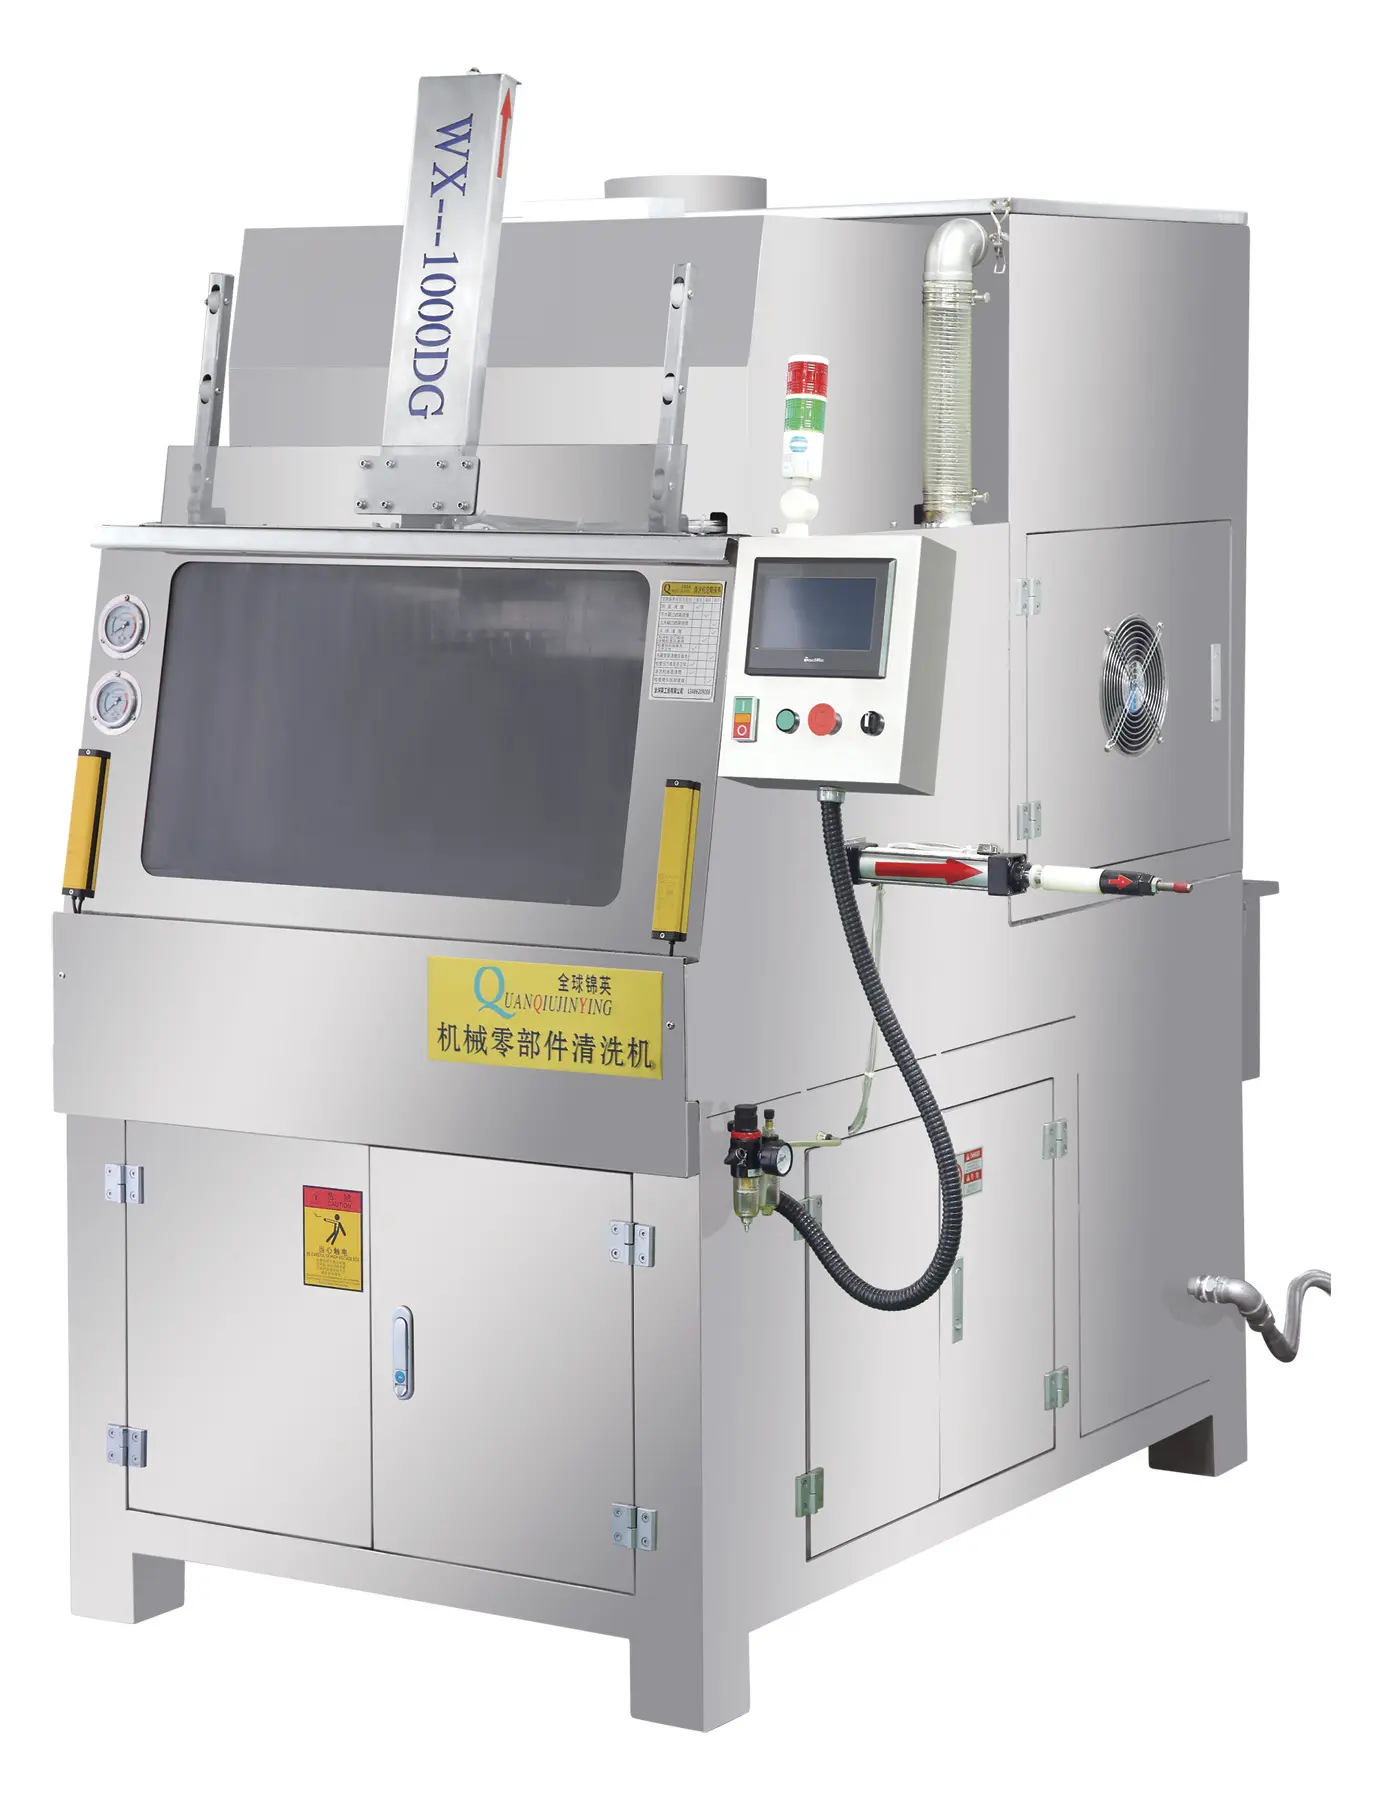
Multi-stage automated ultrasonic degreasing lines and micro-pore purge processes strip all coolant residues, metal swarf, and impurities prior to vacuum treatment or PVD coloring.
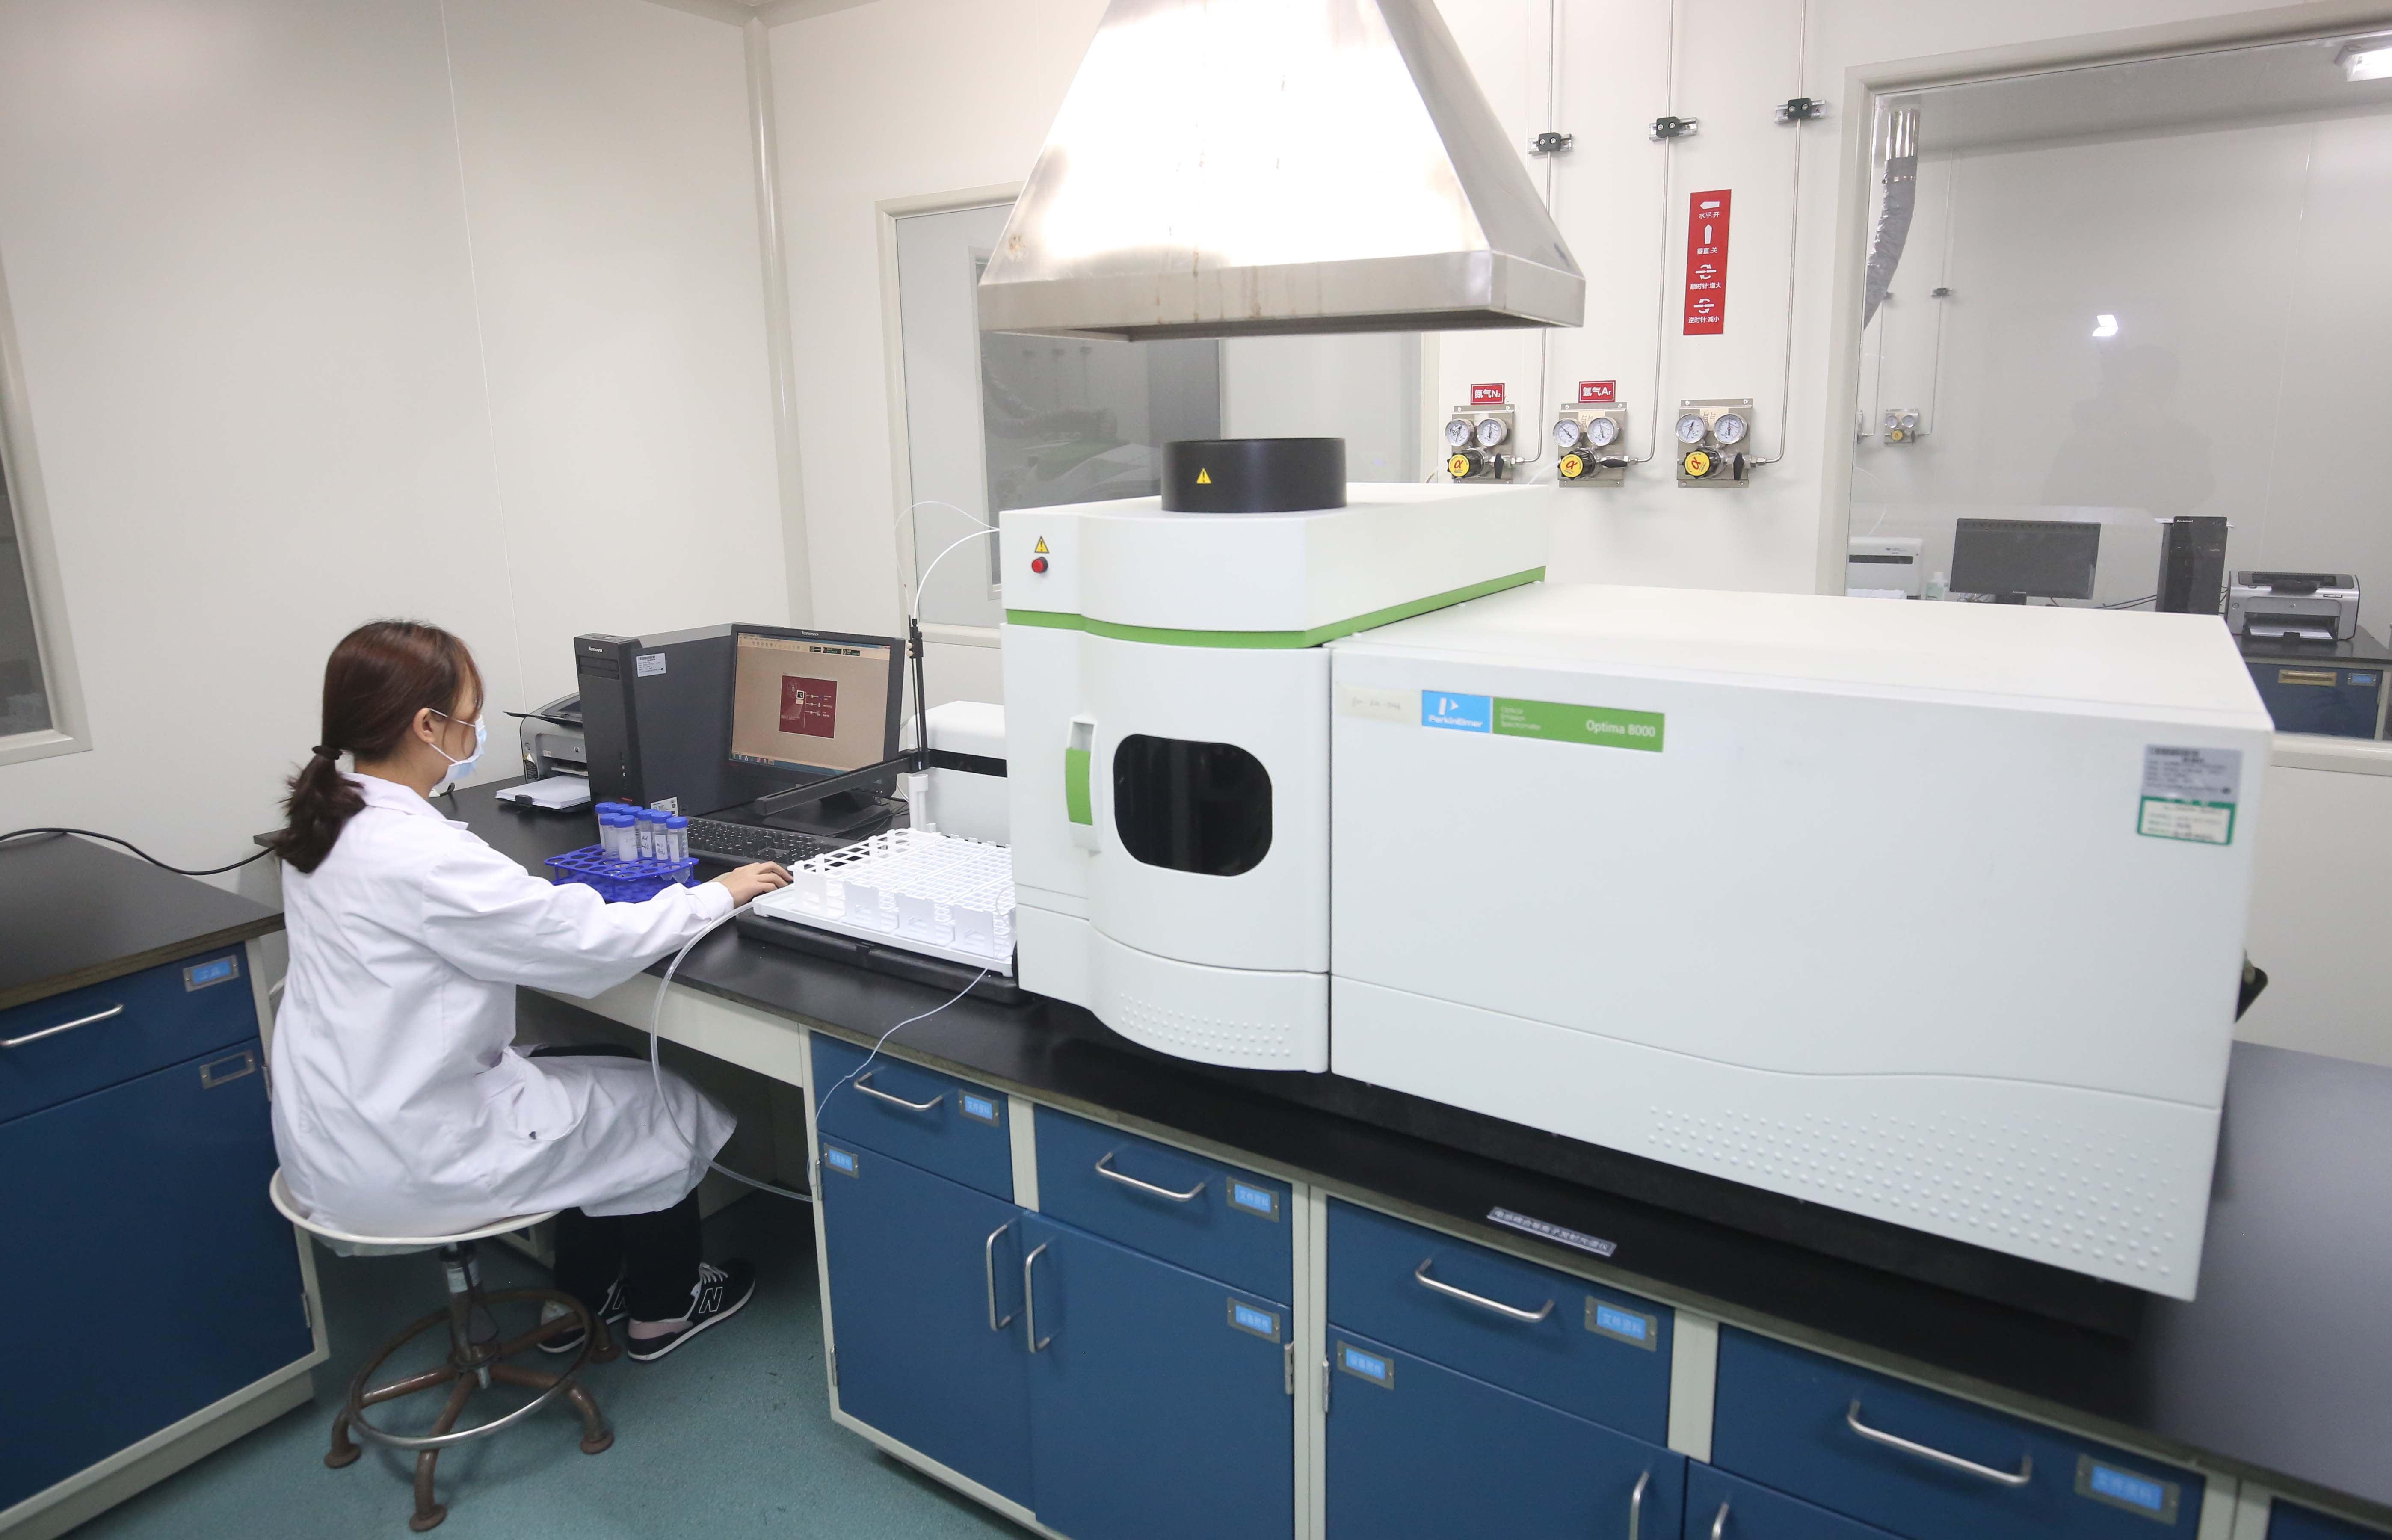
Dedicated metallurgical and mechanical engineers perform finite element stress simulation, hardness mapping, dynamic clamp load analysis, and custom CAD development.
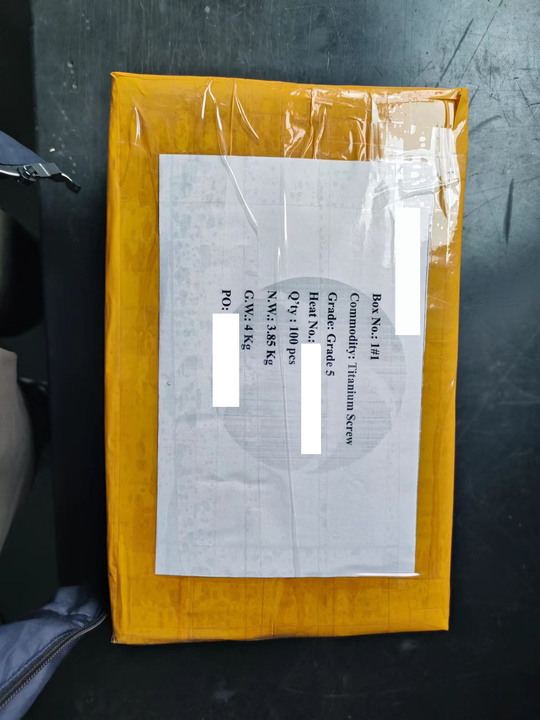
Finished titanium hub bolts are individually encased in anti-scratch foam partitions, boxed with protective thread caps, and labeled with batch traceability barcoding.
Answers to critical questions asked by automotive engineers, aftermarket parts distributors, and procurement directors sourcing titanium wheel hardware.
Partner directly with Yevzo Titanium Metal Co., Ltd. Send us your required thread pitch, shank length, seat profile (Cone, Ball, or Floating), and desired surface finish. Our engineering team reviews all CAD drawings (STEP, DWG, PDF) and delivers detailed wholesale manufacturing quotations within 12 business hours.