Ti-6Al-4V Titanium Screws: Engineering Specifications & Procurement Insights
High-strength Grade 5 aerospace-grade titanium fasteners, custom CNC machined and cold/hot forged for high-performance automotive, robotics, marine, and motorsport assemblies.
Why Global Industrial Buyers Specify Ti-6Al-4V Titanium Screws
In modern mission-critical applications across aerospace engineering, hypercar chassis manufacturing, robotics, and offshore marine infrastructure, mechanical designers constantly face the challenging compromise between mechanical yield strength and structural deadweight. For decades, Class 8.8, 10.9, and 12.9 alloy steels have served as the traditional fastening standard. However, steel introduces substantial weight penalties and is chronically susceptible to galvanic oxidation, stress corrosion cracking (SCC), and chloride pitting. Commercially Pure Grade 2 titanium solves the corrosion equation but lacks the shear resistance and cyclic fatigue limits needed for high-stress dynamic assemblies. This critical junction is where Ti-6Al-4V titanium screws (UNS R56400 / ASTM Grade 5) establish uncontested dominance.
Alpha-Beta Duplex Microstructure
Ti-6Al-4V represents an alpha-beta alloy containing 6% aluminum to stabilize the alpha phase and 4% vanadium to stabilize the ductile beta phase. This balanced metallurgy produces an isotropic fastener offering a minimum tensile strength exceeding 895 MPa (often elevated beyond 950–1050 MPa after controlled thermal-mechanical finishing) alongside a density of merely 4.43 g/cm³. The direct engineering dividend is a strength-to-weight ratio that outclasses Class 10.9 steel by over 42%, while simultaneously offering near-zero non-magnetic susceptibility and exceptional fatigue life under cyclic harmonic vibration.
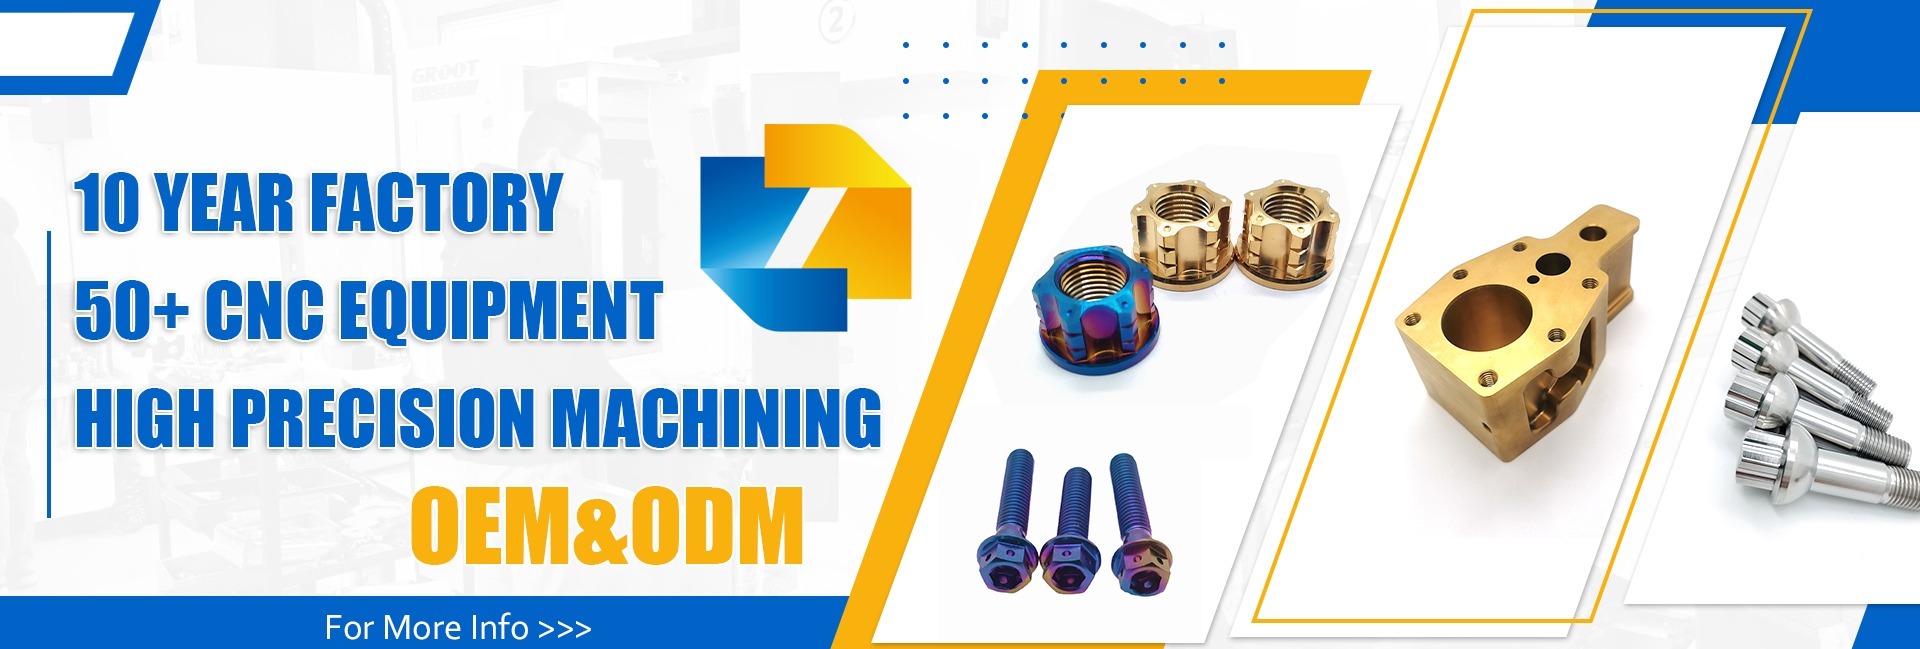
At Yevzo Titanium Metal Co., Ltd., we produce Ti-6Al-4V titanium screws through rigid cold/hot heading coupled with precision rolled threads or multi-axis CNC Swiss turning centers. We safeguard complete grain alignment along the thread root, eliminating micro-notch sensitivity and avoiding premature fastener shear.
Factory-Direct Ti-6Al-4V Fastener Lineup
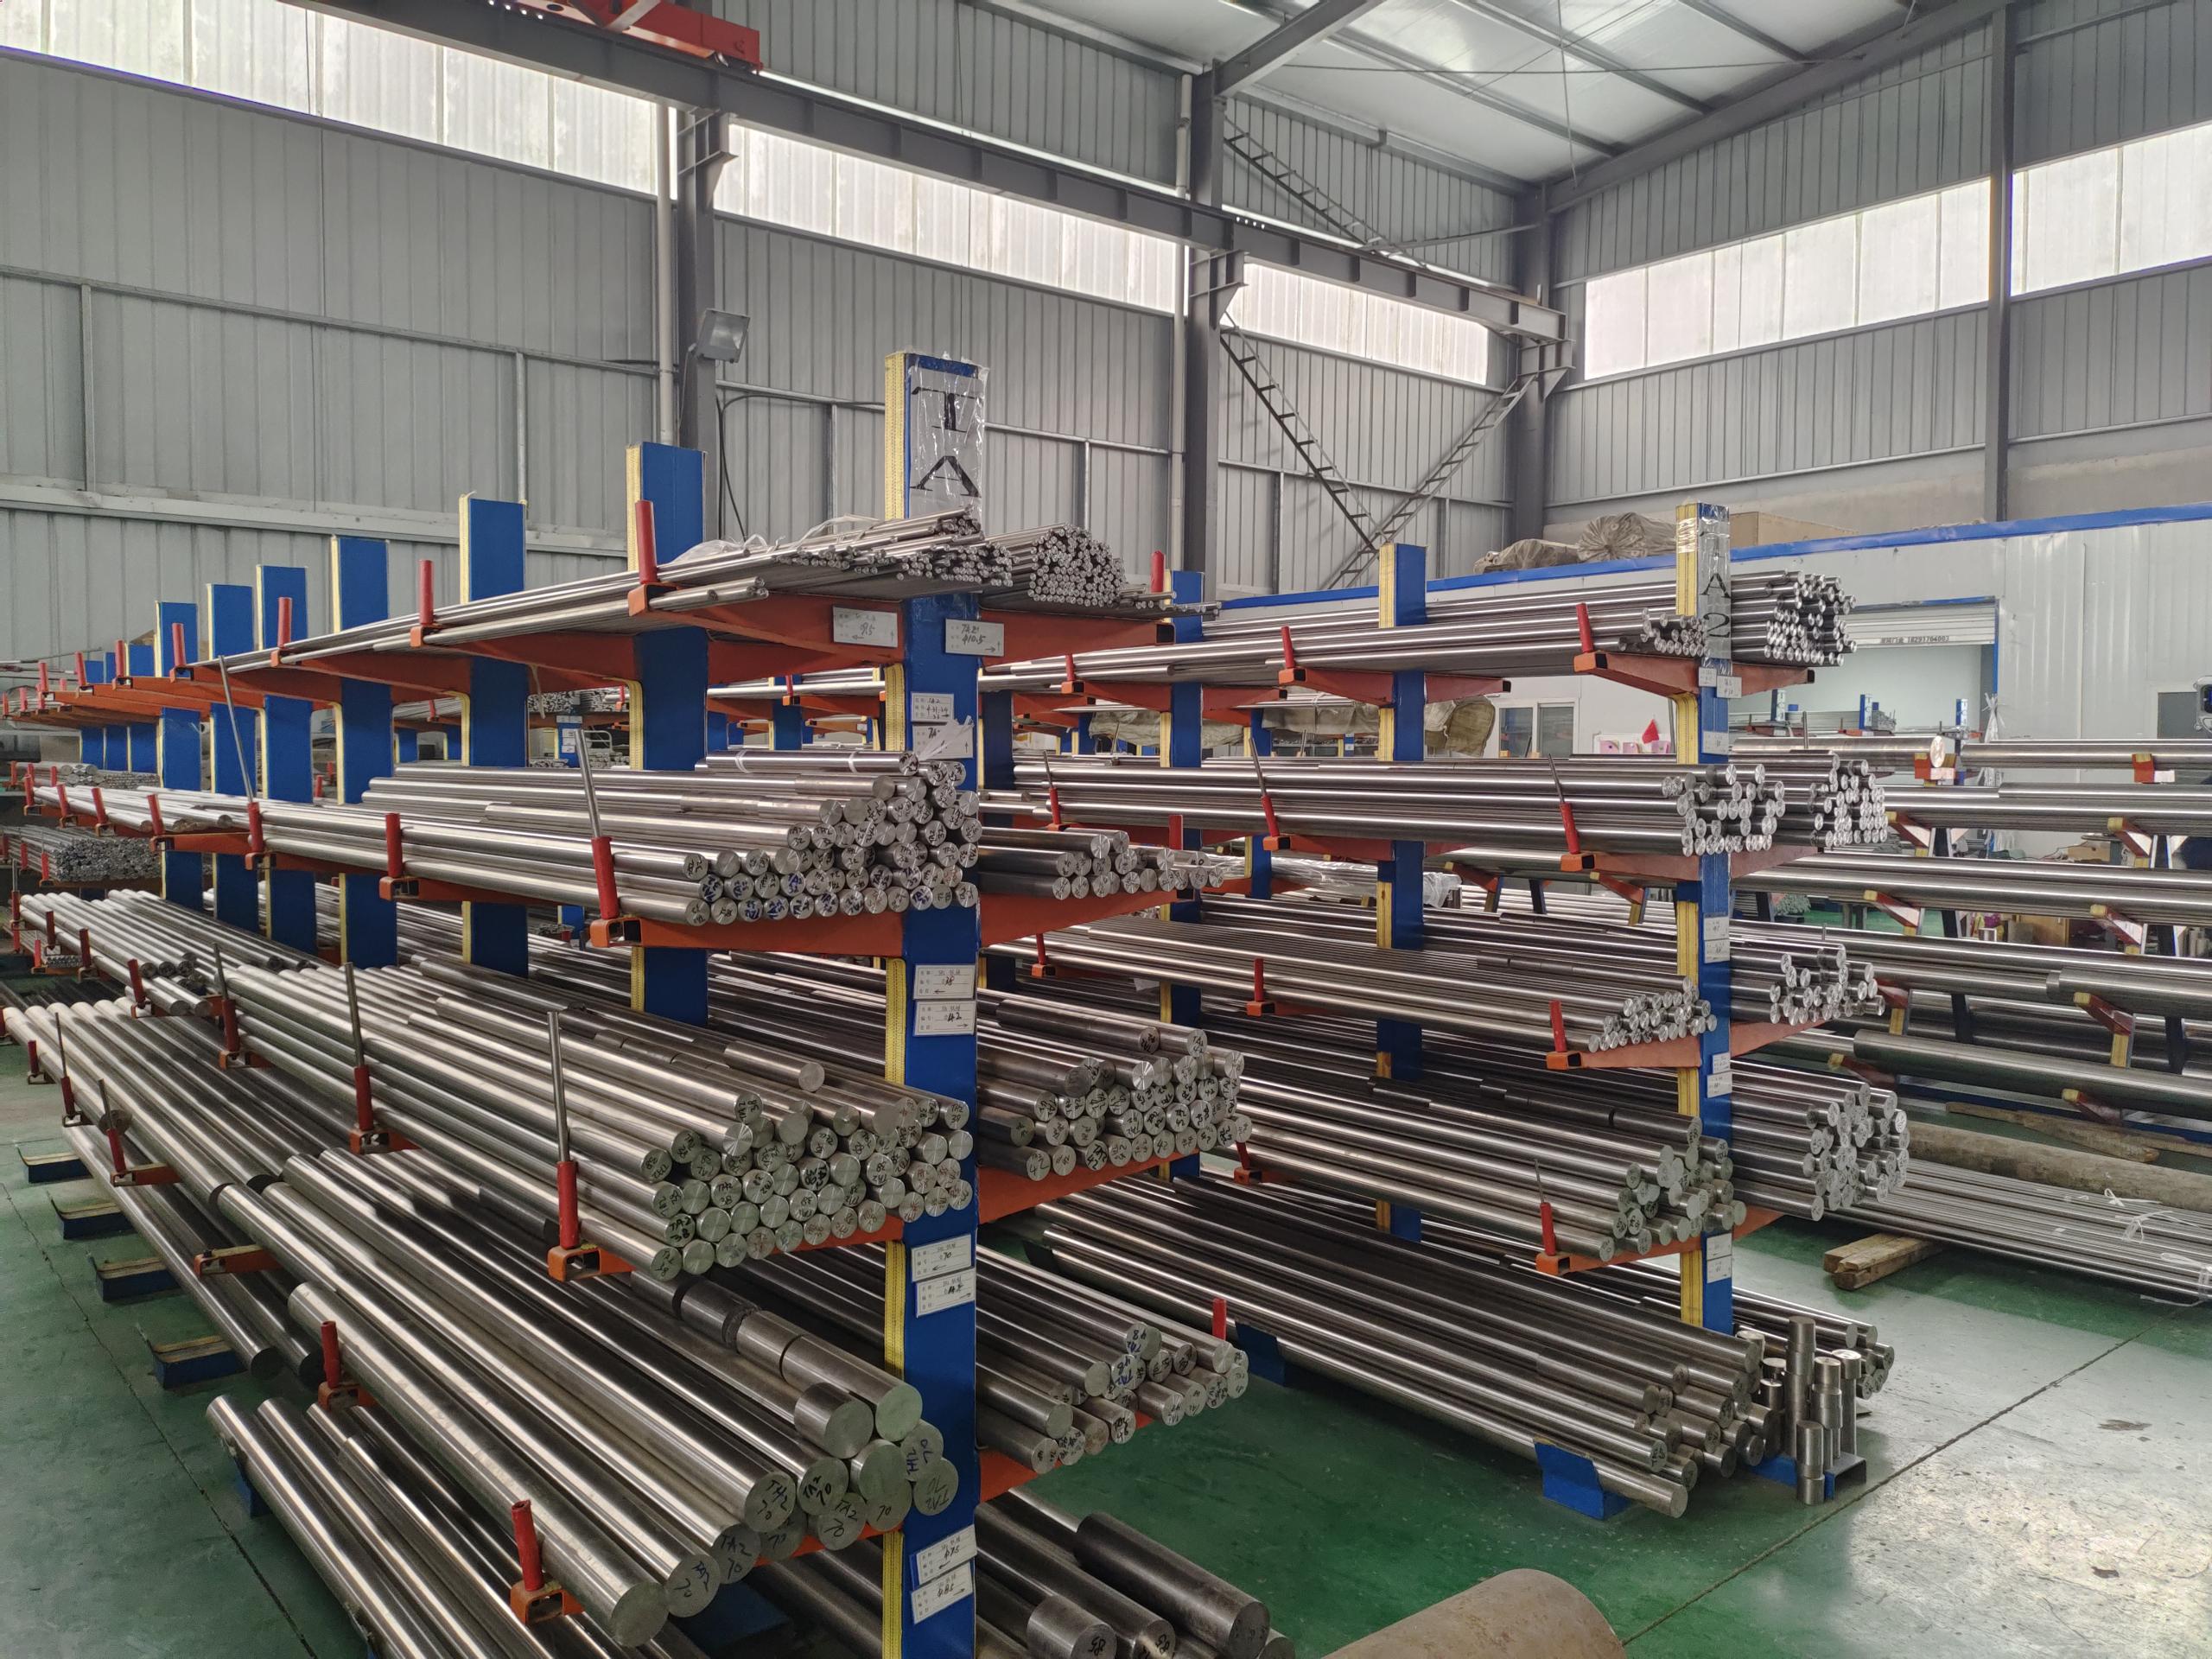
Discover our standard catalogue configurations and customizable structural geometries. Each component is fabricated from ultrasonically inspected vacuum-arc remelted (VAR) Ti-6Al-4V titanium bar stock.
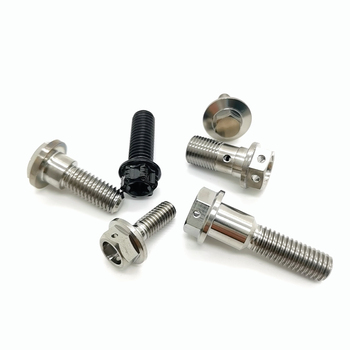
Ti-6Al-4V Hex Flange Screws
Engineered to DIN 6921 and ISO 4162. Large integrated load-bearing face distributes high clamp loads across carbon fiber and magnesium substrates without galling or crushing.
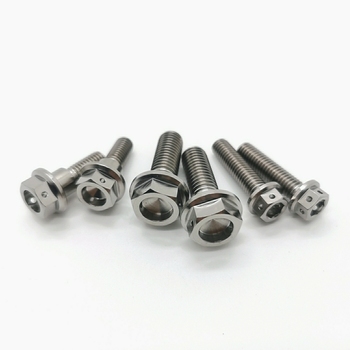
Torx / Hex Socket Cap Screws
Manufactured to DIN 912 and ISO 4762 standards. Features precision broached or cold-formed sockets to provide optimal torque engagement and prevent drive-cam stripping.
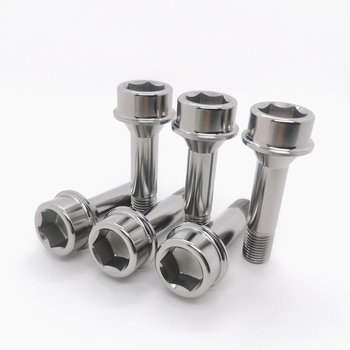
M12 / M14 Titanium Lug Screws
Dedicated motorsport wheel fastening systems. CNC turned 60° conical and floating ball seats that resist extreme cyclic thermal transients during high-load track braking.

Anodized Countersunk Screws
Compliant with DIN 7991 and ISO 10642. Flush-surface aesthetic fitting for aero components, robotic arms, and high-end superbike structural fairing cowls.
Mechanical Performance Matrix: Ti-6Al-4V vs. Traditional Fastener Materials
Data verified in accordance with ASTM B348, ASTM F136, ISO 898-1, and ISO 3506. Understand how Ti-6Al-4V titanium screws outperform competitive alloys across mission-critical indicators.
Technical Property Comparison
| Mechanical / Physical Property | Ti-6Al-4V (Grade 5 Annealed) | Commercially Pure Ti (Grade 2) | Class 10.9 Structural Steel | 316L Stainless Steel (A4-80) | 7075-T6 Aluminum Alloy |
|---|---|---|---|---|---|
| Tensile Strength, Ultimate (Rm) | 900 – 1050 MPa | 345 – 450 MPa | 1000 – 1040 MPa | 800 MPa | 540 – 570 MPa |
| Yield Strength (Rp 0.2) | 830 – 910 MPa | 275 – 350 MPa | 900 – 940 MPa | 600 MPa | 480 – 505 MPa |
| Material Density (g/cm³) | 4.43 g/cm³ | 4.51 g/cm³ | 7.85 g/cm³ | 8.00 g/cm³ | 2.81 g/cm³ |
| Specific Strength (Yield/Density) | 194.1 kN·m/kg | 66.5 kN·m/kg | 117.2 kN·m/kg | 75.0 kN·m/kg | 176.1 kN·m/kg |
| Modulus of Elasticity (E) | 114 GPa | 103 GPa | 210 GPa | 193 GPa | 72 GPa |
| Fatigue Limit (10⁷ Cycles) | 510 MPa | 180 MPa | 420 MPa | 260 MPa | 160 MPa |
| Seawater Corrosion Rate | < 0.0001 mm/year | < 0.0001 mm/year | 0.120 mm/year | 0.005 mm/year | Severe Pitting |
| Thermal Operating Range | -250°C to +420°C | -196°C to +200°C | -40°C to +300°C | -196°C to +400°C | -50°C to +120°C |
Engineering Note: The lower Young's Modulus of Ti-6Al-4V (114 GPa versus 210 GPa for steel) imparts superior resilience to cyclic shock loads. Titanium fasteners absorb elastic energy under dynamic deflection without taking permanent plastic set, effectively preventing fastener loosening in high-vibration environments.
Future Procurement & Technological Trends in Titanium Fastening
Global procurement teams are shifting toward smart, automated, and decarbonized supply chains. Here are the macro shifts shaping the future of Ti-6Al-4V fastener acquisition.
Near-Net-Shape Cold/Hot Forming
Machining complex titanium screws from solid bar stock generates high scrap rates. Advanced producers are adopting multi-station warm and hot heading methods to form screw heads near net shape, cutting raw billet consumption by 35% while aligning metallurgical grain flow.
Electrification & Low-Carbon Footprint
In electric vehicle platforms and urban air mobility (eVTOL) crafts, reducing every kilogram of chassis structural weight increases battery range. Consequently, procurement officers are aggressively phasing out zinc-flake coated alloy steel bolts in favor of Grade 5 titanium bolts.
Stringent Carbon & ESG Traceability
Tier-1 automotive and aerospace firms now require detailed Scope 1, 2, and 3 emissions tracking alongside Certified Material Test Reports (CMTR). Sourcing from verified smelting clusters like Baoji guarantees end-to-end vacuum induction melting (VIM) compliance.
Advanced Tribological Surface Modification
Uncoated titanium faces micro-welding and thread galling when subjected to high friction torquing. The industry is moving beyond standard Type II anodizing toward Physical Vapor Deposition (PVD), Diamond-Like Carbon (DLC), and Micro-Arc Oxidation (MAO) to eliminate galling.
Industrial Heritage in China's "Titanium Valley"
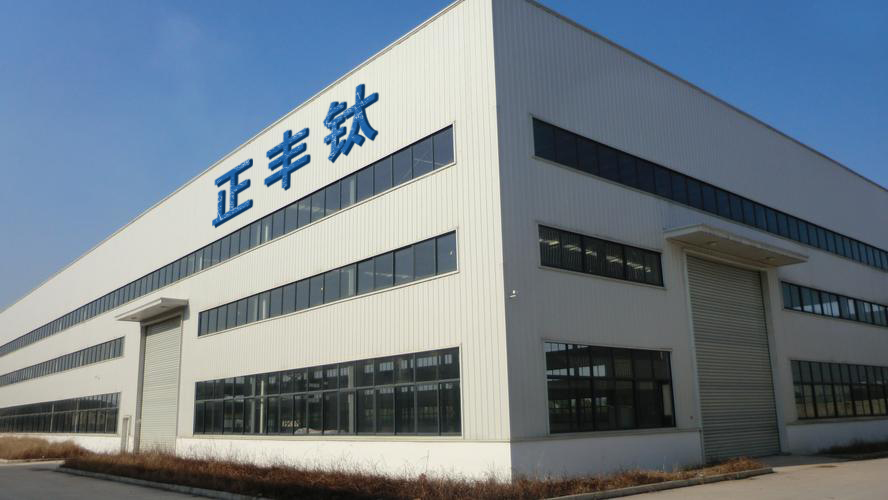
Yevzo Titanium Metal Co., Ltd. is located in the Honeycomb Industrial Park, Baoji High-Tech Development Zone, Shaanxi Province. Operating since 2013, our integrated manufacturing and testing facilities sit at the core of Baoji's titanium production hub, giving us direct access to high-purity Grade 5 sponge and triple-melted VAR titanium bar stock.
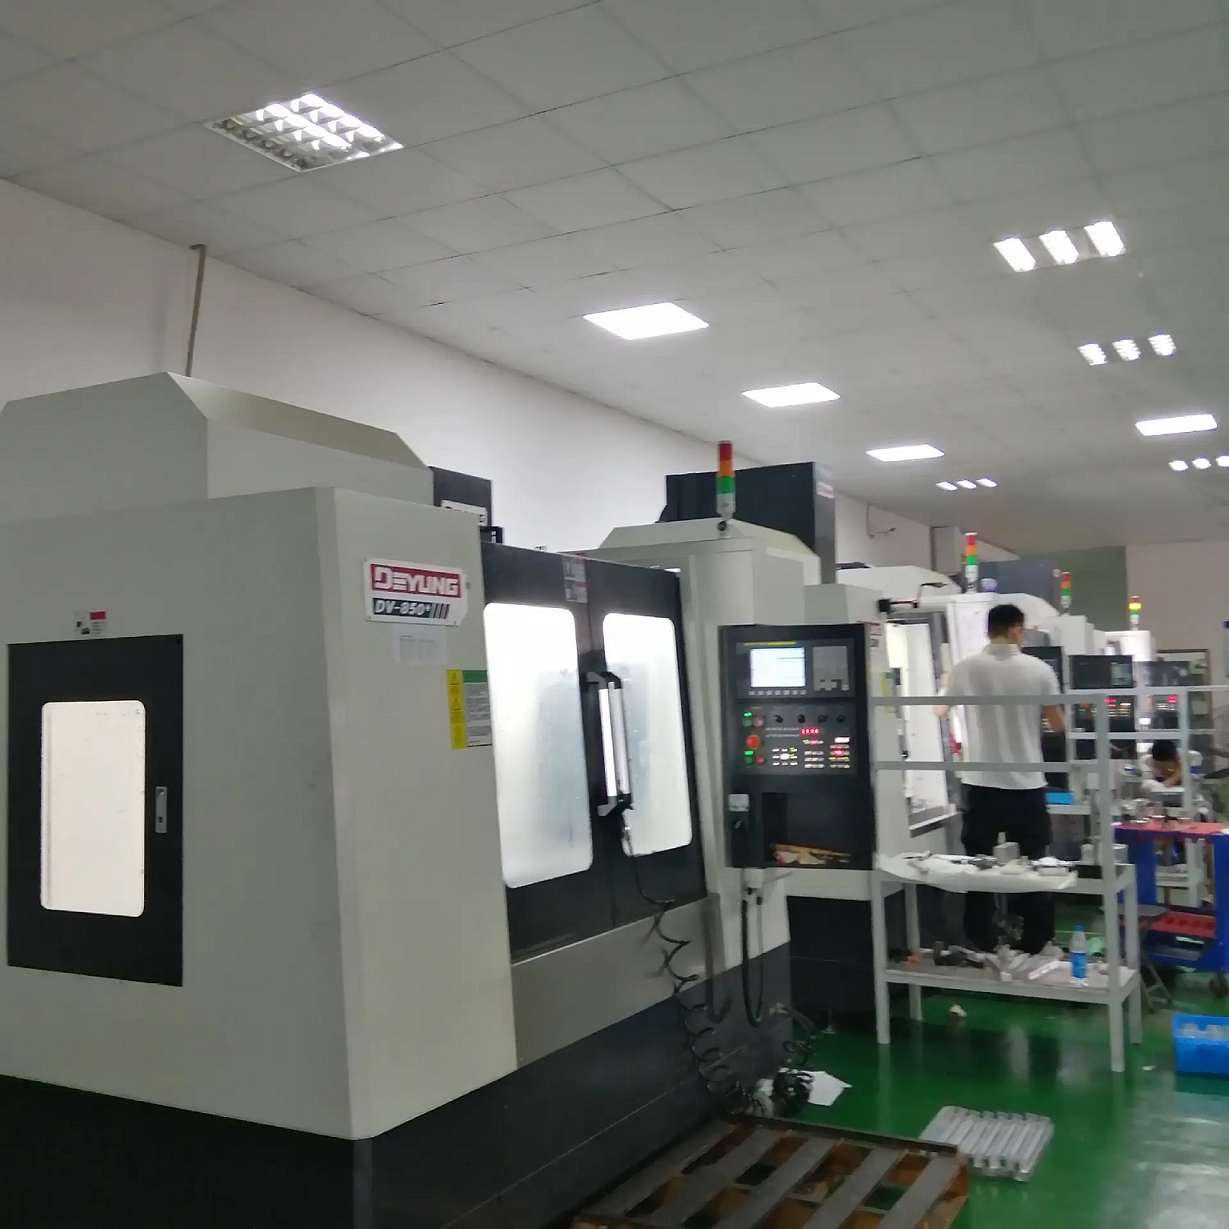
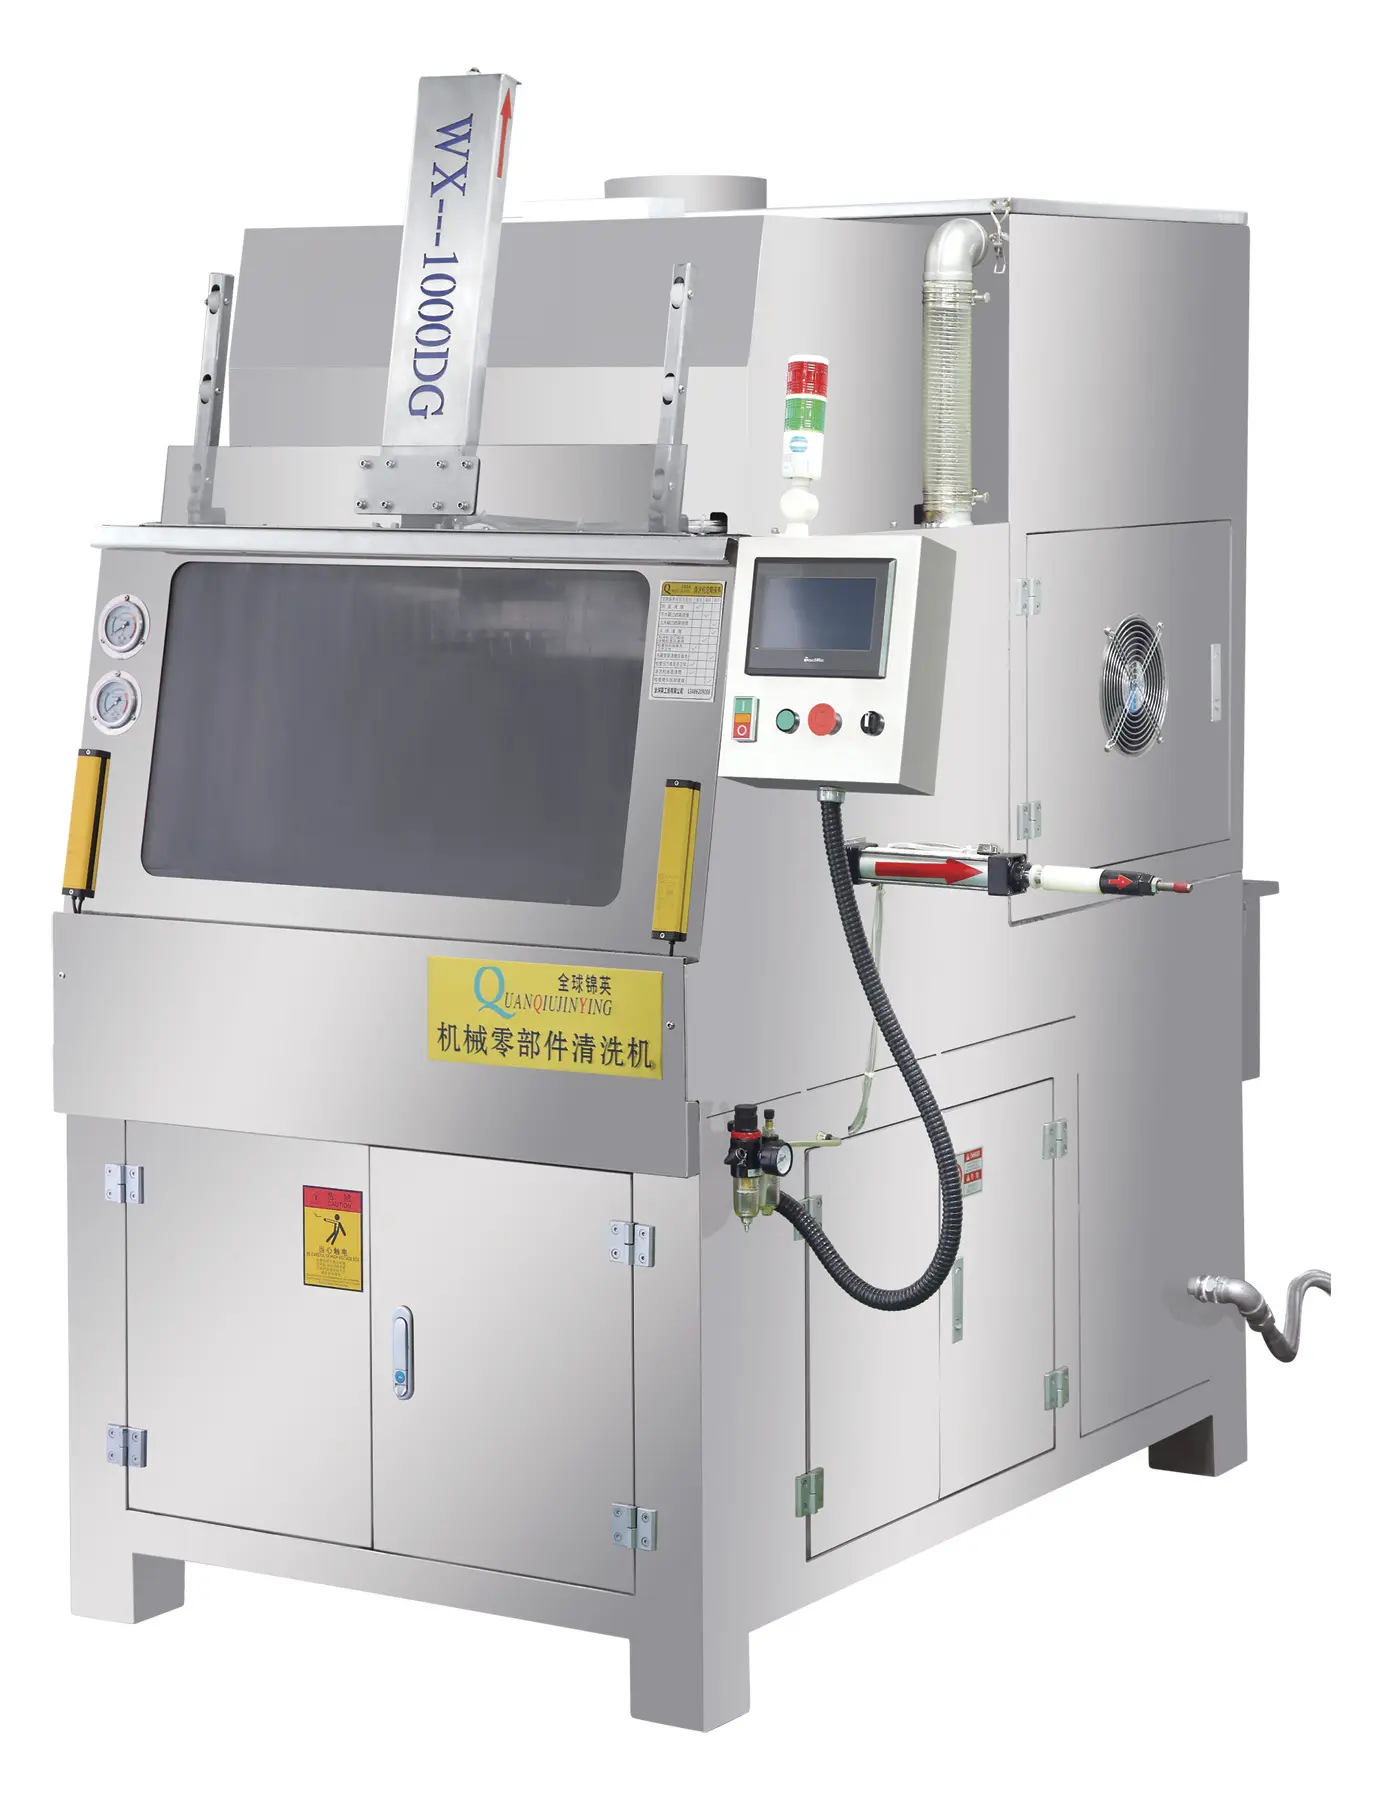
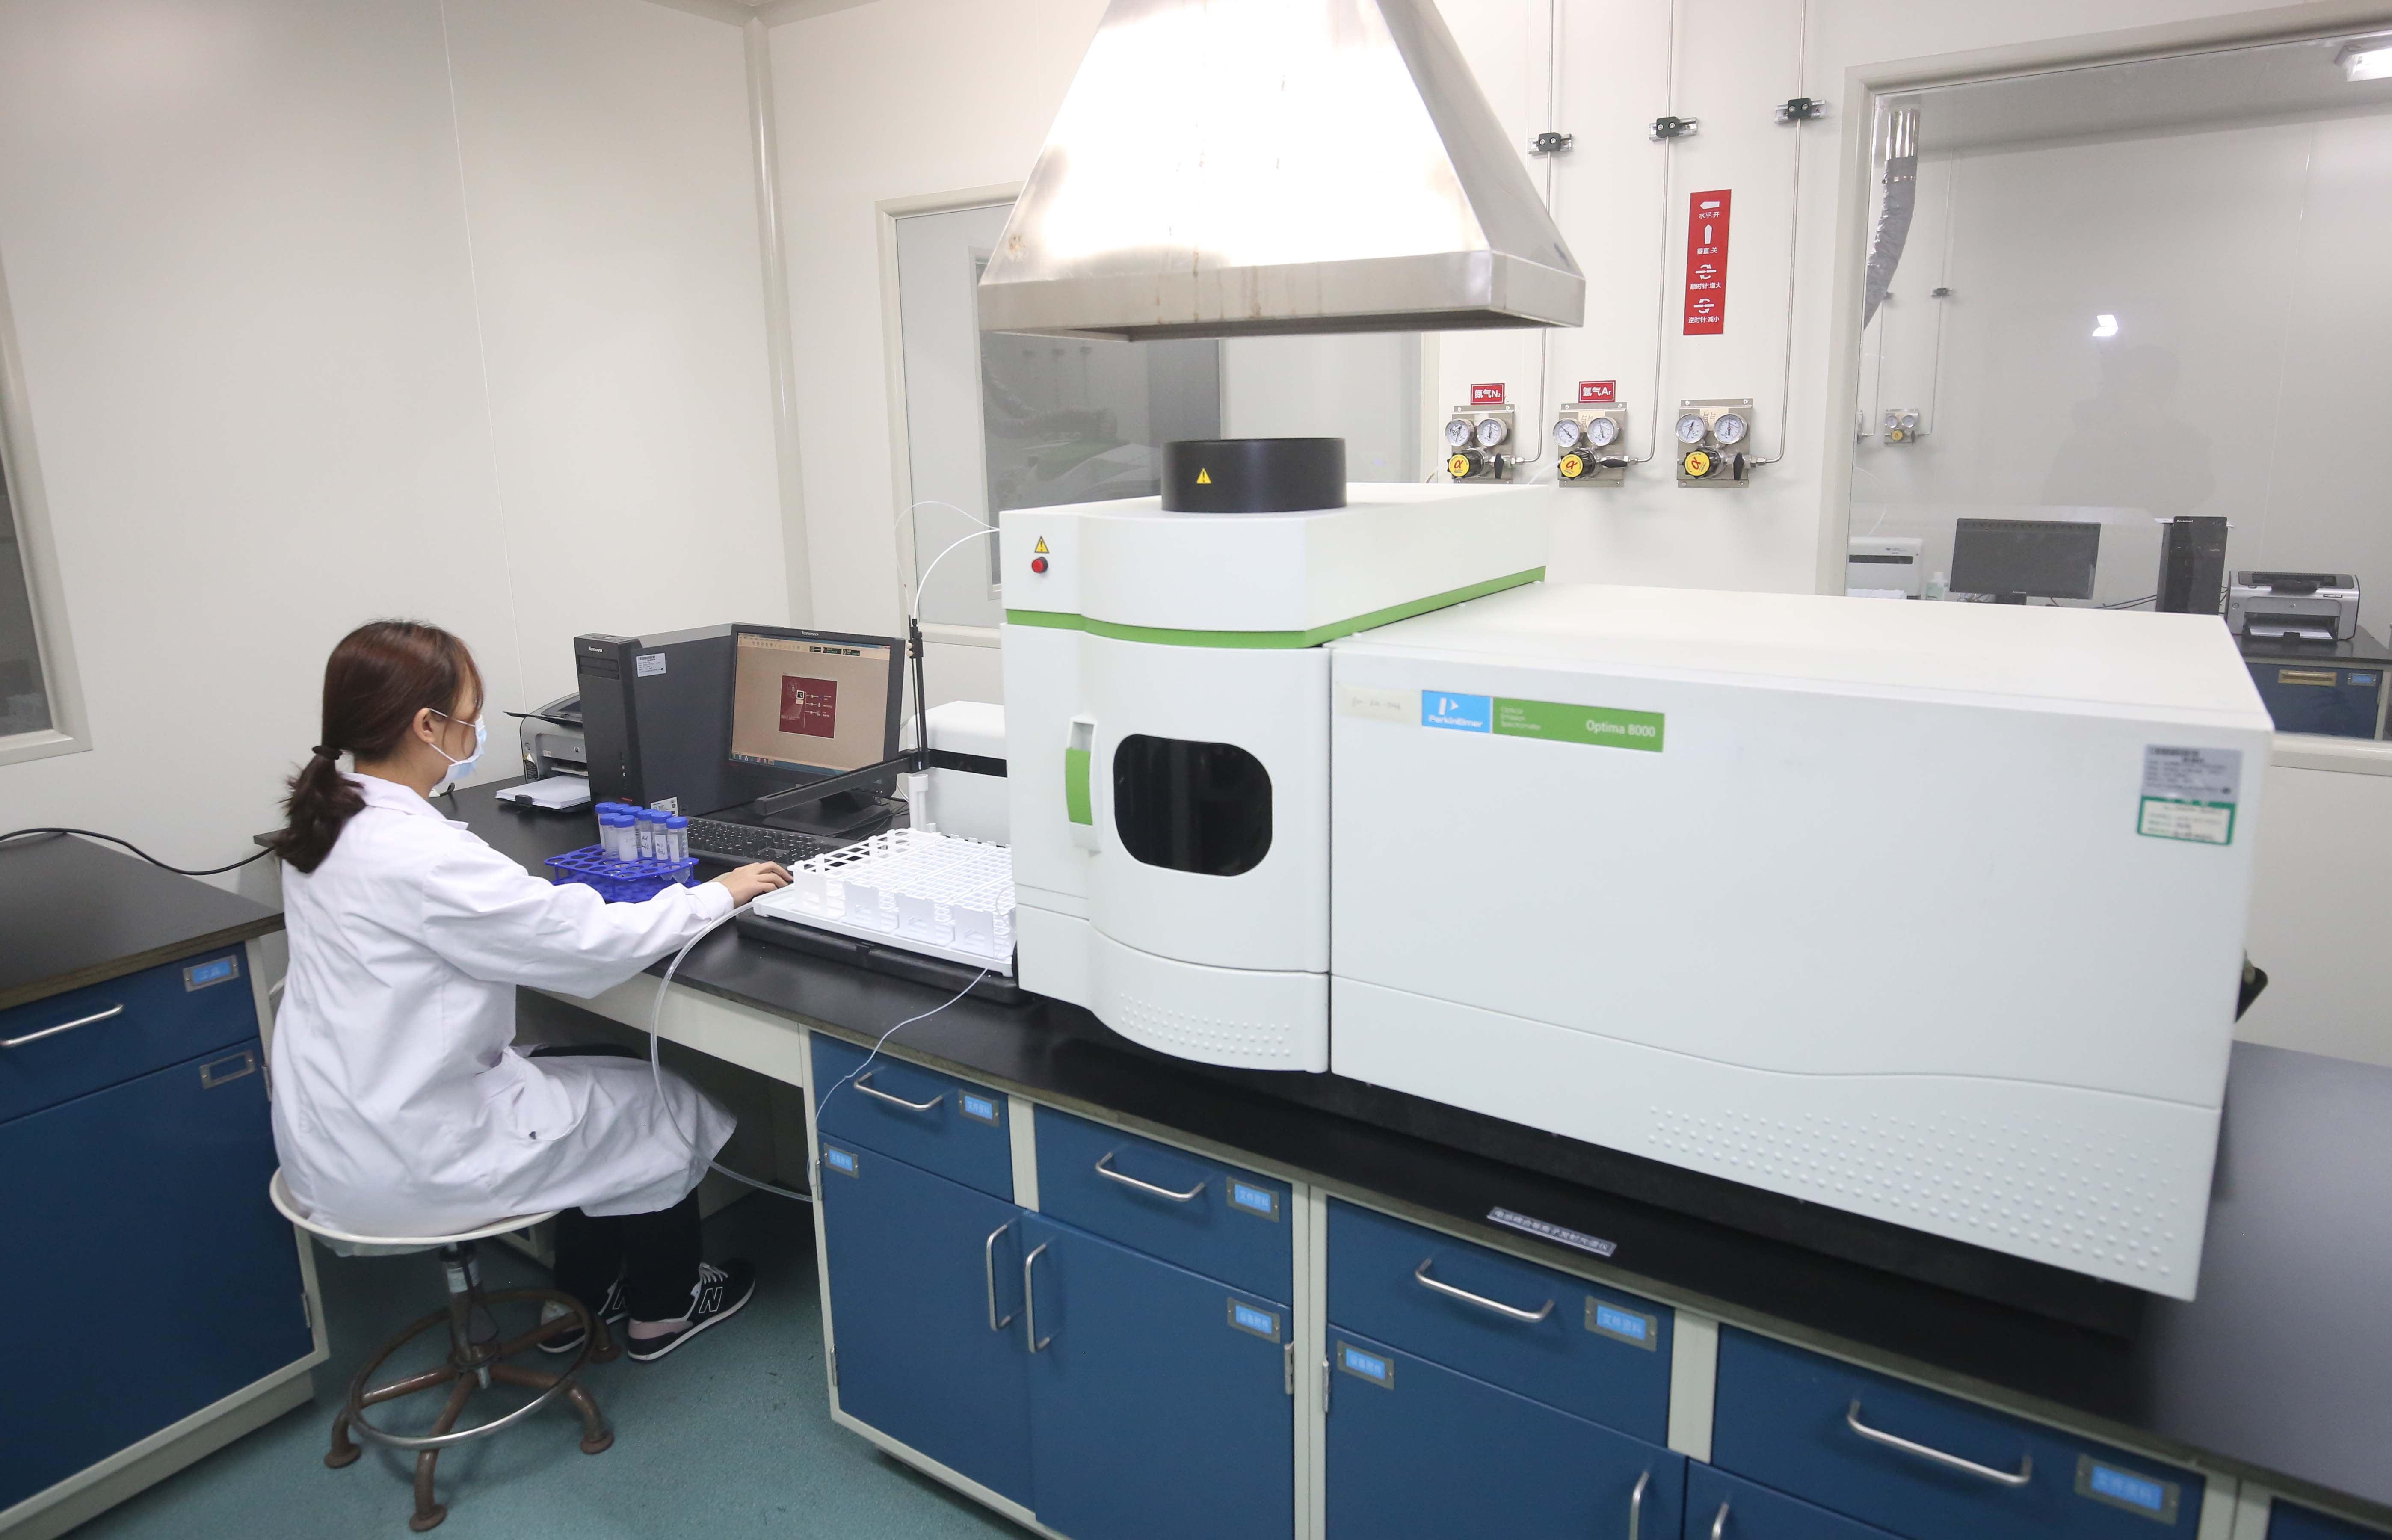
Our workshop houses over 100 sets of advanced processing equipment, including high-precision 3-axis, 4-axis, and 5-axis CNC machining centers, automatic thread rolling machines, vacuum annealing chambers, and continuous ultrasonic washing lines. Under our core operating philosophy of "Titanium concentration, service intention," every production run undergoes dimensional validation, optical thread profiling, and spectroscopic verification.
- ASTM B348, AMS 4928 & ISO 5832-3 compliance
- Strict 100% thread gauge verification (6g / 6H)
- Full EN 10204 3.1 Material Test Reports available
- Comprehensive custom OEM/ODM drawing engineering
Verified Facility Divisions
Incoming ultrasonic flaw detection and PMI spectroscopic verification.
High-speed precision turning and CNC thread milling down to ±0.005mm.
De-oiling, multi-stage ultrasonic purging, and precision color anodizing.
Alloy phase stability, mechanical load simulations, and torque-tension R&D.
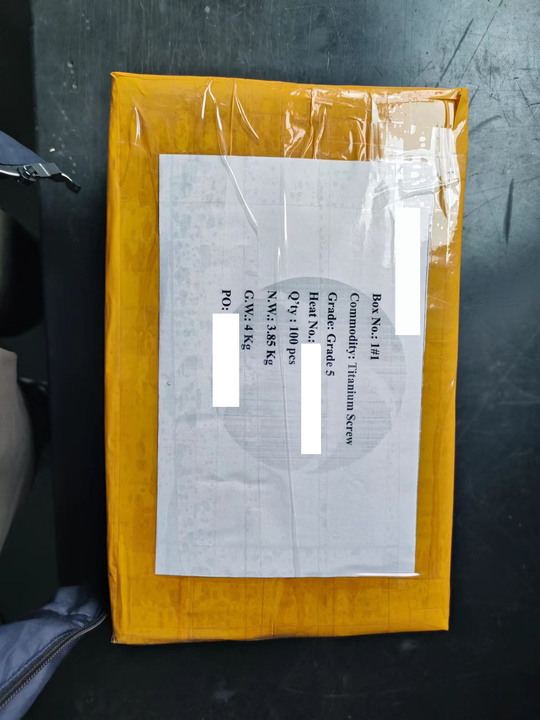
Individual compartmentalized thread sleeves, sealed nitrogen barrier wraps, and shockproof export packaging.
Rigorous Manufacturing & Inspection Flow
Every Ti-6Al-4V titanium screw produced at Yevzo Titanium Metal Co., Ltd. moves through five documented quality gates.
Material Prep
Spectrochemical analysis and ultrasonic flaw detection of Grade 5 titanium round bars.
CNC Machining
Swiss-type turning, cold/hot header forming, and thread rolling for fatigue resistance.
Purge Group
Multi-stage automated ultrasonic cleaning and chemical passivation to prevent contamination.
R&D Validation
Tensile testing, metallographic grain inspection, and optical profile projector analysis.
Package Group
Anti-collision plastic netting, custom batch labeling, and export-grade pallet packaging.
Global Sourcing & Engineering Inquiries
Direct technical answers from the metallurgy and export engineering teams at Yevzo Titanium Metal Co., Ltd.
1. How do Ti-6Al-4V titanium screws compare to Class 10.9 steel and 7075-T6 aluminum screws?
Ti-6Al-4V (Grade 5) provides an optimal strength-to-weight ratio. While Class 10.9 alloy steel provides a tensile strength of 1000–1040 MPa, it has a heavy density of 7.85 g/cm³ and rusts when exposed to moisture. 7075-T6 aluminum is lightweight (2.81 g/cm³) but possesses only 540 MPa tensile strength, has low shear endurance, and easily strips under high torques.
Ti-6Al-4V delivers 900–1050 MPa tensile strength at 4.43 g/cm³ density—offering a 45% weight saving compared to steel while offering more than double the structural yield capability of aerospace aluminum, all combined with virtually immune corrosion resistance in saltwater and chemicals.
2. Why are rolled threads preferred over cut threads on Ti-6Al-4V fasteners?
Thread cutting severs the continuous metallic grain flow lines of the titanium alloy, creating micro-notches at the thread root where stress concentration precipitates premature fatigue failure under cyclic loads. In contrast, precision thread rolling cold-works the root radius and plastically deforms the grain structure to follow the thread profile uninterrupted. Rolled threads on Ti-6Al-4V screws exhibit work-hardened root compressive stresses, enhancing fatigue endurance limits by 30% to 50% under dynamic stress.
3. What causes galling during titanium screw installation, and how do you prevent it?
Titanium naturally develops a thin, passive titanium dioxide (TiO₂) film. When two titanium surfaces (or titanium against stainless steel) slide together under heavy pre-load torque without lubrication, this oxide film shears off, exposing active metallic contacts that micro-friction-weld together—a failure mode known as thread galling or seizing.
To eliminate galling, apply a high-quality anti-seize lubricant formulated with molybdenum disulfide (MoS₂), nickel, or PTFE paste. Alternatively, request Yevzo's factory-applied anti-galling treatments, such as Type II sulfuric anodization, Physical Vapor Deposition (PVD), or Diamond-Like Carbon (DLC) hard thin films.
4. How does the thermal expansion and galvanic compatibility of Ti-6Al-4V match with carbon fiber composites (CFRP)?
Aluminum and conventional carbon steel fasteners encounter severe galvanic corrosion when in direct contact with carbon fiber reinforced polymers (CFRP) because carbon behaves as a noble cathodic element, accelerating anodic breakdown in adjacent metals. Ti-6Al-4V has a close electrochemical potential to carbon (-0.05 to +0.06 V), making it virtually immune to galvanic corrosion in CFRP joints.
Furthermore, its thermal expansion coefficient (8.6 × 10⁻⁶/K) closely matches carbon composites much better than aluminum (23 × 10⁻⁶/K), preventing joint loosening under thermal expansion and contraction.
5. What quality certifications and inspection documentation does Yevzo provide?
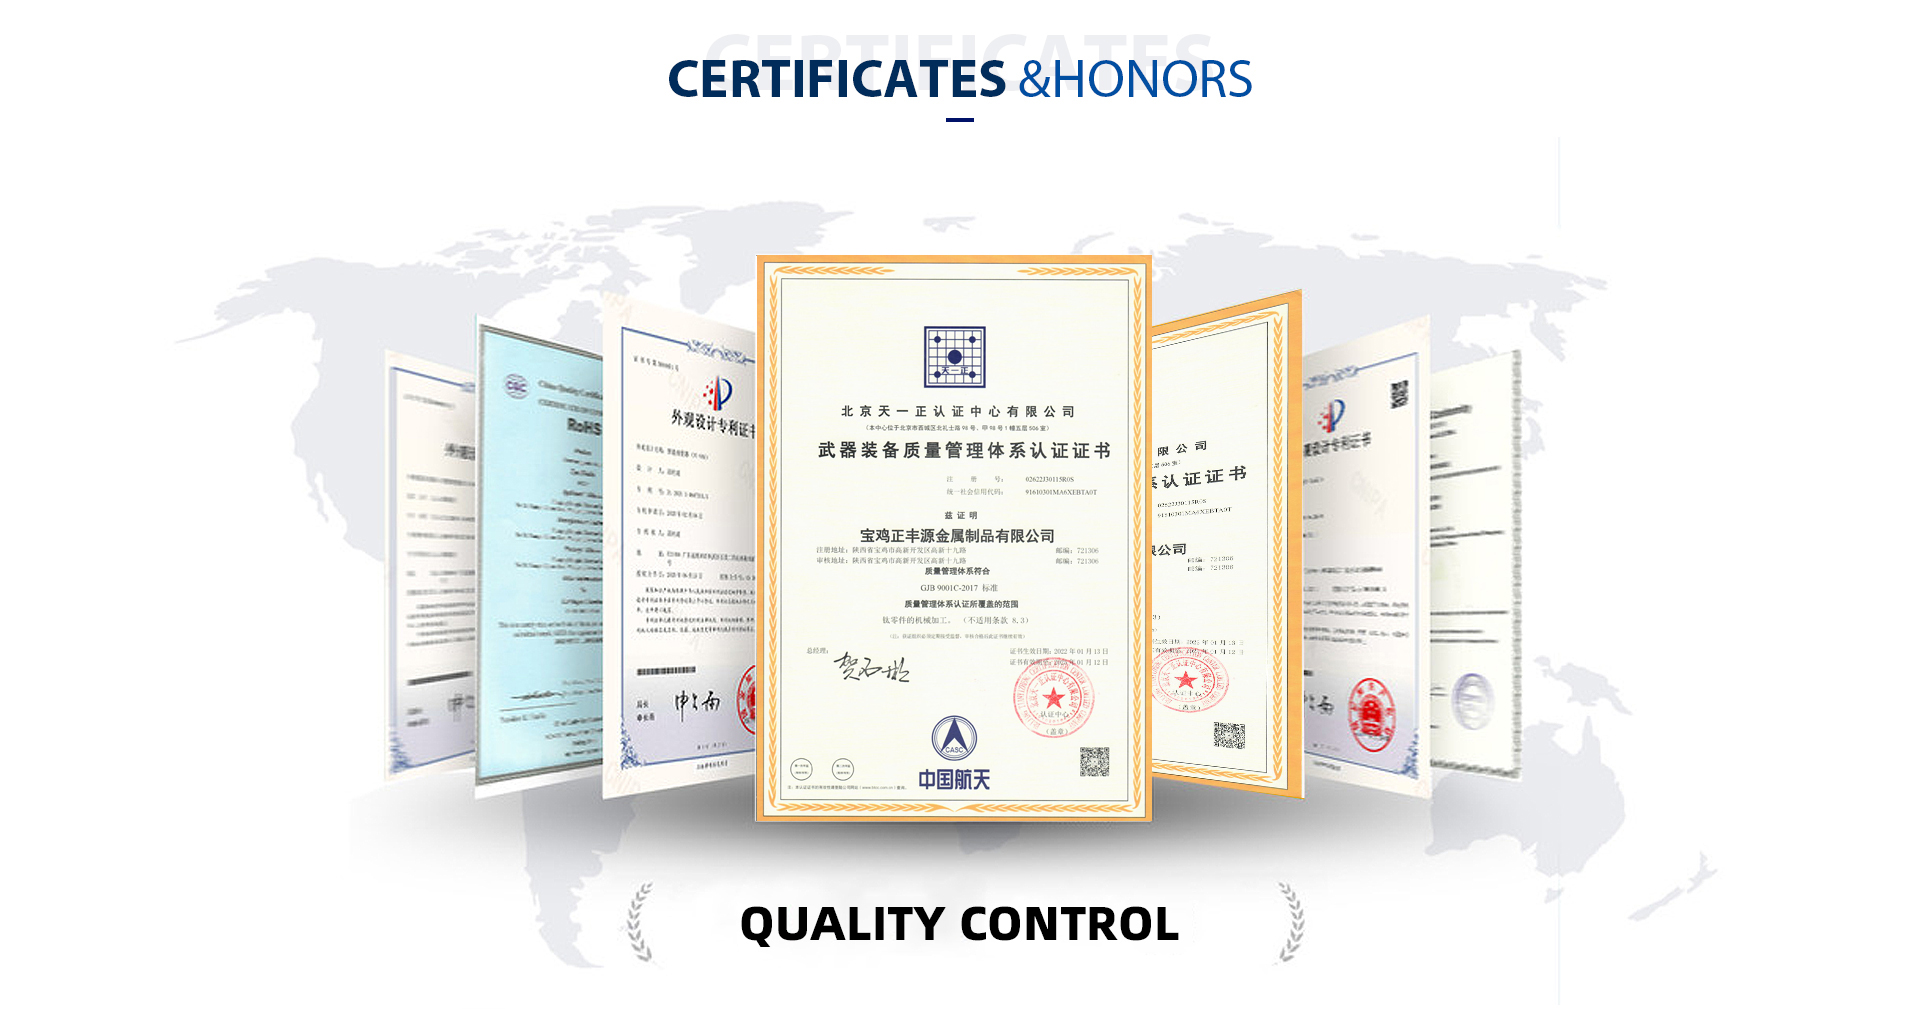
Every commercial and custom manufacturing shipment from Yevzo Titanium Metal Co., Ltd. comes with comprehensive EN 10204 3.1 Certified Material Test Reports (CMTR). Our documentation details exact chemical compositions (Al, V, Fe, C, N, H, O content) verified by optical emission spectrometry, mechanical tensile and yield tests, elongation percentages, hardness profiles (Rockwell C), and optical micro-comparative thread tolerance inspection sheets.
6. What are the standard lead times, MOQs, and Incoterms for international procurement?
For standard catalogue M3–M20 DIN and ISO hex, flange, and socket screws, the typical MOQ is 20 to 100 pieces per size, with immediate stock availability for rapid dispatch within 3–5 working days. For custom OEM/ODM drawing orders, prototypes require 10–15 days, and production batches require 20–30 days. We accept EXW, FOB, CFR, CIF, and full DDP door-to-door delivery with customs cleared, supported by secure international wire transfers (T/T), L/C, or online escrow.
Request an Engineering Consultation & Fast Factory Quote
Whether you require standard DIN/ISO Grade 5 stock fasteners or tailored OEM titanium CNC components manufactured to custom prints, the metallurgy and machining engineers at Yevzo Titanium Metal Co., Ltd. are ready to assist. Provide your specs for swift pricing and lead-time schedules.
Procurement Data Checklist
- 2D prints (PDF, DWG) or 3D geometry files (STEP, IGES)
- Material verification: Grade 5 Ti-6Al-4V / ASTM B348 / AMS 4928
- Surface finish: Plain, micro-polished, anodized, or PVD coated
- Estimated production quantity & designated delivery destination