Featured Titanium Fasteners & Motorsport Wheel Hardware
Precision-machined from certified vacuum-melted Ti-6Al-4V (Grade 5) titanium. Built to withstand punishing cyclic torque, high brake-rotor heat transfer, and aggressive speedway vibrations.
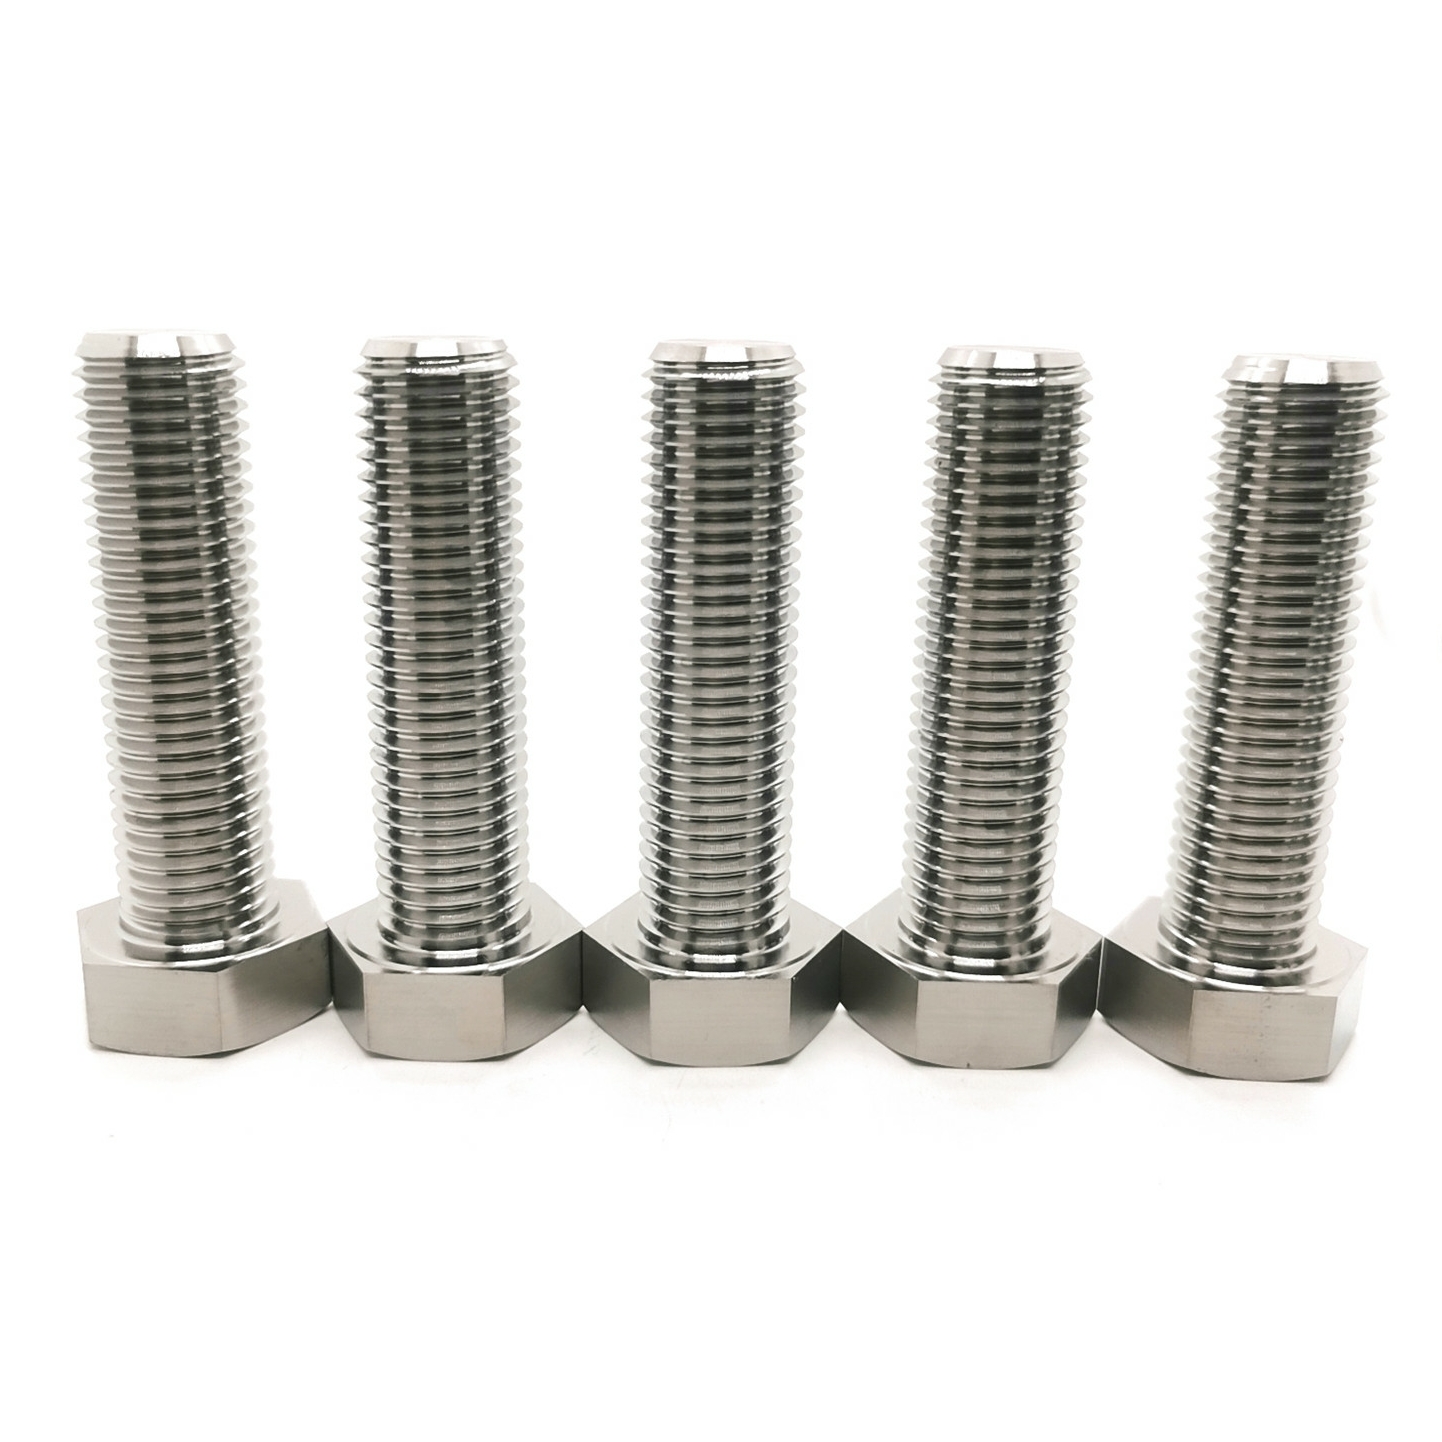
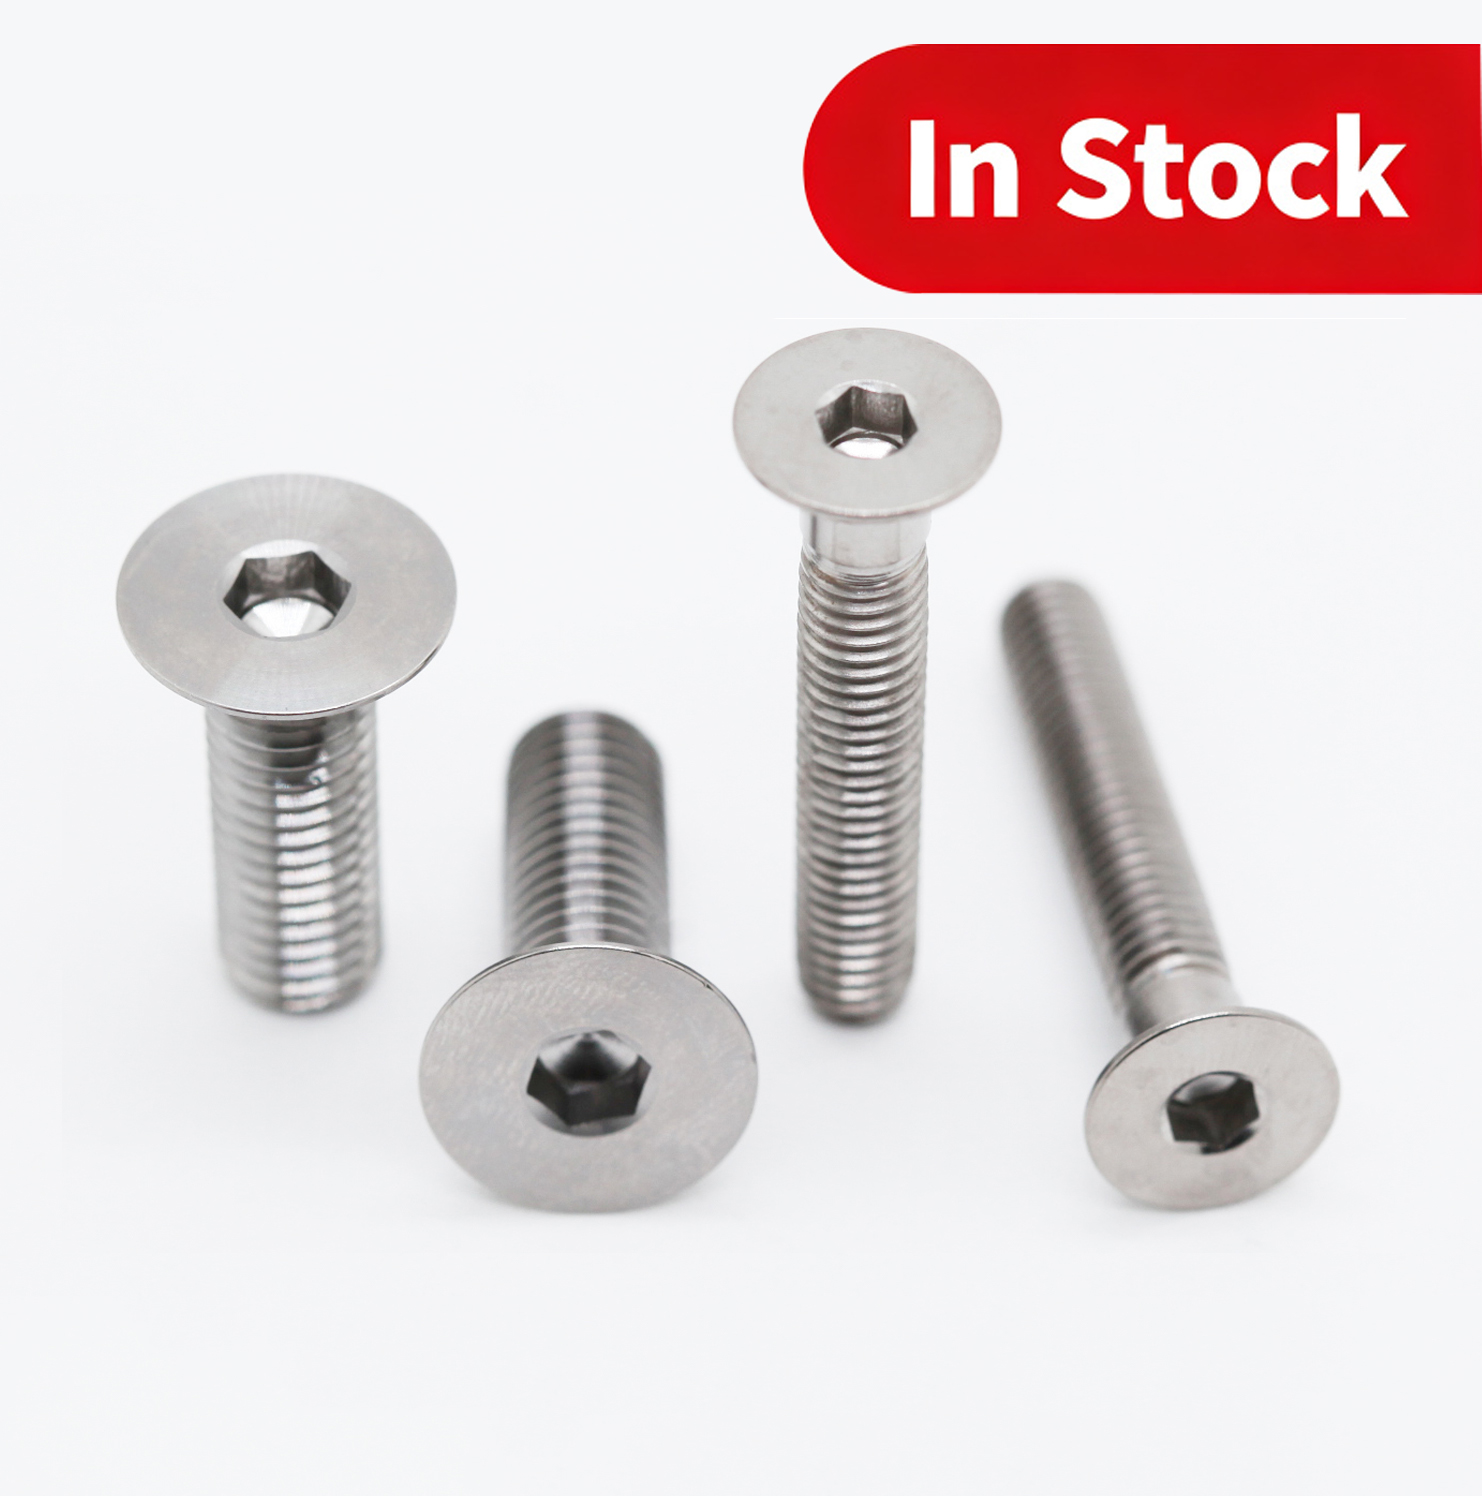
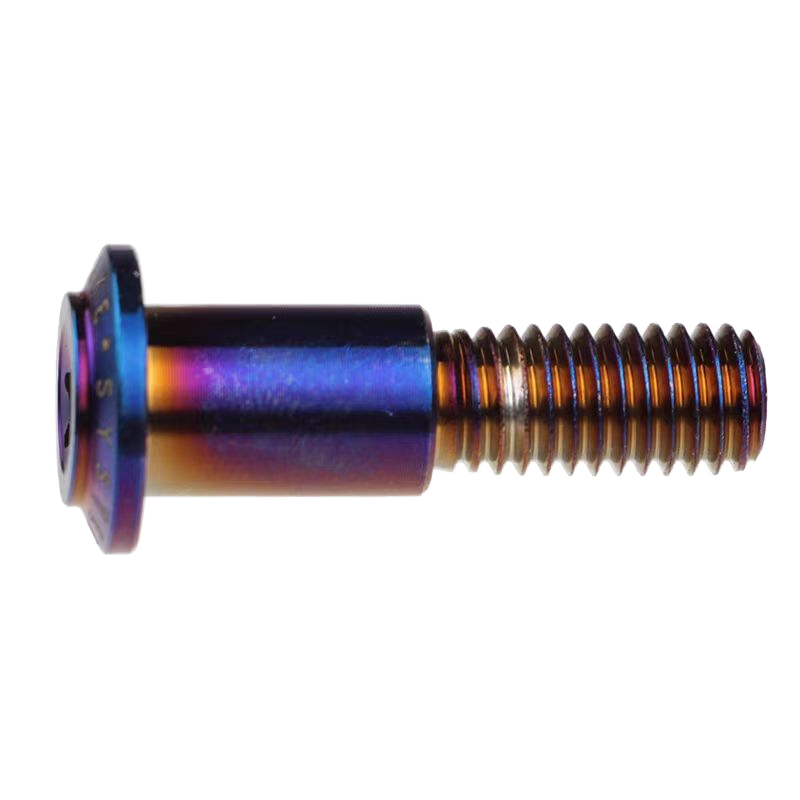
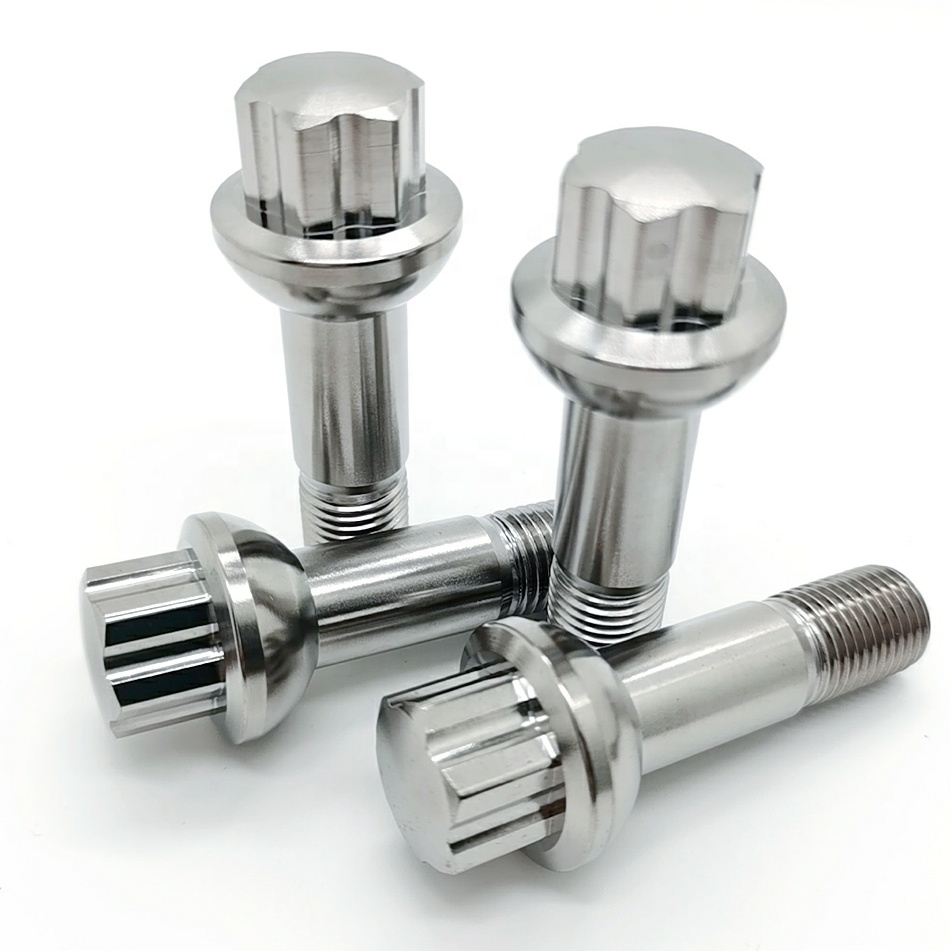
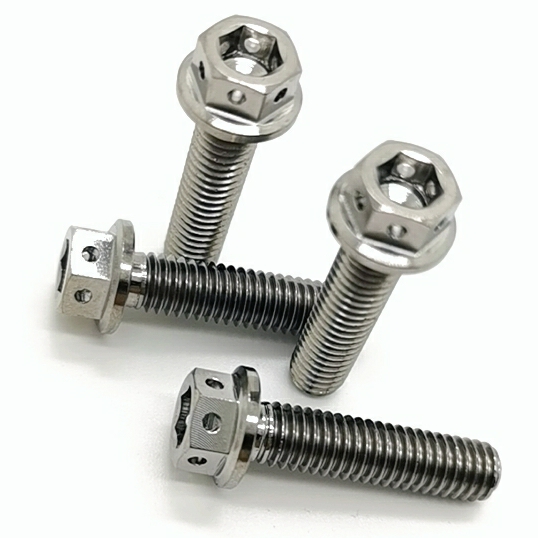
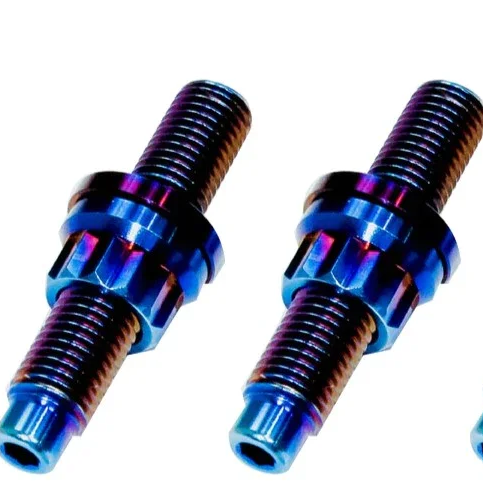
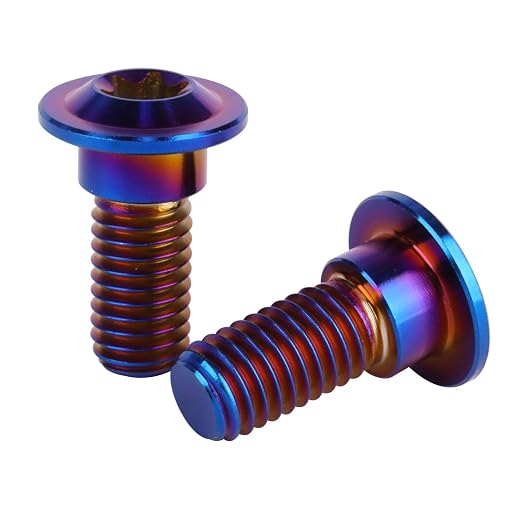
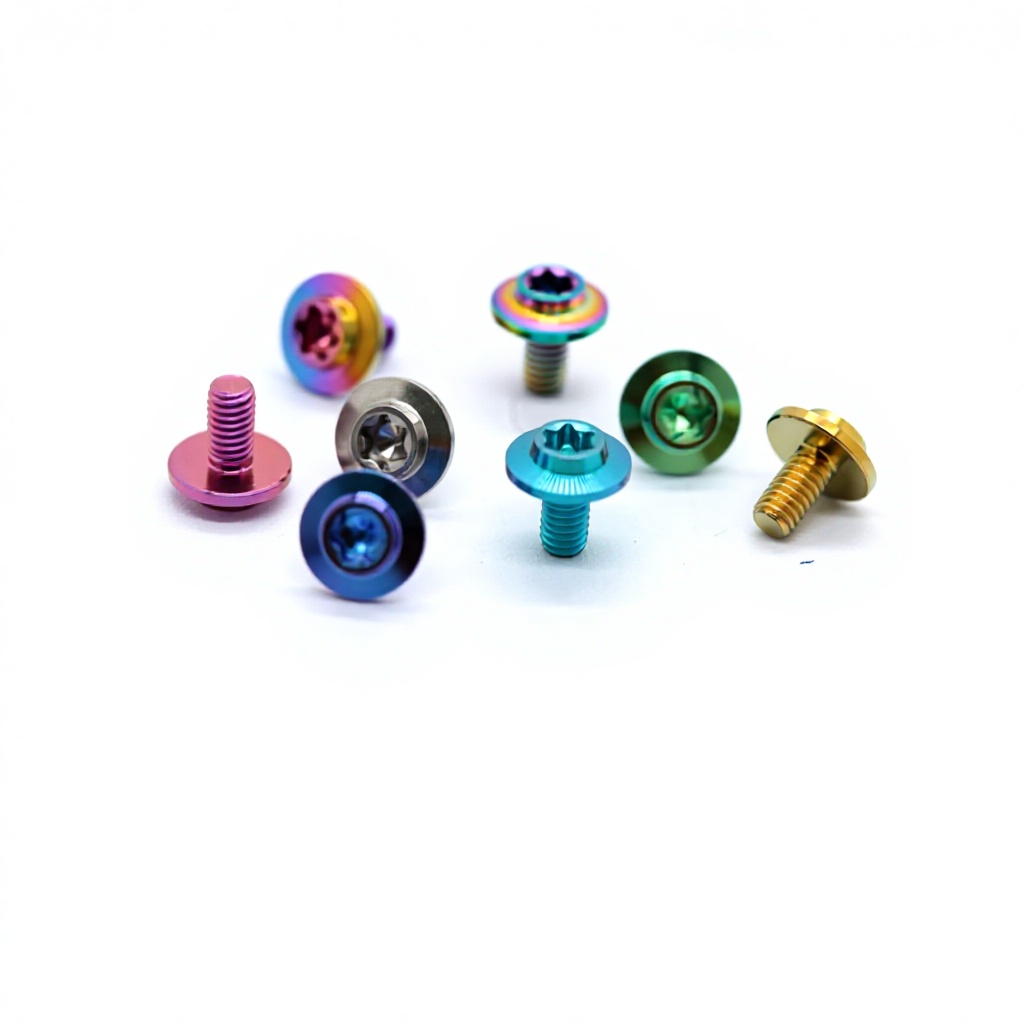
Mission-Critical Applications Across Central Indiana's Automotive Hub
Indianapolis is the epicenter of world motorsport engineering. From Speedway racing garages along Georgetown Road to precision tier-1 fabrication centers in Plainfield, Brownsburg, and Columbus, fastening integrity dictates dynamic survival.
In high-speed competition—from NTT IndyCar chassis setups to USAC sprint cars and endurance sports cars—wheel studs endure severe transient shear spikes and elevated wheel-hub thermal conditions exceeding 500°F (260°C) conducted directly from cross-drilled carbon-ceramic and slotted iron braking packages. Standard Grade 10.9 steel wheel studs, while mechanically tough, suffer from rotating unsprung mass penalties and progressive surface micro-pitting caused by salt spray, tire-prep chemicals, and continuous track washdowns.
Yevzo manufactures titanium wheel studs engineered specifically for this demand profile. Using aerospace-spec ASTM B348 Grade 5 rod processed at our dedicated source mills, our wheel studs undergo continuous thread rolling after thermal treating. Unlike cut threads that sever titanium grain boundaries, rolled threads compress the crystalline lattice, elevating thread shear strength, reducing galling susceptibility, and guaranteeing clean lug engagement during sub-3-second pit stop tire swaps.
Speedway & Oval Competition
Engineered for Indy oval sustainment where continuous 220+ MPH G-loads create lateral deflection. Our studs provide high elasticity with 828 MPa yield strength, flexing predictably without permanent elongation.
NHRA Pro & Lucas Oil Drag Racing
Drag programs based in Brownsburg demand ultimate torque shock resistance at the launch pad. Our rolled threads resist thread stripping under instant multi-thousand foot-pound rotational launches.
EV & High-Output Tuning Centers
Modern performance EVs demand massive load-bearing hub hardware to counter dual-motor instantaneous torque. Titanium stud conversions save approximately 2.5 to 3.8 lbs per vehicle in rotating unsprung mass.
Engineering Benchmark: Titanium Gr5 vs. High-Tensile Steel
Direct comparative test data measuring mechanical parameters vital for track engineers, chassis designers, and parts directors.
| Performance Metric | Ti-6Al-4V Grade 5 (Yevzo) | Grade 10.9 Chromoly Steel | 6061-T6 Aluminum (Stud Caps) | Motorsport Advantage |
|---|---|---|---|---|
| Ultimate Tensile Strength | 950 - 1050 MPa | 1040 MPa | 310 MPa | Matches 10.9 Steel Integrity |
| Yield Strength (0.2% Offset) | 880 - 920 MPa | 940 MPa | 276 MPa | High elastic return under heat |
| Material Density (g/cm³) | 4.43 g/cm³ | 7.85 g/cm³ | 2.70 g/cm³ | 43.6% Weight Reduction |
| Modulus of Elasticity (GPa) | 114 GPa | 210 GPa | 69 GPa | Superior damping of hub vibration |
| Thermal Expansion (10⁻⁶/K) | 8.6 | 12.2 | 23.2 | Maintains clamping torque when hot |
| Corrosion & Galling Resistance | Impervious (Self-Passivating) | Rusts without zinc/nickel | Oxidizes rapidly with iron | Zero track chemical oxidation |
Emerging Sourcing Trends Across the Indiana Motorsports Corridor
How changing technical regulations, supply-chain localization, and lightweighting mandates are reshaping fastener procurement in Region 7 and across the American Midwest.
Direct-from-Source Factory Integration
Midwestern speed shops and chassis fabricators are moving away from multi-tier white-label distributors. Direct collaboration with Yevzo's Baoji Titanium Valley factory eliminates domestic distributor markups (often 40-60%) while offering direct OEM dimensional customization.
PVD Micro-Coatings & Anti-Galling
Galling was historically a hurdle for titanium threads. The 2024-2026 technical trend across Speedway engineering facilities emphasizes specialized PVD (Physical Vapor Deposition) DLC and titanium nitride coatings, ensuring frictionless nut threading without compromising baseline metallurgy.
Wheel Conversion: Lug Bolt to Stud
European racing platforms (Porsche GT3 Cup, BMW M2 CS, Audi TCR) competing at Indianapolis Motor Speedway road courses are converting from OEM wheel bolts to press-in/screw-in titanium studs. This drastically cuts pit-lane change times and prevents cross-threading into expensive hub hubs.
Why Indianapolis Performance Engineers Trust Yevzo Fasteners
Yevzo Titanium Metal Co., Ltd. operates in the Honeycomb Industrial Park within Baoji’s High-Tech Development Zone—the global manufacturing nucleus for non-ferrous metal refinement. Our proximity to certified sponge reduction facilities guarantees uncompromising heat-lot purity for every wheel stud run.
- 100% Aerospace Grade 5 Material: Sourced strictly per ASTM B348 / AMS 4928 standards, never secondary alloy remelts.
- Precision Thread Rolling Technology: Continuous fiber flow threads engineered to resist cyclic fatigue, rated Class 6g fit.
- Full Traceability & MTRs: Every production batch is delivered with full Chemical & Mechanical Mill Test Reports (MTR).
- Custom OEM & Racing Dimensions: Fast turnaround on bullet-nose studs, custom knurl diameters, and custom lengths from 45mm to 95mm.
Spectrometry Verification
In-house PMI testing ensures chemical composition complies with Ti-6Al-4V requirements.
CNC Lathe Turning
Multi-axis precision CNC turning holds stud shank diameter and bullet-nose concentricity to ±0.005mm.
Thread Rolling
Cold thread rolling compresses grain structure, ensuring extreme fatigue strength under high torque.
Anodizing / PVD
Optional electrochemical oxidation or DLC coatings applied to provide desired aesthetics and surface wear resistance.
Frequently Asked Questions by Indianapolis Buyers
Clear answers addressing torque specifications, thread-engagement mechanics, anti-seize protocols, and commercial logistics.
Titanium has a lower modulus of elasticity (114 GPa vs. 210 GPa for steel), meaning it stretches more elastically under initial clamp load. We recommend torque values equal to or approximately 5-8% higher than Grade 10.9 factory specifications when installed with proper molybdenum disulfide or titanium-rated anti-seize. Always torque dry threads only when explicitly instructed by vehicle engineering guidelines.
Galling occurs when friction breaks down microscopic oxide layers, causing friction weld transfer. We prevent this by precision roll-polishing our threads to an Ra < 0.4 surface finish. For race teams, pairing our studs with our coated titanium open-ended lug nuts or quality hard-anodized 7075-T6 aluminum lug nuts, combined with copper-free synthetic anti-seize, delivers flawless long-term service.
Yes. We specialize in custom OEM engineering. We machine press-in knurl dimensions tailored exactly to your hub's bore tolerance (e.g., 0.565" to 0.625" knurl variants for aftermarket racing hubs), as well as screw-in studs with M12x1.25, M12x1.5, M14x1.25, or M14x1.5 transitions and extended bullet noses for rapid wheel locating.
Standard catalog sizes are stocked for rapid shipment. Custom CNC manufacturing batches typically require 12 to 18 business days. We offer direct-to-door express delivery (air express via DHL/FedEx) arriving in Indianapolis within 4–6 business days, as well as sea freight DDP shipping for volume wholesale consignments.
Ti-6Al-4V retains substantial mechanical integrity at elevated temperatures up to 750°F (400°C), well beyond the operational transfer temperature of wheel hubs during continuous endurance race braking. Additionally, titanium has lower thermal conductivity than steel, acting as a thermal buffer that slows heat transfer into wheel bearings and hub seals.
For stocked motorsport hardware and wheel stud kits, our MOQ starts at just 20 pieces (accommodating single-vehicle setups). For full custom CNC knurl machining or custom PVD rainbow/burnt titanium coatings, custom run MOQs generally start at 100 to 200 pieces with complete volume pricing breaks.
Partner with a Direct Titanium Fastener Factory
Whether you are outfitting a racing team for the upcoming season, upgrading an aftermarket brand portfolio, or requiring custom CNC wheel studs for high-performance builds, our engineering desk is ready to review your CAD files and spec sheets.