Flagship Titanium Racing Fasteners & Hardware Series
Precision-engineered Grade 5 (Ti-6Al-4V) components designed for extreme shear stress, high-rpm vibrational loads, and corrosive motorsport track conditions. Fully compliant with DIN, ISO, and bespoke OEM motorsport blueprints.
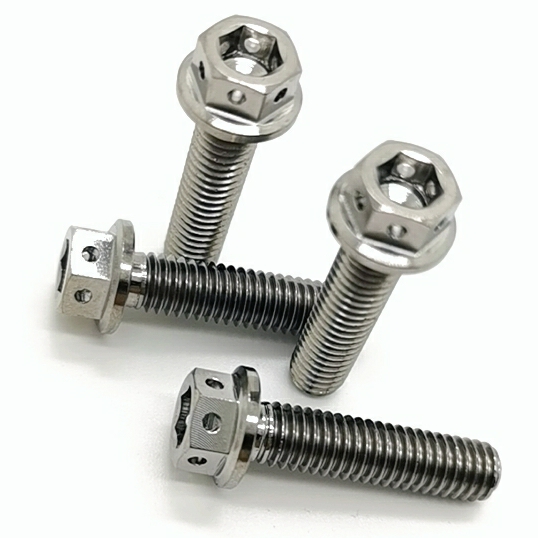
GR5 Titanium Socket Head Plain Finish Bolt & Nut Assembly
- Grade: Ti-6Al-4V (Grade 5)
- Tensile Strength: 950–1050 MPa
- Thread Spec: M3 to M24 Rolled Threads
- Application: Chassis & Engine Block Mounts
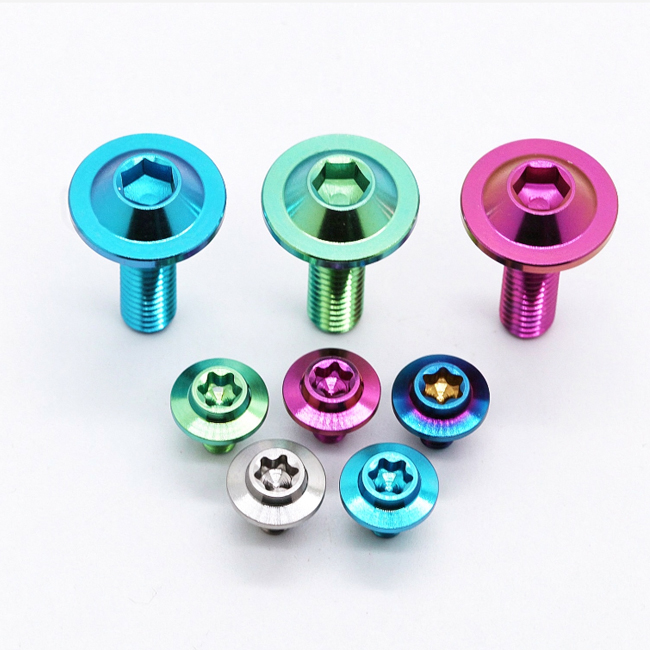
Anodized Rainbow GR5 Titanium Flange Head Allen Racing Bolt
- Grade: Ti-6Al-4V Alpha-Beta
- Surface: Physical Vapor Deposition (PVD)
- Design: Flanged Wide Surface Seating
- Application: Motorcycle Fairing & Caliper
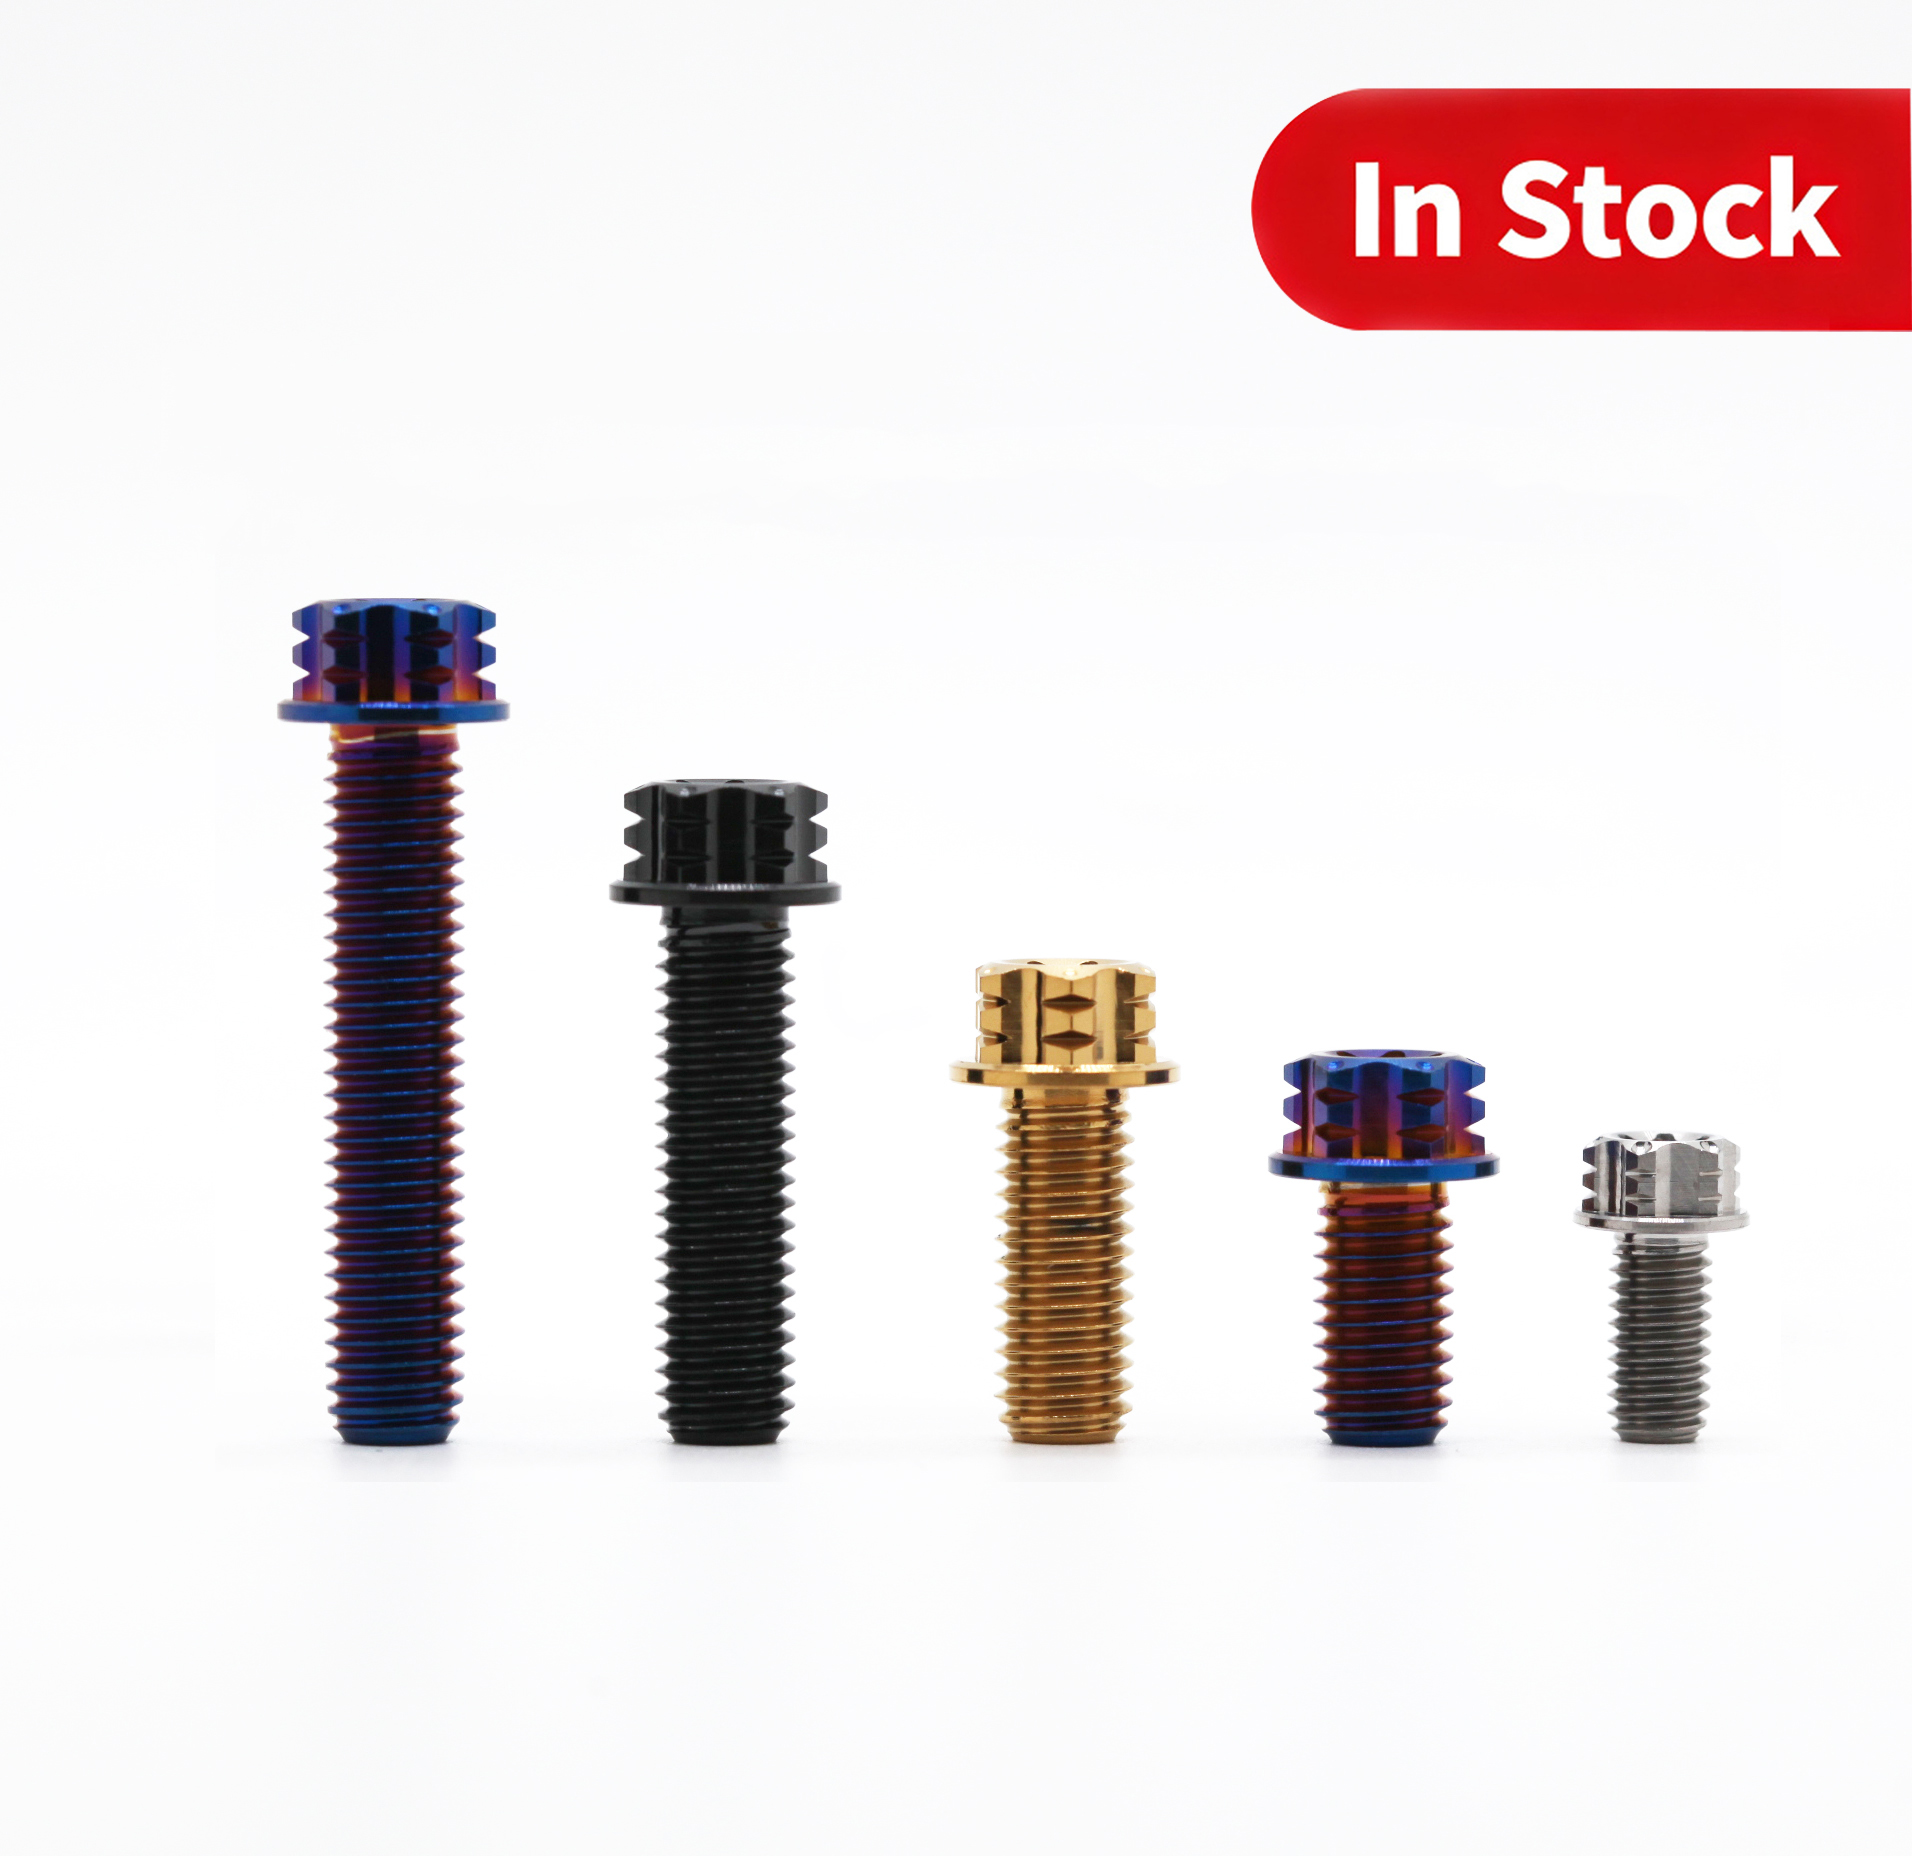
Gr5 Ti-6Al-4V High-Torque Motorcycle Flange Bolts (M6–M22)
- Shear Strength: >550 MPa
- Colorways: Burnt Blue / Gold / Violet / Raw
- Flange Spec: Integrated Serrated / Smooth
- Application: Sprocket & Brake Rotor Hubs
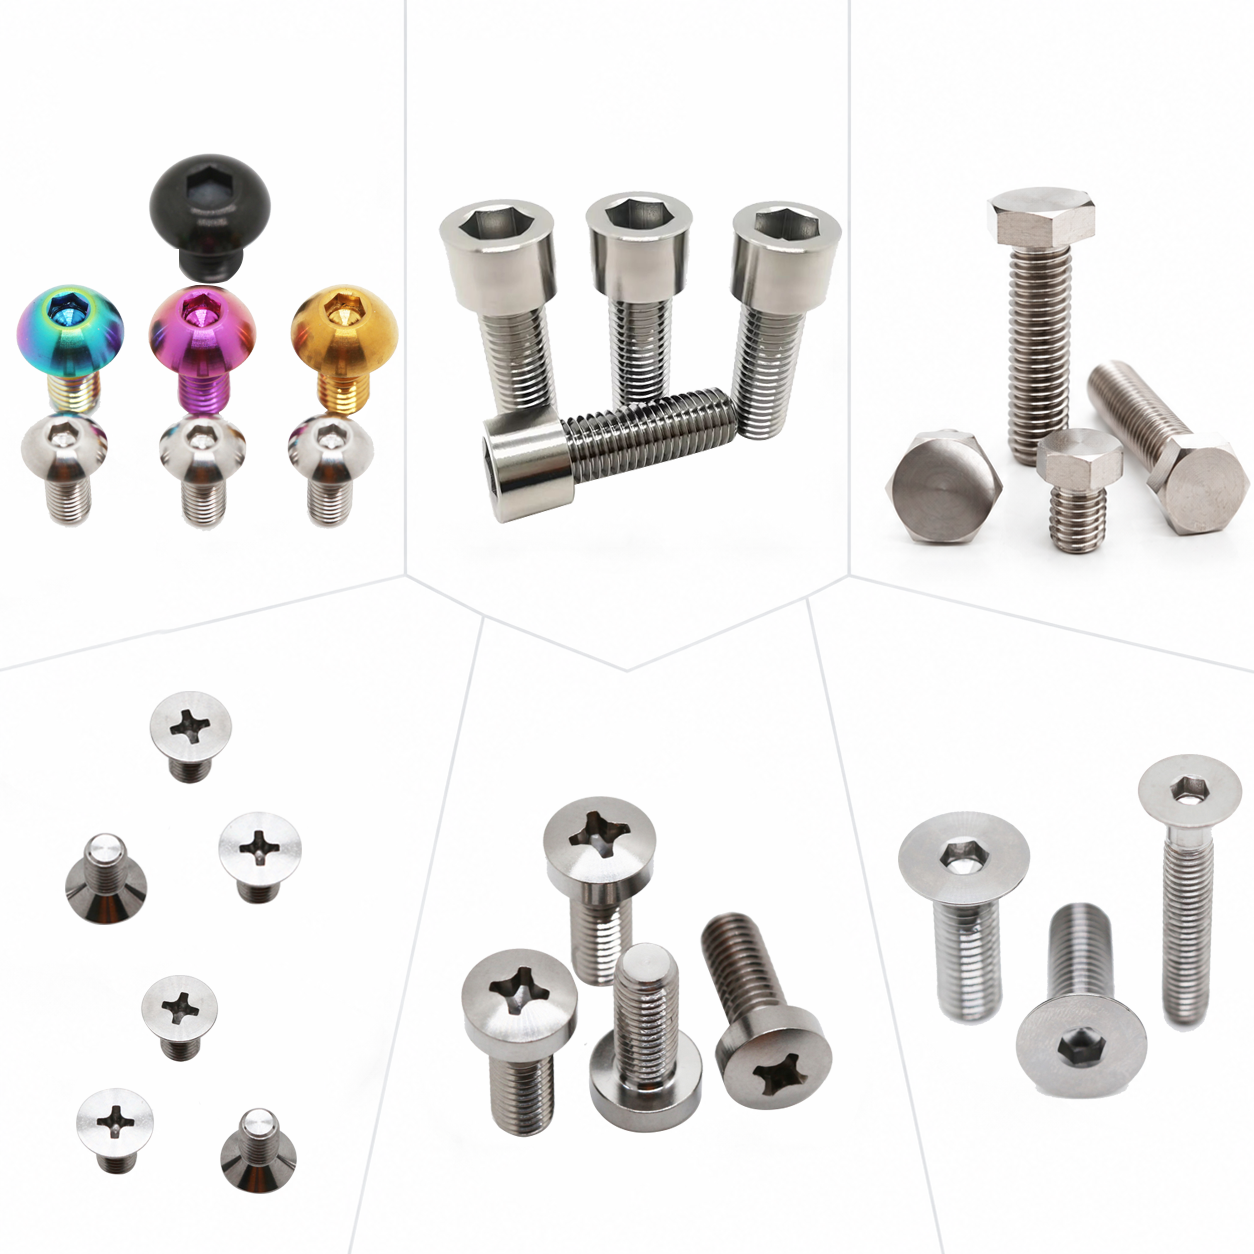
GR5 Titanium Fastener Bolts & Nuts Track Maintenance Kit
- Standard: ISO 4014 / 4017 / DIN 6921
- Thread Engagement: Rolled 6g Tolerance Fit
- Hardness: HRC 32–38 Heat Treated
- Application: Paddock Spares & Suspension Links
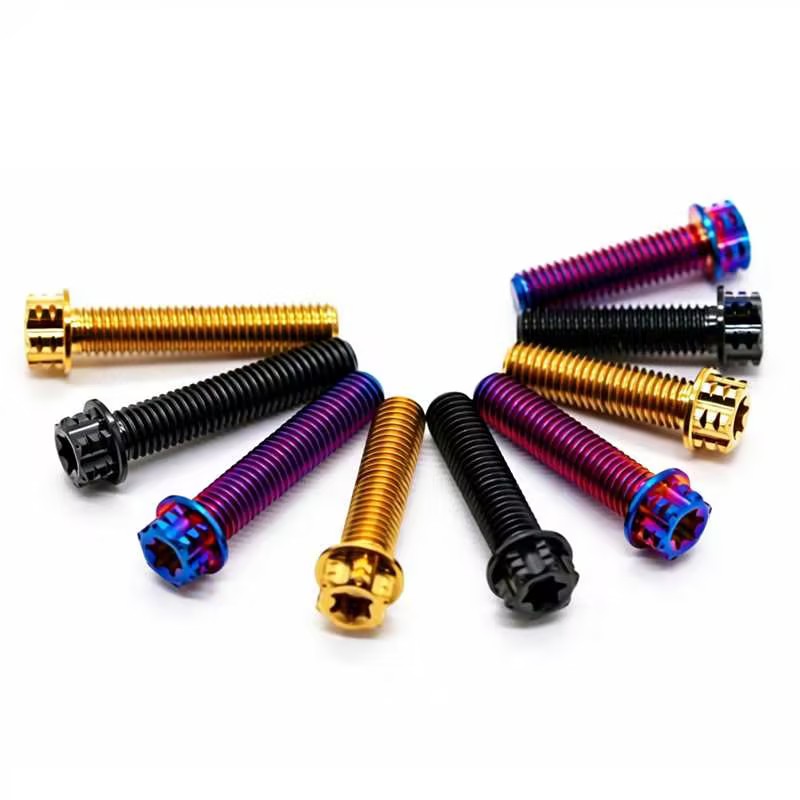
Titanium Torx (Star Drive) High-Torque Motorcycle Bolt
- Drive Profile: Precision CNC Torx T25–T50
- Coating: Hard PVD Titanium Nitride
- Anti-Camout: High Engagement Angle
- Application: High-Vibration Disc Assemblies
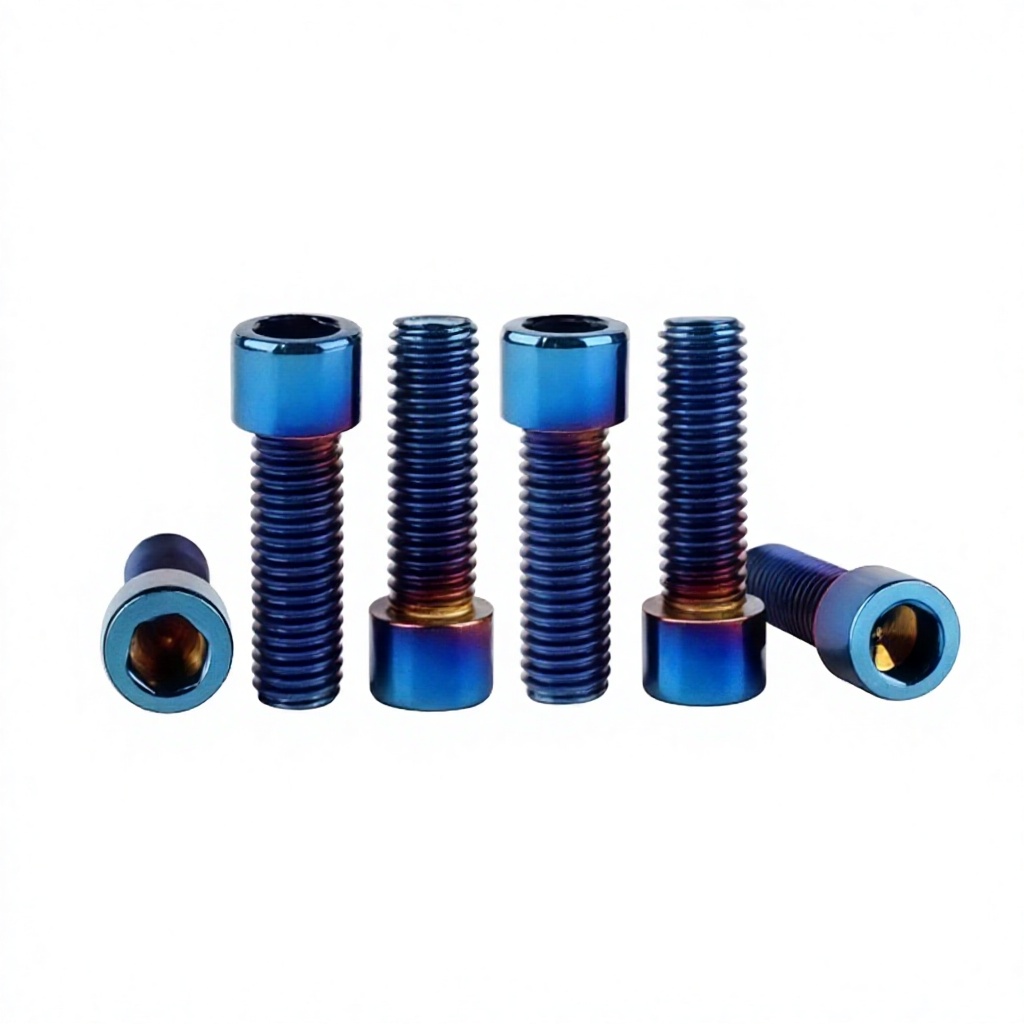
Flush Countersunk Flat Head Titanium Fasteners (M1.6–M8)
- Head Profile: 90° DIN 7991 Flat Countersunk
- Aerodynamics: 100% Flush Body Integration
- Machining: Swiss-Type Lathe Ultra Precise
- Application: Aero Spoilers & Bicycle Controls
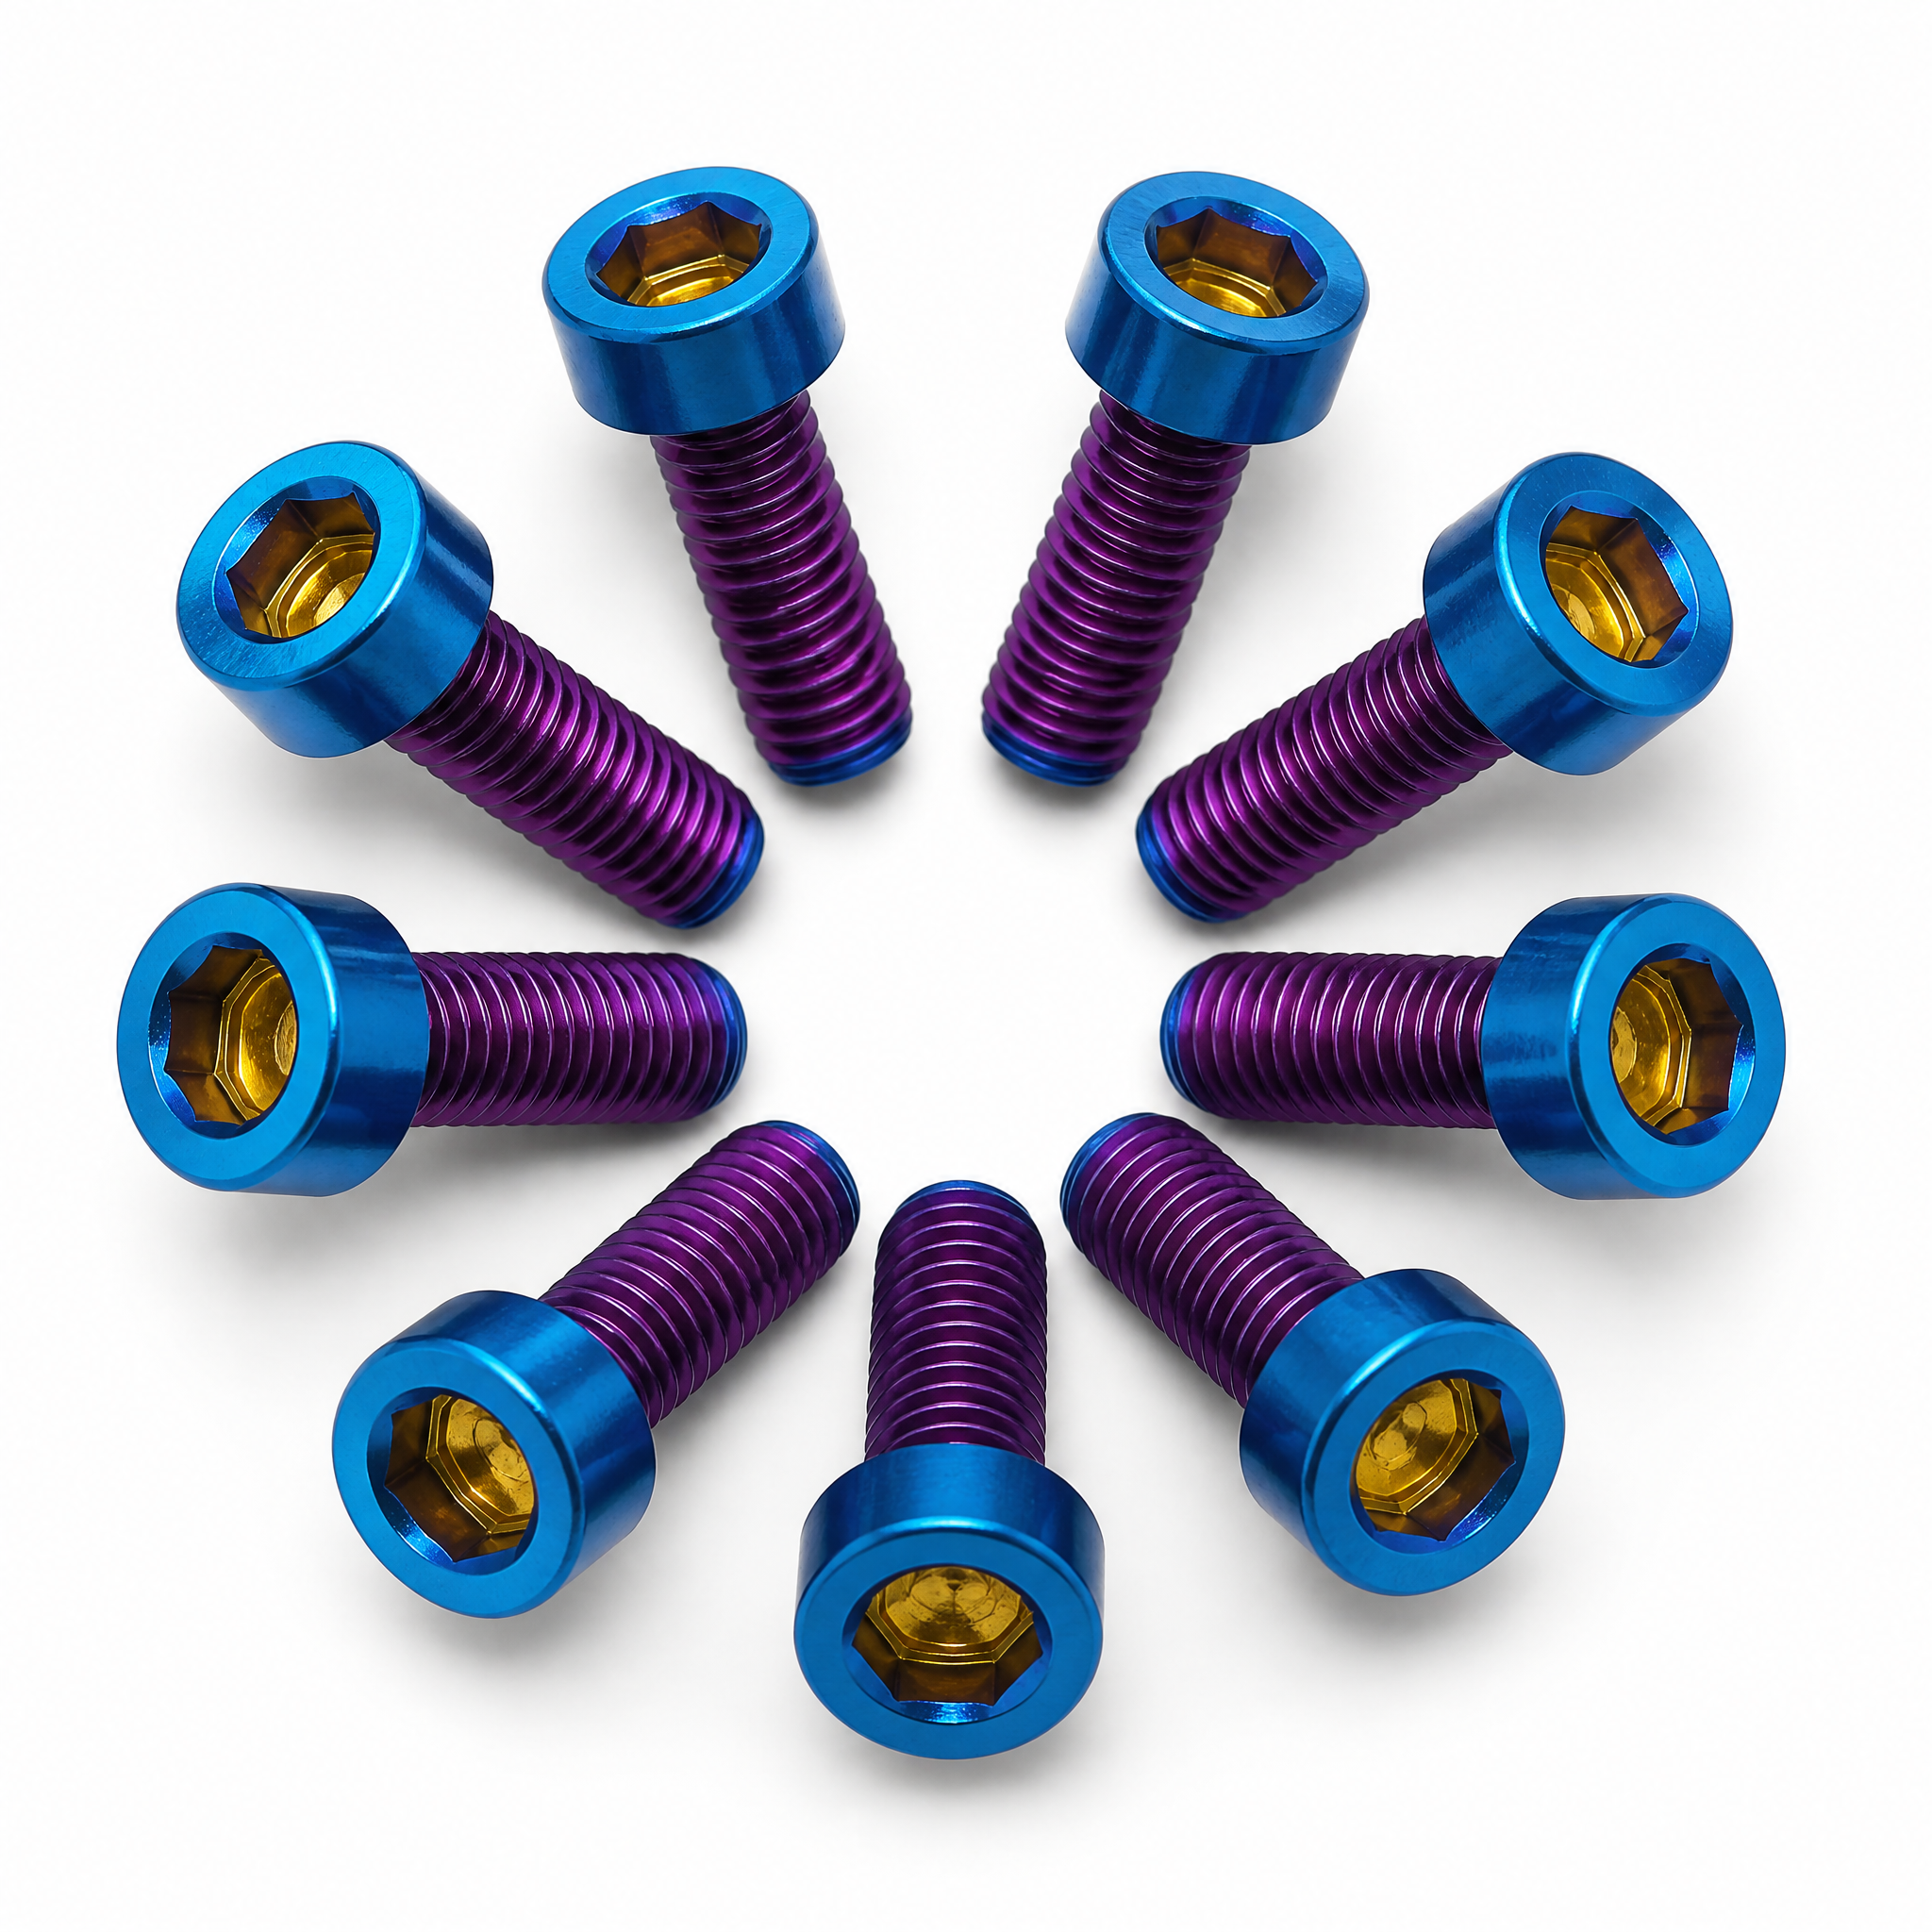
Colored Torx Shell & Bodywork Titanium Fasteners (M4–M6)
- Weight Index: 4.43 g/cm³ Pure Low Mass
- Anodization: Type II Electrochemical Oxide
- Head Diameter: Low Profile Spun Perimeter
- Application: Carbon Fiber Fairing Fastening
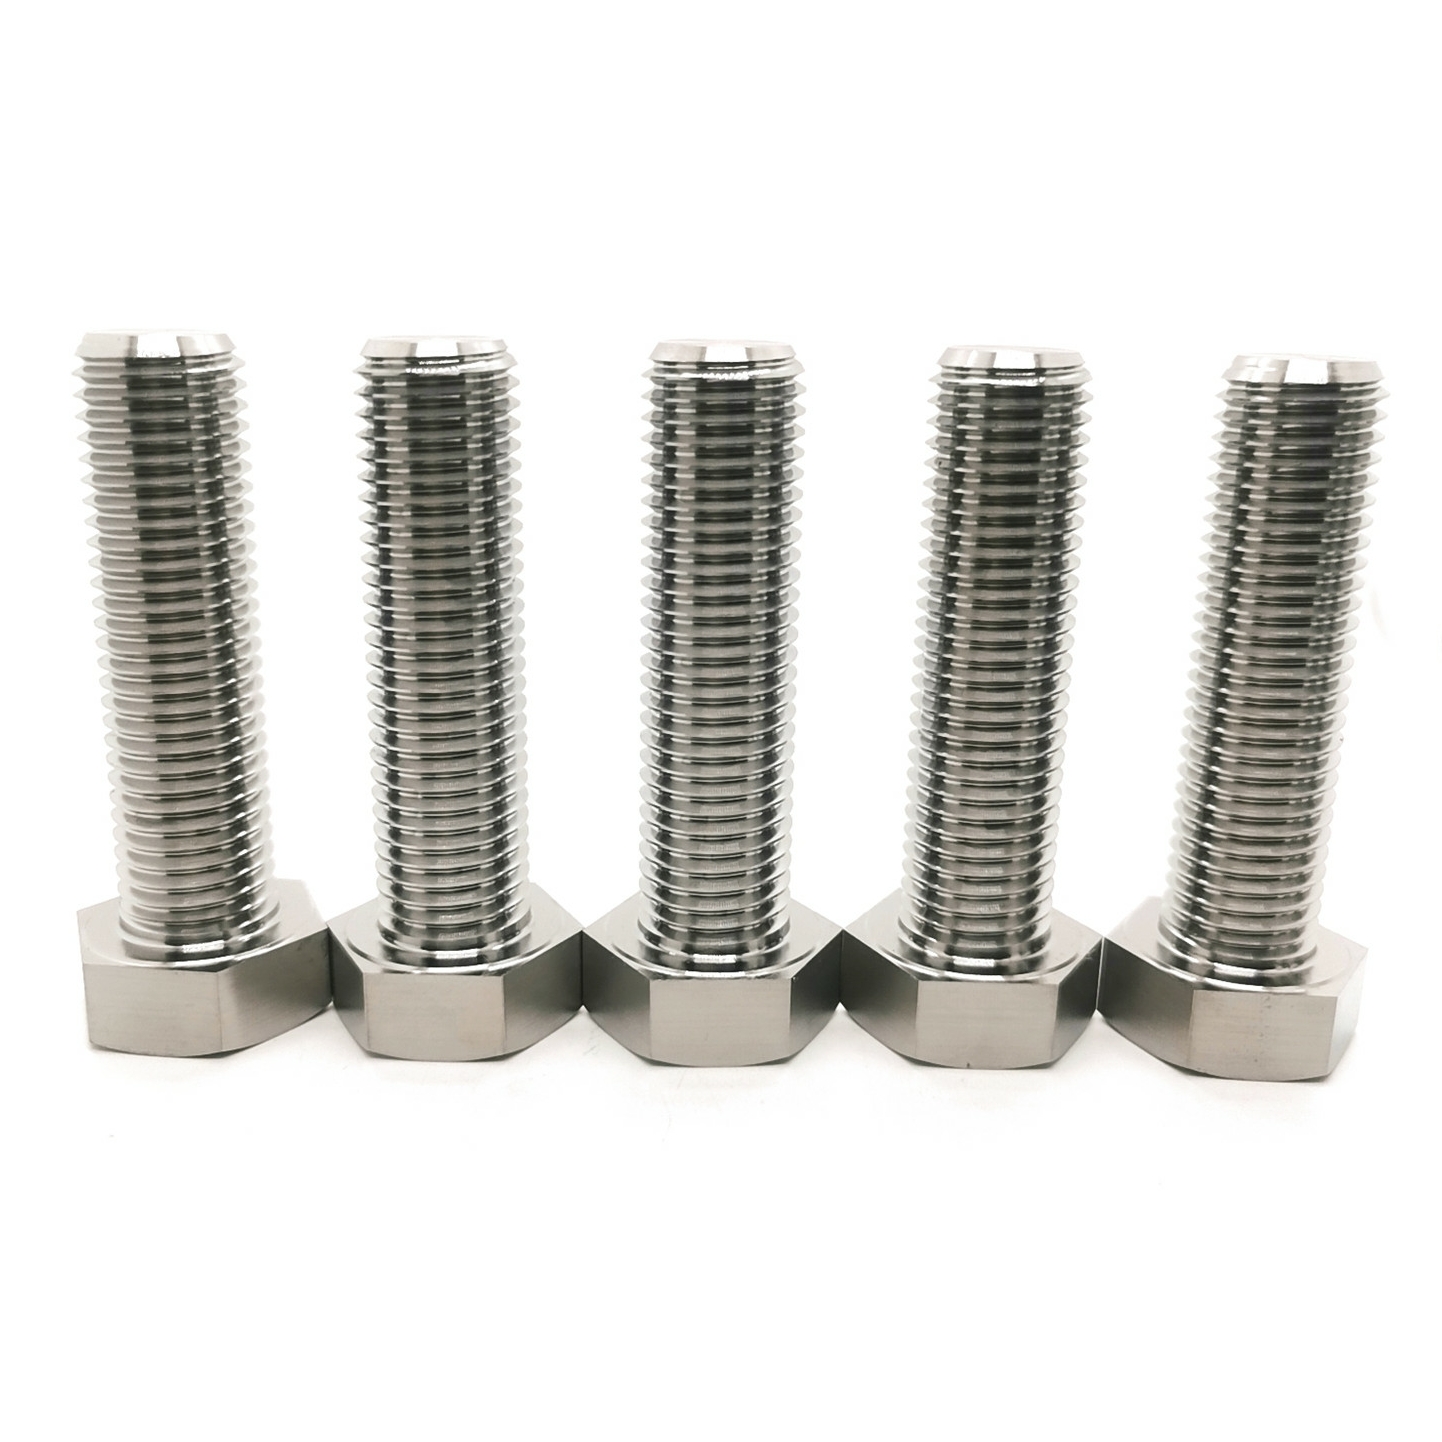
DIN912 Titanium Hexagon Socket Head Cap Screws (M0.8–M24)
- Proof Stress: 828 MPa Minimum
- Corrosion Shield: Passive TiO2 Natural Layer
- Threading: Fully Machined / Cold Forged
- Application: Suspension Knuckles & Calipers
Looking for Custom Titanium Racing Hardware Drawings?
From custom hollow-shank caliper bolts to drilled safety-wire hex flange bolts, our Baoji engineering unit provides Rapid CAD/CAM quotes within 24 hours.
The Global Titanium Racing Fasteners Manufacturing Ecosystem
In modern performance racing—spanning Formula 1, MotoGP, Superbike World Championship (WorldSBK), GT3 endurance racing, and hypercar engineering—the mechanical connection between critical subassemblies is the difference between podium success and catastrophic mechanical failure. High-tensile steel fasteners (such as ISO 898-1 Class 10.9 and 12.9) have traditionally shouldered cyclic fatigue loads, but at a punishing mass penalty. Aluminum 7075-T6 hardware is lightweight yet lacks the yield endurance and high-temperature integrity necessary for dynamic unsprung rotational assemblies.
This structural paradox has positioned Grade 5 Titanium (Ti-6Al-4V, UNS R56400, Werkstoff 3.7165) as the premier fastener alloy of choice. Balancing an extraordinary ultimate tensile strength exceeding 950 MPa with a low density of 4.43 g/cm³, titanium fasteners instantly eliminate approximately 44% of structural fastener mass while providing complete immunity to road-salt, moisture, and chemical oxidation.
Selecting an OEM supplier or bulk export partner requires deep technical scrutiny. A racing bolt cannot simply be machined from raw billet bar on an entry-level CNC lathe; it demands controlled microstructural metallurgy, hot/cold precision head forging, grain-flow thread rolling, and zero-defect non-destructive testing (NDT).
| Alloy & Condition | Yield Strength (MPa) | Tensile Strength (MPa) | Density (g/cm³) | Fatigue Runout (Cycles) | Corrosion Shield |
|---|---|---|---|---|---|
| Titanium Gr5 (Ti-6Al-4V Solution & Aged) | 880–920 | 960–1050 | 4.43 | > 10,000,000 (Rolled) | Inherent TiO2 Oxide Layer |
| Titanium Gr2 (Commercially Pure CP) | 275–350 | 345–480 | 4.51 | Moderate (~10^5) | Immune (Acid/Marine) |
| Alloy Steel Class 10.9 (Ref.) | 940 | 1040 | 7.85 | High (~10^7) | Requires Zn-Ni Plating |
| Alloy Steel Class 12.9 (Ref.) | 1100 | 1220 | 7.85 | Susceptible to Hydrogen | Requires Phosphate/Plate |
| Aircraft Aluminum 7075-T6 | 505 | 570 | 2.81 | Low Under High Shear | Prone to Galvanic Pitting |
Top 10 Global Titanium Racing Fasteners Manufacturers & Exporters
The global manufacturing ecosystem for titanium racing hardware is clustered within specialized aerospace corridors and metalworking hubs. Below is the authoritative industry evaluation of the top ten leading factories, technical exporters, and specialized racing bolt manufacturers serving global OEM, motorsport, and defense tiers:
1. Yevzo Titanium Metal (China)
Headquarters: Baoji Titanium Valley, Shaanxi.
Specialization: Fully integrated forging, rolled threading, and 5-axis CNC machining for motorcycle and automotive racing fasteners. Direct access to raw titanium ingots, 100+ precision turning centers, comprehensive ISO/ASTM compliance, and worldwide DDP/FOB distribution.
2. Lisi Aerospace (France)
Headquarters: Paris, France.
Specialization: World-renowned aerospace and Formula 1 structural fastener supplier. Pioneer in ultra-high-precision multi-alloy cold heading, high-reliability engine stud packs, and proprietary motorsport weight-reduction fastener geometry.
3. Pro-Bolt (United Kingdom)
Headquarters: Gloucestershire, England.
Specialization: Premium aftermarket motorcycle racing bolts, MotoGP and WorldSBK team fastener supplier. Excellent surface anodizing programs, pre-drilled safety-wire race heads, and specialized trackside kits.
4. ARP (Automotive Racing Products - USA)
Headquarters: Santa Paula, California, USA.
Specialization: Industry benchmark for engine cylinder head studs, rod bolts, and drivetrain fasteners. Precision heat-treating capabilities and specialized high-yield titanium racing line applications.
5. Poggipolini S.p.A. (Italy)
Headquarters: San Lazzaro di Savena, Italy.
Specialization: Elite tier-1 structural fastener designer for Formula 1 teams, MotoGP paddock, and Italian supercar marques. Unmatched focus on hot-forged structural titanium aerospace-grade fasteners.
6. Ti64 Racing Fasteners (Japan)
Headquarters: Shizuoka, Japan.
Specialization: Super GT and factory road-racing motorcycle hardware. Highly specialized in cold-formed Ti-6Al-4V high-precision wheel hub studs, rotor bolts, and proprietary low-friction dry lubricants.
7. Titanium Joe Inc. (USA / Canada)
Headquarters: Ontario, Canada & USA.
Specialization: Major supplier of raw aerospace titanium rod, bar stock, and custom race-team fastener manufacturing. Wide inventory coverage for custom one-off motorsport prototype builders.
8. Bulten AB (Sweden)
Headquarters: Gothenburg, Sweden.
Specialization: Full-service fastener engineering provider catering to European electric racing vehicle programs and lightweight high-volume performance automotive assemblers.
9. SPS Technologies (PCC Fasteners - USA)
Headquarters: Jenkintown, Pennsylvania, USA.
Specialization: Precision aerospace and high-temperature performance racing fasteners. Legendary MP35N, A286, and titanium alloy shear pin and wheel hub manufacturing.
10. Acer Titanium Racing (USA)
Headquarters: Los Angeles, California, USA.
Specialization: Lightweight niche motorsport solutions, off-road racing, and competition karting fasteners. Extensive inventory of high-purity Grade 5 titanium tapered socket caps and lightweight lock-nuts.
Rolled Threads vs. Cut Threads: The Critical Fatigue Life Differential
The single greatest determinant of whether a titanium bolt survives high-frequency track oscillation is the threading method. During thread cutting or single-point CNC threading, the cutting tool physically severs the grain structure of the Ti-6Al-4V bar. This creates microscopic stress risers and microscopic tearing at the thread root. Under cyclic tensile strain, micro-cracks originate at these root defects, causing rapid catastrophic fatigue failure.
In contrast, high-performance racing bolts utilize hot or cold thread rolling between hardened cylindrical dies. Thread rolling plastically deforms the titanium crystal lattice without cutting the fibers. The grain lines are forced to follow the exact contour of the crest and root radii. Furthermore, rolling induces beneficial compressive residual stresses on the surface layers. As confirmed in mechanical testing laboratories, thread-rolled titanium bolts display a 300% to 500% longer dynamic fatigue life compared to cut-thread equivalents.
Continuous Grain Flow
Rolling aligns titanium alloy grains organically along thread contours, completely preventing notch crack propagation.
Residual Compression
Compressive stresses engineered into the root valley neutralize cyclic tensile forces exerted during aggressive braking.
Surface Smoothness (Ra 0.2)
Burnished rolled finishes lower the friction coefficient, preventing galling during high-speed impact-gun wrenching.
Pitch Class 6g / 4h Fit
Extreme micrometer tolerances prevent thread play, bolt back-out, and harmonic micro-loosening under track rumble.
Future Procurement Trends in Motorsport Titanium Fasteners
As the international automotive industry shifts toward hybrid performance, ultra-dense battery electric platforms (EVs), and aerodynamic downforce limits, procurement strategies for titanium fasteners are experiencing structural evolutions:
1. Hollow-Shank and Additive-Subtractive Hybrid Fasteners
Motorsport engineering departments are no longer satisfied with standard solid shanks. Advanced machining setups integrate deep-hole gundrilling to produce hollow-shank bolts that eliminate up to 18% additional weight from the bolt core without compromising tensile or shear capabilities. For complex geometry brackets, direct metal laser sintering (DMLS) combined with secondary 5-axis CNC finish-threading is gaining adoption for small-batch hypercar development.
2. Transition to Ti-6Al-4V ELI (Grade 23) in Critical Crash Envelopes
Grade 23 (Extra Low Interstitial) titanium, traditionally reserved for aerospace cryogenic storage and surgical implants, is making rapid inroads into Formula racing cockpits and crash structures. By strictly limiting interstitial oxygen (≤ 0.13%) and iron, Grade 23 delivers significantly higher fracture toughness and impact energy absorption at sub-zero or ultra-high thermal extremes.
3. Physical Vapor Deposition (PVD) Diamond-Like Carbon (DLC) Coatings
While electrochemical color anodizing remains popular for paddock branding, top-tier racing teams specify DLC (Diamond-Like Carbon) and TiAlN (Titanium Aluminum Nitride) PVD coatings. These coatings introduce an ultra-hard surface layer (over 2,500 HV) with a dry friction coefficient below 0.12. This eliminates the risk of thread galling and permits repeated disassembly with pneumatic impact tools without anti-seize paste re-application.
4. Digital Heat-Lot Passports and Blockchain Verification
Counterfeit metal stock represents an existential risk to racing teams. Tier-1 exporters now ship every batch with QR-linked Digital Material Passports containing optical emission spectrometry (OES) chemical analysis, tensile pull curves, and ultrasonic immersion inspection records traceable directly back to the primary vacuum arc remelting (VAR) titanium ingot melt.
The Baoji Titanium Valley Manufacturing Advantage: Yevzo Titanium
Based in the High-Tech Development Zone of Baoji, Shaanxi—globally recognized as China’s "Titanium Valley"—Yevzo Titanium Metal Co., Ltd. exemplifies the modern integrated supply-chain model. Baoji houses over 60% of China’s national titanium processing capacity, allowing immediate access to raw sponge, triple-melt ingots, and ASTM B348 certified round bar stock.
Operating continuously since 2013, our production infrastructure combines heavy forging presses, 3-axis to 5-axis CNC machining suites, dedicated thread-rolling centers, and automated optical laser inspection systems. Key operational strengths include:
- Certified Raw Ingot Sourcing: Full chemical lot control adhering strictly to ASTM B348, ASTM F136, AMS 4928, and ISO 5832 standards with zero scrap blending.
- Comprehensive Thread Range: Full metric pitch coverage (M1.6 to M36), imperial UNC/UNF standard specifications, and bespoke custom pitch racing threads.
- Complete In-House Surface Engineering: Precision automated polishing, multi-spectral electrochemical anodizing (gold, violet, green, burnt rainbow, cyan), and advanced PVD ceramic hard coatings.
- Low MOQ & Rapid Rapid Prototyping: Catalogue standard fasteners available from 20–30 piece increments, with custom blueprint prototypes machined and shipped within 5 to 7 business days.
- Flexible Global Trade Architecture: Comprehensive Incoterms support (FOB, CIF, FCA, CPT, DDP, DDU, Express) accepting USD, EUR, GBP, JPY, and AUD via global escrow and international bank trade channels.
Frequently Asked Questions: Sourcing Titanium Racing Bolts
In-depth metallurgical and mechanical guidance curated by senior applications engineers to resolve common design, assembly, and sourcing uncertainties.
Why is Grade 5 (Ti-6Al-4V) mandatory over Grade 2 for racing bolts?
How do racing teams solve titanium thread galling and seizing?
What are the recommended torque values for titanium bolts compared to steel?
Does titanium cause galvanic corrosion when fastened into aluminum uprights?
What documentation should accompany an export batch of titanium bolts?
Can custom head shapes (drilled race heads, Torx flange) be produced in low volumes?
What is the lead time for standard stock vs. bespoke drawing-based orders?
Partner with Baoji's Premier Racing Fastener Factory
Direct manufacturer pricing, uncompromising aerospace-grade metallurgical purity, and flexible low MOQs. Download our complete 2025 racing catalog or speak directly with our engineering team for a rapid quote on custom drawing specifications.