Precision Performance Lineup
Explore production-ready Gr5 titanium fasteners, sprocket fastening solutions, and custom CNC automotive/motorcycle assemblies direct from our specialized manufacturing cells.
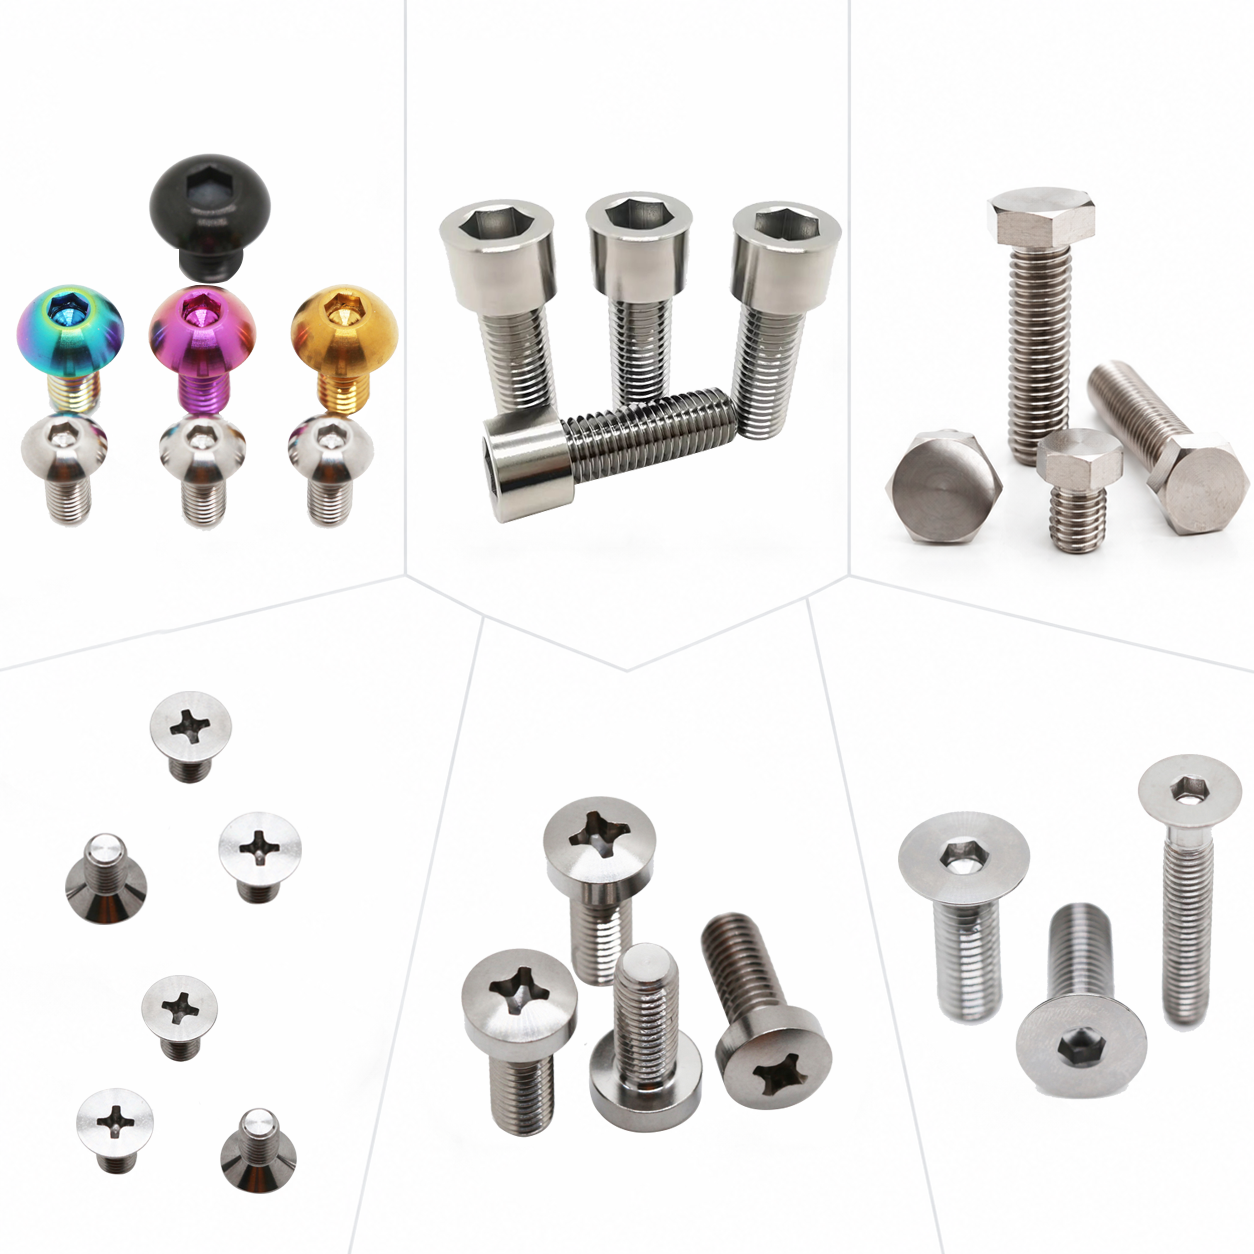
GR5 Titanium Alloy Standard Bolts Factory Wholesale Fastener Bolts and Nuts
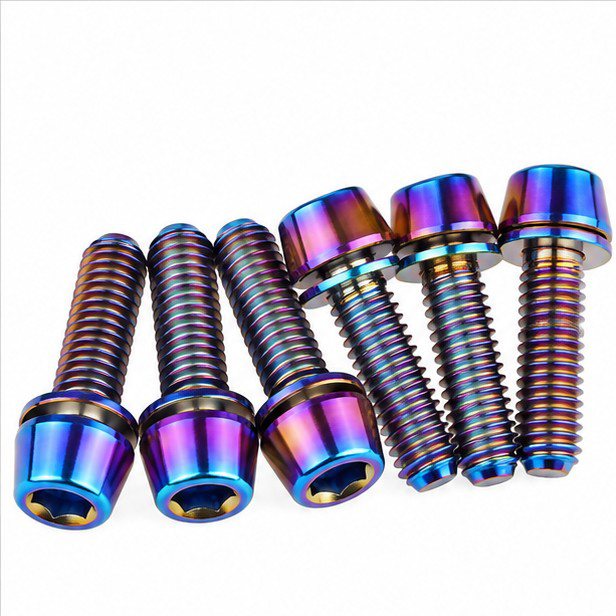
Titanium M5 Bolt with Washer Stem Screw (Burnt Blue, M5x16mm)
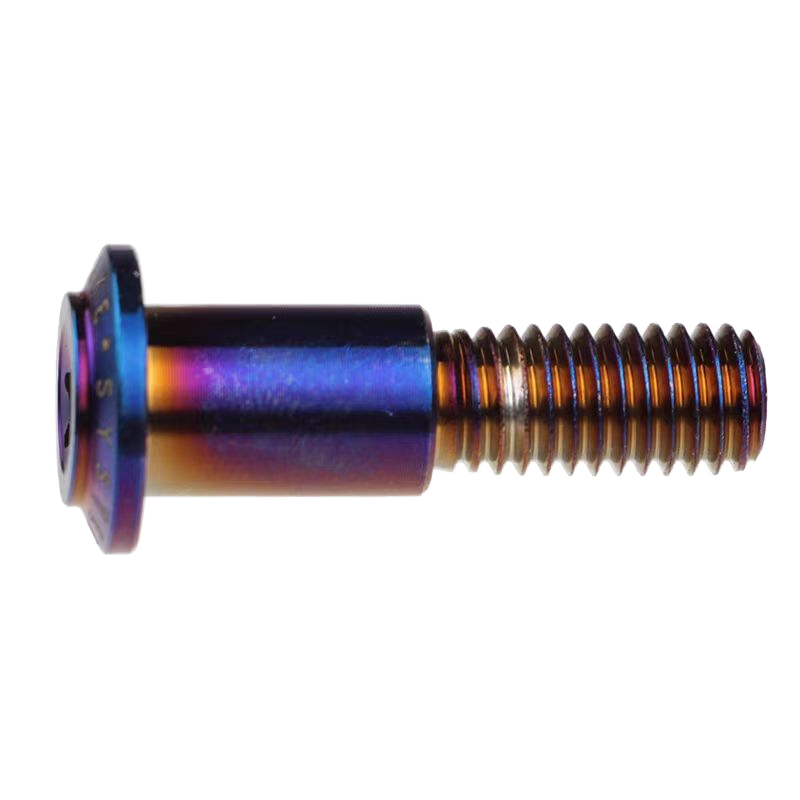
Bike Motorcycle Titanium Bolts Hexagonal Step Flat Head Teeth Disc Brake
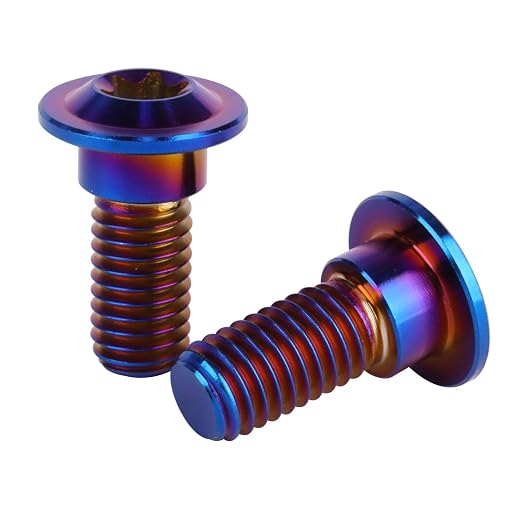
Motorcycle Titanium Bolts Hexagonal Step Flat Head M8 1.25 Teeth Disc Brake
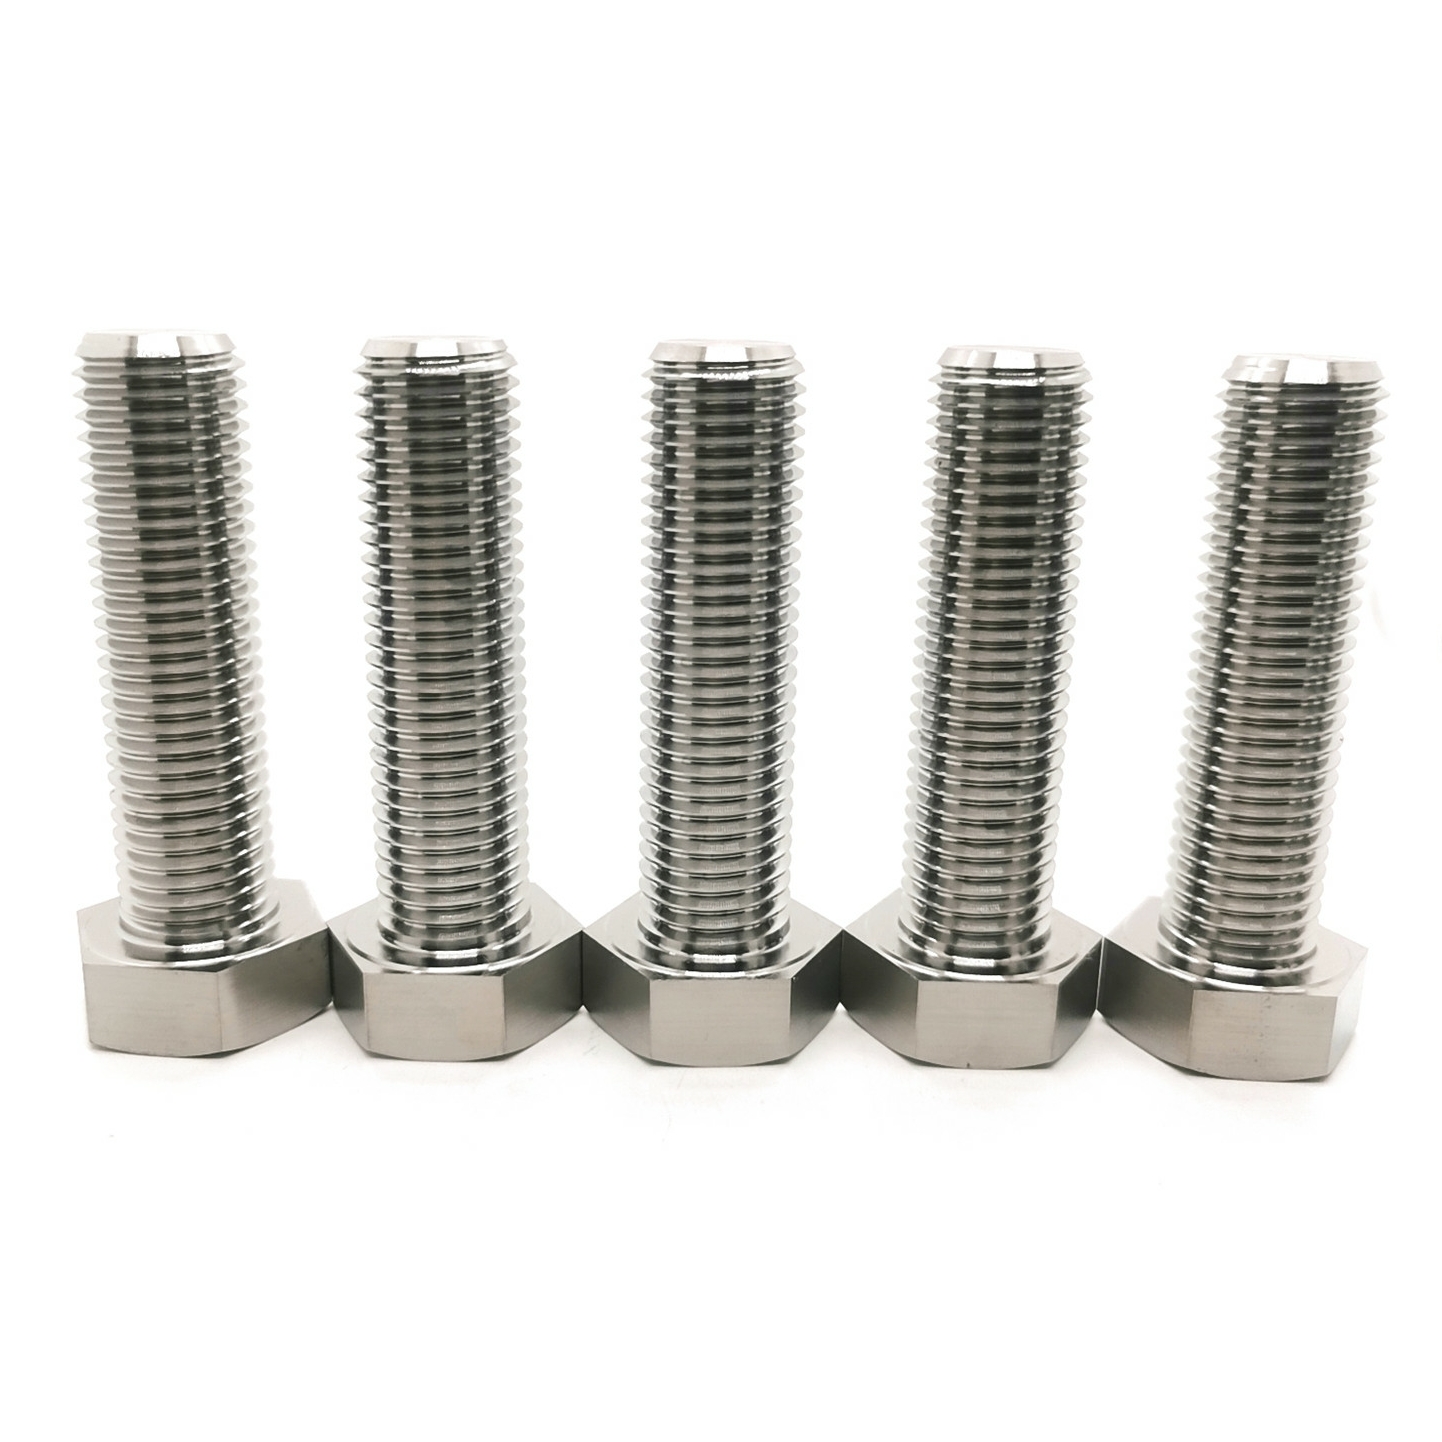
DIN912 Titanium Hexagon Socket Head Cap Screws Class 8.8 CNC Machined
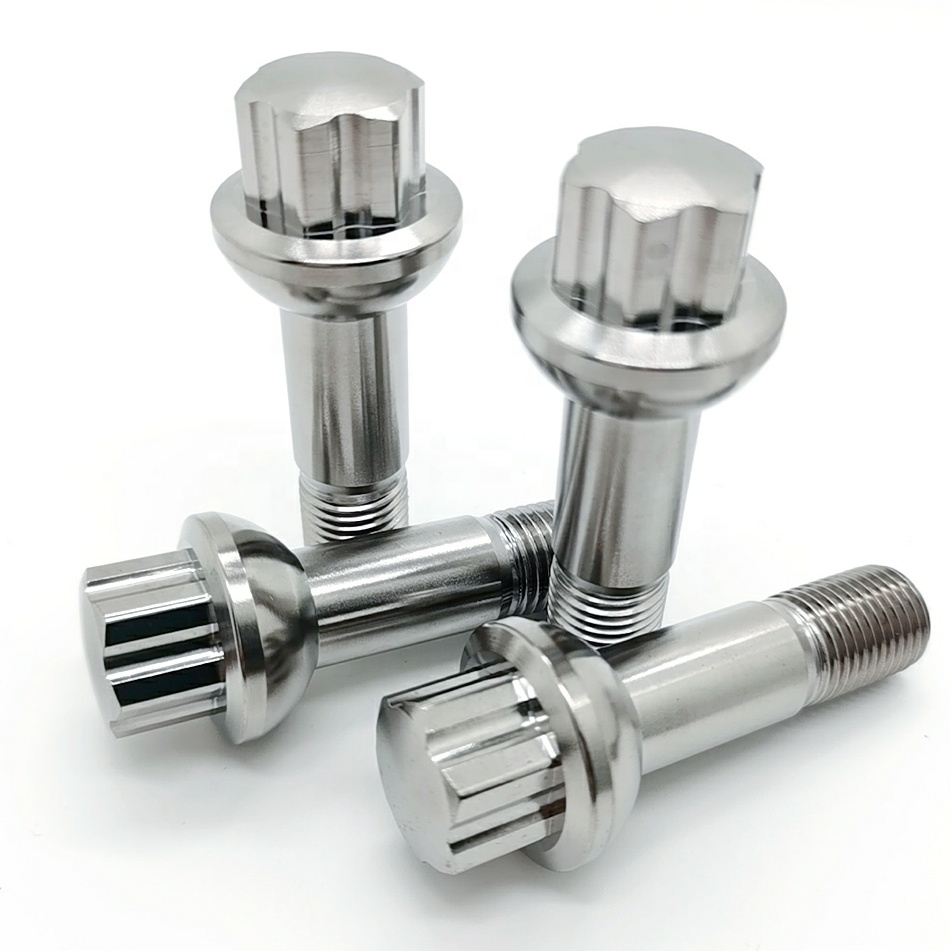
Nice Surface Titanium Lug Wheel Bolts M14x1.5 / M12x1.25 for Racing Cars
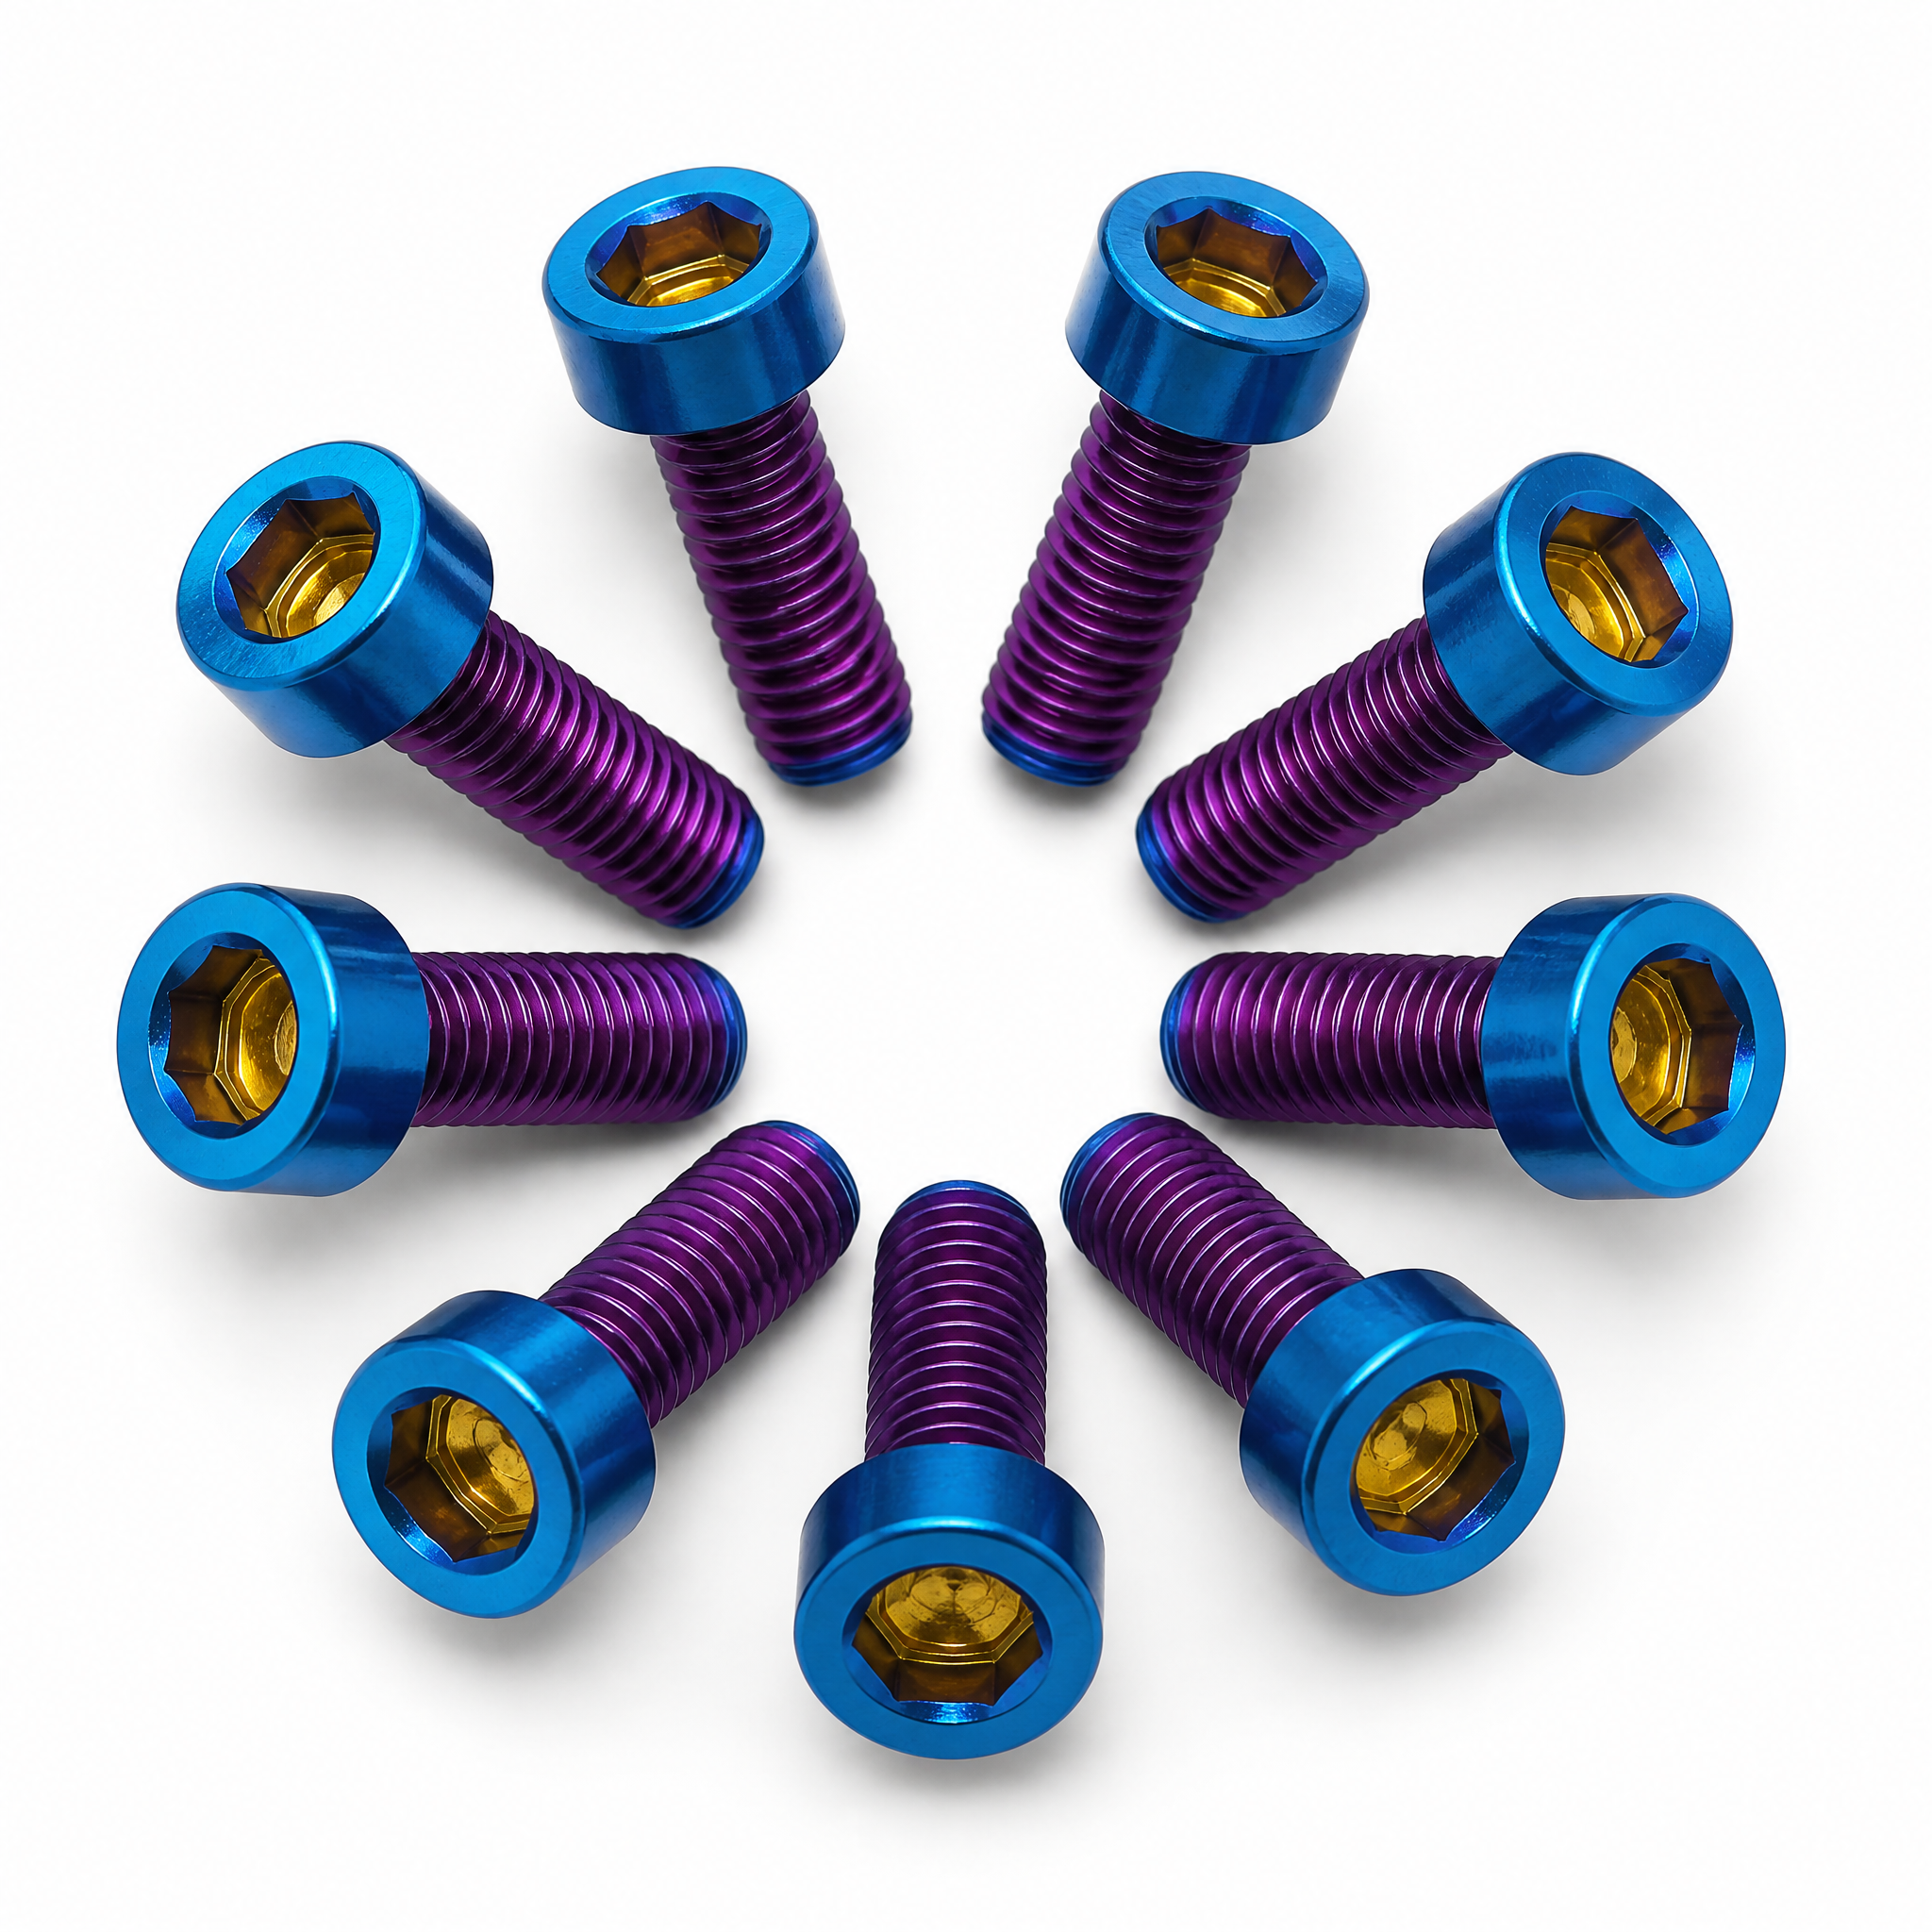
Titanium Alloy Bolts Gr5 Anodized Colored Torx Bolts M4 M5 M6*15 Modified Screws
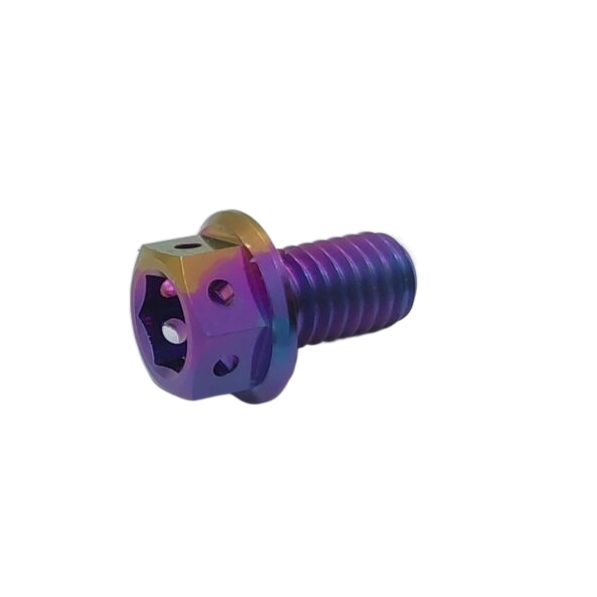
ZFTI Class 8.8 Gr5 Titanium Flange Bolt Anodized PVD Hex Head UNF Thread
Engineering Dynamics: Why Titanium Grade 5 Redefines Sprocket Fastener Longevity
In high-torque powertrain systems—such as motocross bikes, supermotos, rally vehicles, and track-engineered superbikes—the rear sprocket assembly operates under extreme shear stress, cyclical vibration, and severe shock loads. Traditional zinc-plated carbon steel bolts (Class 8.8 and 10.9) carry an inherent liability: significant unsprung rotational mass and sensitivity to stress-corrosion cracking (SCC). When racing setups run over rough courses or sustain aggressive downshifts, the instantaneous shear torque applied to the sprocket mounting holes can exceed standard yield calculations if pre-load tension relaxes.
As dedicated Custom OEM Titanium Sprocket Bolts Factories & Exporters, Yevzo manufactures rear wheel sprocket hardware leveraging cold-rolled threads over precision-turned Grade 5 Ti-6Al-4V (ASTM B348 / AMS 4928) bar stock. With an ultimate tensile strength surpassing 950 MPa and an exceptional strength-to-weight ratio, our titanium sprocket bolts cut unspring rotating inertia by approximately 44% compared to steel. Reducing rotational mass at the wheel hub translates directly into faster acceleration response, reduced rear-suspension hysteresis, and mitigated fatigue degradation on the wheel hub carrier bushings.
Material Metallurgy Comparative Evaluation
| Mechanical Property | Ti-6Al-4V (Gr5 Titanium) | AISI 4140 Alloy Steel (Q&T) | Grade 2 (Commercially Pure) | 7075-T6 Aluminium |
|---|---|---|---|---|
| Ultimate Tensile Strength (MPa) | 950 – 1050 | 900 – 1000 | 345 – 450 | 510 – 540 |
| Yield Strength (0.2% Offset, MPa) | 880 – 920 | 750 – 850 | 275 – 350 | 430 – 480 |
| Density (g/cm³) | 4.43 | 7.85 | 4.51 | 2.81 |
| Fatigue Limit Ratio (Cycles 10⁷) | 0.55 – 0.60 | 0.40 – 0.45 | 0.35 | 0.28 – 0.32 |
| Shear Modulus (GPa) | 43 – 45 | 80 | 40 | 27 |
| Corrosion Resistance (Chloride/Brine) | Impervious (Self-Passivating) | Requires Plating / Rusts | Superior | Prone to Pitting |
Noticeably, although 7075-T6 aluminium provides low weight, its shear fatigue strength under repetitive, sudden chain shock makes it unsafe for drive sprockets. Ti-6Al-4V strikes the optimal balance of aerospace-grade yield performance and lightweight agility, giving professional racing teams and OEM equipment distributors unquestioned mechanical safety margins.
Procurement & Drivetrain Sourcing Trends
How Tier-1 automotive brands, aftermarket racing enterprises, and boutique e-mobility developers are evolving their global titanium fastener procurement protocols.
TCO Optimization & Near-Net Manufacturing
Purchasing managers are shifting from evaluating upfront unit costs to calculating Total Cost of Ownership (TCO). High scrap rates from subtractive machining are being replaced with hot-forged blank preforms followed by high-speed CNC thread rolling. This process eliminates grain-boundary shear defects, doubles component service lifetimes, and curtails replacement cycles across harsh track conditions.
Electrification & High-Torque Drivetrains
High-output electric motorcycles and performance EVs generate instantaneous maximum torque from standstill (zero RPM). This instant impulse places catastrophic shear tension on sprocket and hub studs. Procurement leaders are mandating Gr5 Class 10.9-equivalent titanium specifications with rolled thread profiles to mitigate notch sensitivity and withstand peak torque cycles without plastic stretch.
Traceability & Environmental ESG Compliance
European and American defense, industrial, and racing sectors require full material traceability. Future supply agreements demand verified heat numbers, chemical composition spectroscopy (ICP-OES), and physical destruction pull-tests corresponding to raw material billets directly traceable to source sponge factories in Baoji, eliminating unregulated alloy dilution.
Engineering Advancements in Sprocket Bolt Technology
Emerging innovations reshaping performance parameters, thread durability, and metallurgical surface interfaces.
Rolled Threads vs. Cut Threads
Unlike conventional cut threads that sever metal grain lines, advanced titanium sprocket bolts employ hydraulic cold thread rolling. Continuous grain lines wrap smoothly around root radii, reducing stress concentrations, elevating root shear capacity by over 30%, and eliminating early micro-crack initiation during intense vibration.
Functional PVD & Anti-Galling Coatings
Galling (cold-welding) represents the historic operational bottleneck for titanium fastened into matching alloy or aluminium hub seats. Modern breakthroughs combine specialized Physical Vapor Deposition (PVD), Diamond-Like Carbon (DLC), or titanium anodizing with micro-ceramic thread films that ensure stable friction coefficients without reliance on messy wet pastes.
Integrated Fuji-Lock & Flanged Architectures
Advanced motorcycle racing setups prioritize integrated assemblies. Precision-machined self-locking all-metal lock nuts (Fuji-style with resilient spring washers) manufactured from Ti-6Al-4V replace separate plastic-insert nylon locknuts that perish under exhaust and brake-rotor thermal radiation.
Why Partner With Yevzo: Direct Baoji Titanium Manufacturing Directness
Operating out of the Honeycomb Industrial Park, Fenghuang 3rd Road in the Baoji High-Tech Development Zone, Yevzo Titanium Metal Co., Ltd. holds an indisputable strategic advantage. Baoji represents China's "Titanium Valley," producing the world's most concentrated volume of sponge titanium, certified alloy ingots, and ASTM B348 bars. Since our formation in 2013, our integrated manufacturing platform eliminates intermediary broker surcharges and delivers strict metallurgical accountability.
With an onsite manufacturing arsenal exceeding 100 advanced machining units—including multi-axis CNC lathe centers, precision cold-forging presses, thread rolling stations, automated polishing lines, and PVD chamber equipment—we engineer custom sprocket hardware directly matching CAD drawings (.STEP, .IGES, .DWG, PDF). Our team reviews dimensional tolerances (up to ±0.005mm), thread fit classifications (6g/6H, Class 2A/2B), surface roughness requirements (Ra < 0.4μm), and anti-corrosive coating applications before batch cycling.
Sprocket Bolts Procurement FAQ
Practical technical and commercial guidance for purchasing managers, engineering designers, and international supply chain directors.
Why choose Gr5 (Ti-6Al-4V) over Gr2 for drive sprocket applications?
Grade 2 commercially pure titanium possesses a minimum tensile strength of roughly 345 MPa, which is inadequate for the high shear forces in drivetrains. Grade 5 is an alpha-beta alloy yielding over 895–950 MPa tensile strength, exceeding Class 8.8 steel parameters while offering resilience against cyclic fatigue and chain shock loads.
How should titanium sprocket bolts be installed to prevent galling?
Titanium threads naturally generate a thin passivating oxide film that can tear and micro-weld under bare dry torque. Always apply a high-nickel, copper-based, or synthetic anti-seize paste before fastening. Alternatively, specify our PVD/DLC-coated bolts, which decrease the friction coefficient and allow direct torquing to OEM specs without galling.
Does custom PVD coloring or anodizing affect thread tolerances?
Electrochemical titanium anodizing grows an optical refraction oxide film mere nanometers thick, causing no measurable dimensional shift. Functional PVD (TiN, TiCN, or DLC) adds a uniform layer of roughly 1.5–3.0 microns, safely managed within standard ISO 6g external thread tolerances without binding.
What are the typical MOQs and lead times for custom drawings?
Stock standard titanium hex and flange bolts start from 20 to 100 units. For fully bespoke OEM sprocket fasteners machined to client drawings (.STEP/.DWG), prototype production starts at 50–100 pieces with sample lead times of 10–14 days. Volume production orders generally ship within 20–30 days via DHL, FedEx, or air/ocean freight.